- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling




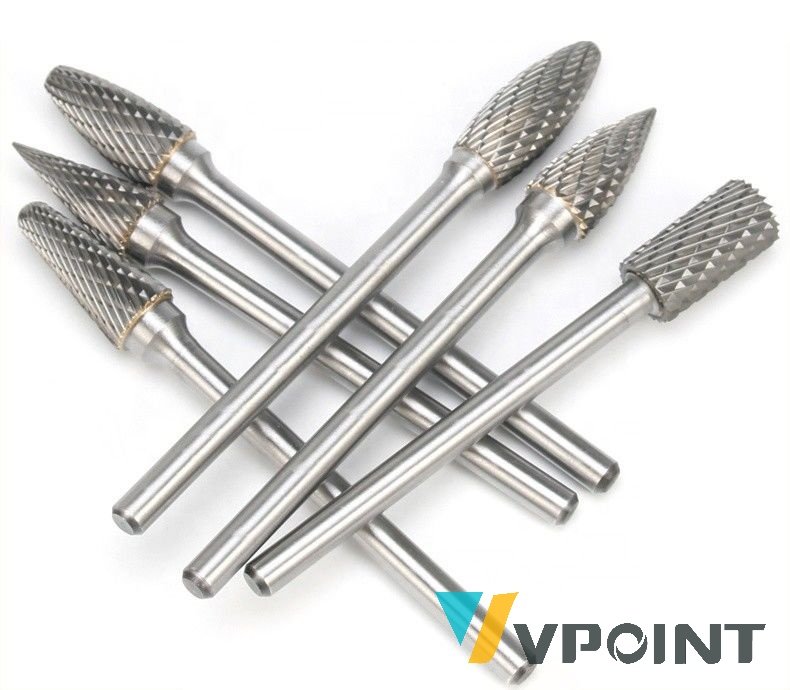

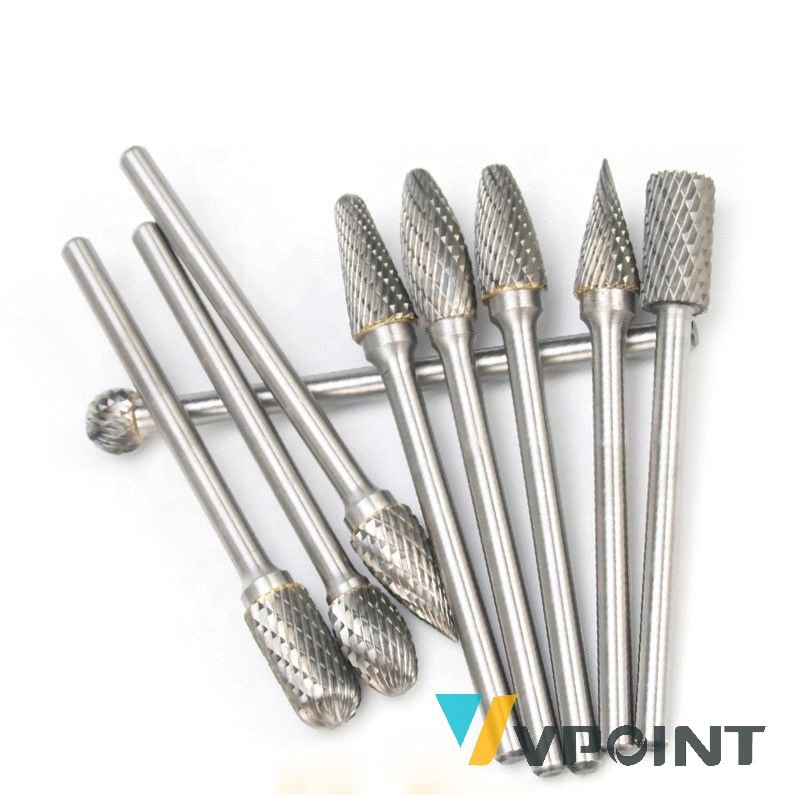


Design and Construction
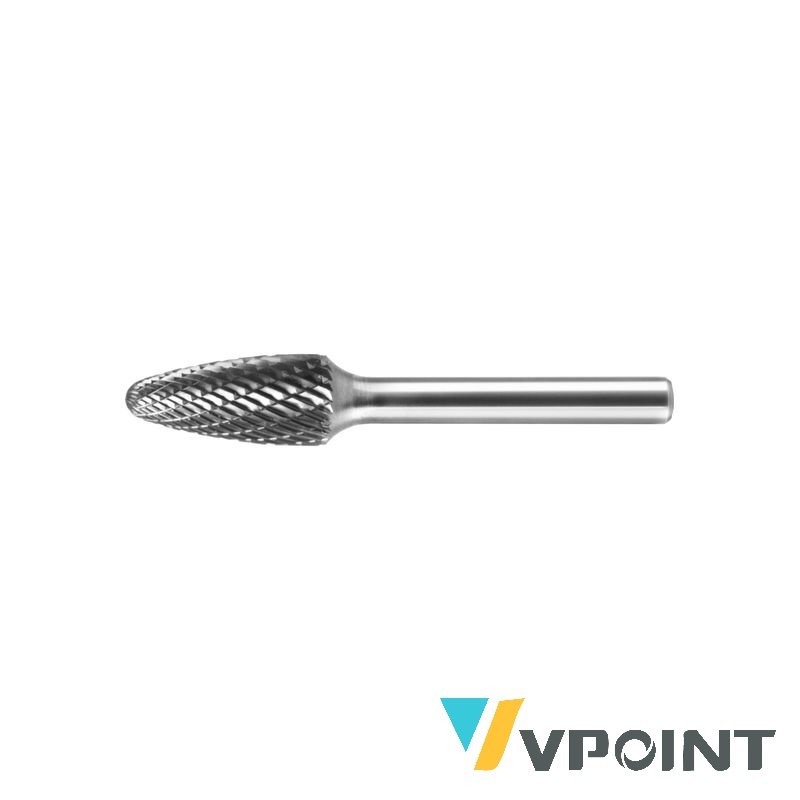
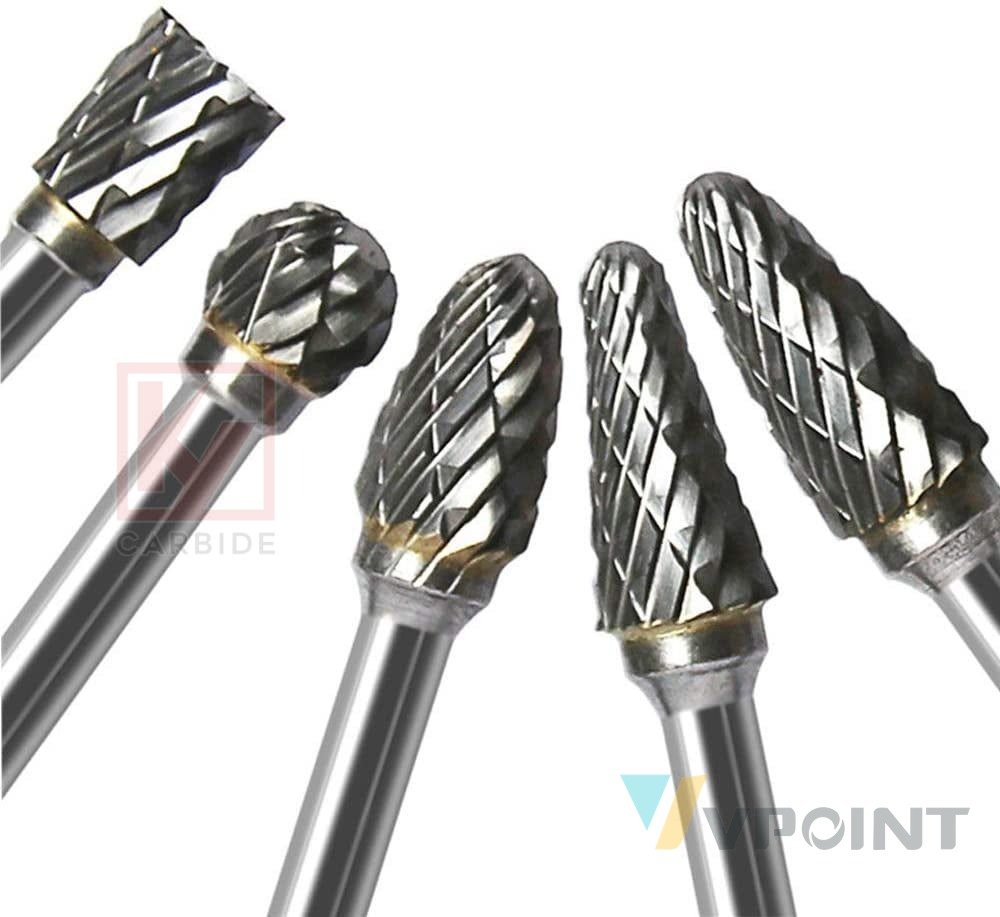
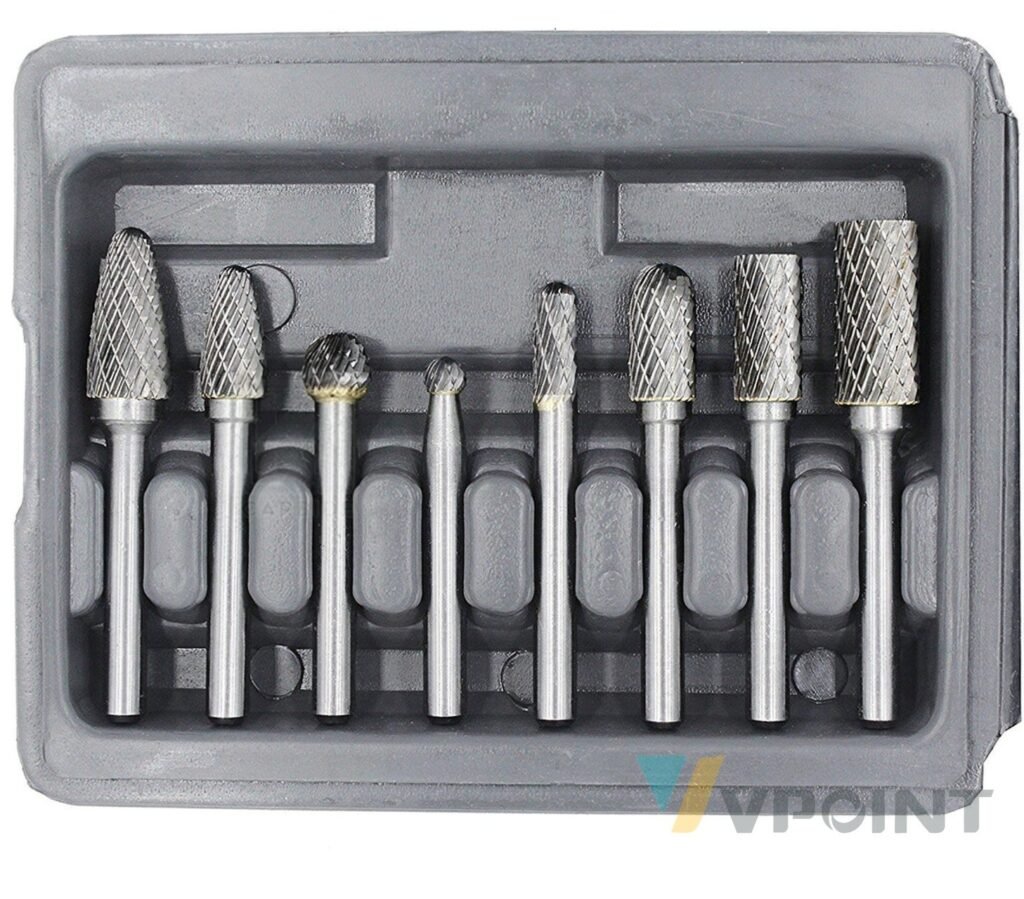
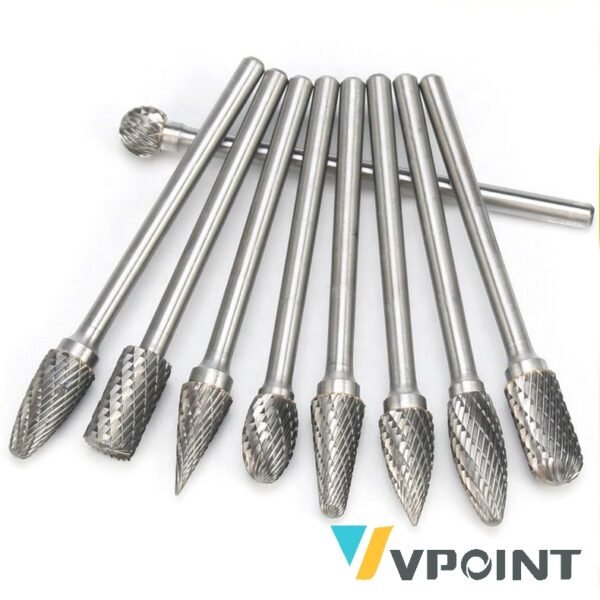
A safety-oriented extended-length carbide burr for interrupted cuts, cross holes and uneven cast surfaces. Head geometry, braze quality and shank straightness are held to a consistent standard because intermittent engagement puts a shock load through the whole assembly.
How It Works
An interrupted cut loads and unloads the tool every revolution. On a long shank that cycle excites vibration, so the practical controls are a reduced side load, a secure collet grip and a tool with no braze or straightness defects.
Applications
Cross-hole deburring, cast skin removal, interrupted weld seams, uneven surfaces, maintenance work in frames.
Field Cases
- Foundry: cross-hole burrs cleaned at reduced feed with no head losses.
- Fabrication: uneven cast skins dressed without the grabbing seen at full feed.
- Maintenance: frame welds with gaps and steps finished with a controlled light cut.
Performance Data
| Metric | Value / Observation |
|---|---|
| Primary duty | Interrupted / intermittent cuts |
| Load pattern | Cyclic shock loading |
| Controls | Light side load, secure collet, sound joint |
| Construction | Carbide head on straight extended shank |
Suitable Materials
Cast iron, cast steel, carbon and alloy steel, stainless steel and weld metal.
Material Comparison: Continuous vs Interrupted vs Cross-Hole Engagement
How engagement pattern changes the load on an extended tool. Typical industry analysis:
| Factor | Continuous Cut | Interrupted Cut | Cross-Hole Edge |
|---|---|---|---|
| Load per revolution | Steady | Cyclic spikes | Sharp spikes at each hole edge |
| Vibration excitation | Low | High | Highest |
| Recommended side load | Nominal | Reduced | Minimal |
| Collet grip requirement | Standard | Secure | Very secure |
| Defect sensitivity | Moderate | High | Highest |
| Typical feature | Flat surface | Weld seam, cast skin | Cross-drilled hole |
Delivery Scope
Single burr; reach, head shape and shank diameter confirmed with the order.
Why Choose VPOINT
Interrupted cuts are a safety problem on a long tool – the controls are stated instead of left to habit.
Precision & Quality Control
Braze integrity, shank straightness and head runout inspected per lot with ISO 9001 batch traceability.
Specifications
Published specification:
| Item | Specification |
|---|---|
| Type | Safety extended length burr |
| Duty | Interrupted / intermittent cutting |
| Construction | Carbide head on straight shank |
| Controls | Light side load, secure collet |
| Workpiece | Cast iron, cast steel, steel, weld metal |
| Inspection | Per-lot braze and straightness |
Frequently Asked Questions
Why are interrupted cuts harder on a long tool?
The cyclic load excites vibration along the extended shank.
What should I change in the setup?
Reduce side load, secure the collet grip and use a tool with a sound braze joint.
Is it suitable for cross holes?
Yes – that is a primary application, at minimal side load.
Which materials?
Cast iron, cast steel, carbon and alloy steel, stainless and weld metal.
What is inspected?
Braze integrity, shank straightness and head runout per lot.
Related Search Terms
safety extended length burr, interrupted cut carbide burr, cross hole deburring tool, cast skin removal burr, shock load rotary burr, long shank vibration control, secure collet burr, uneven surface die grinder, weld seam extended burr, braze integrity long burr, cyclic loading carbide, maintenance frame burr, light side load burr, long reach safety tool, intermittent cutting burr