- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
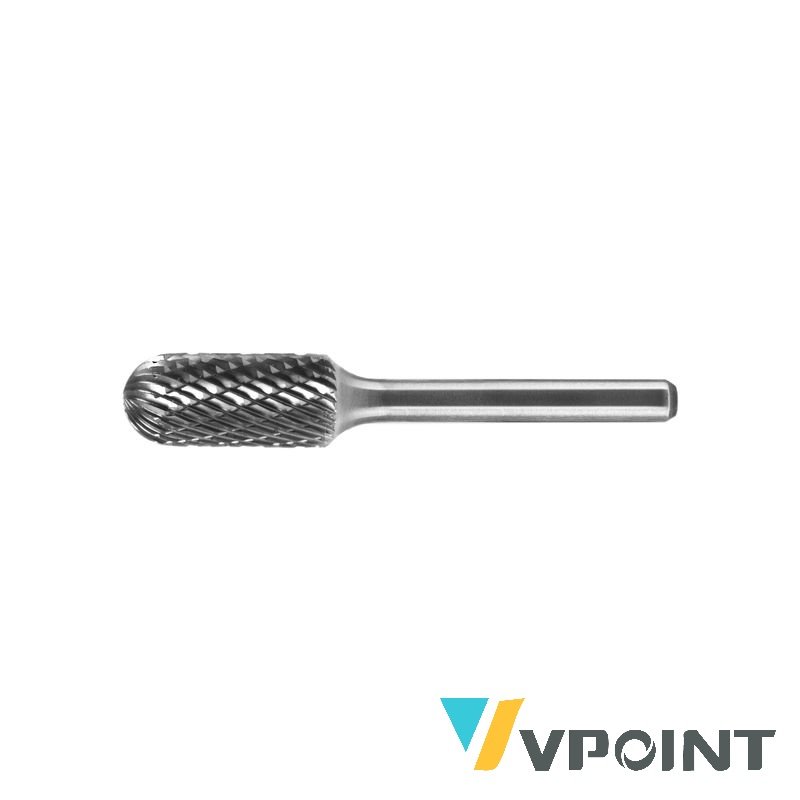
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling


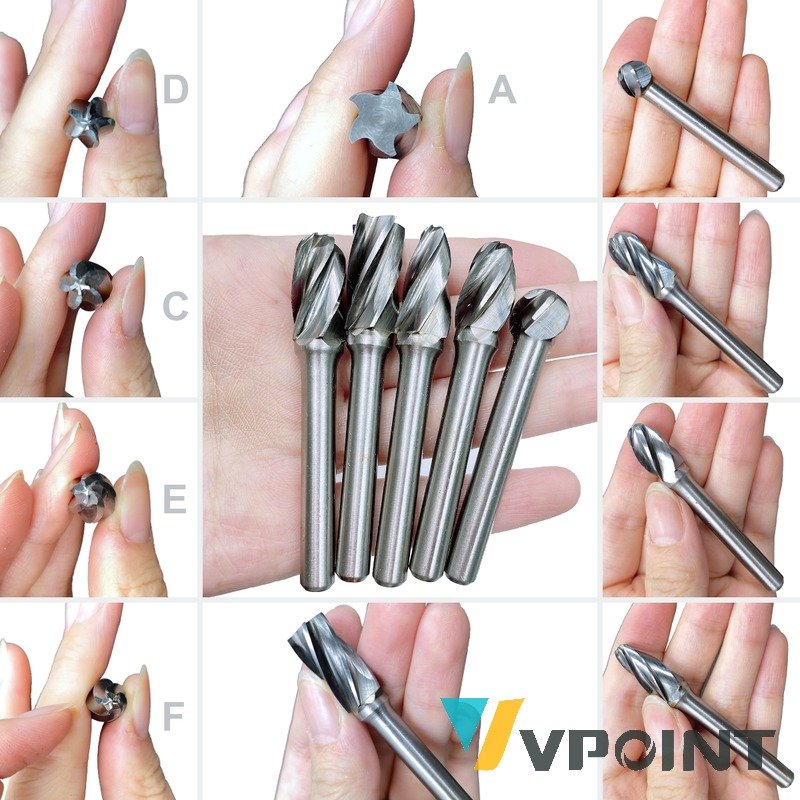

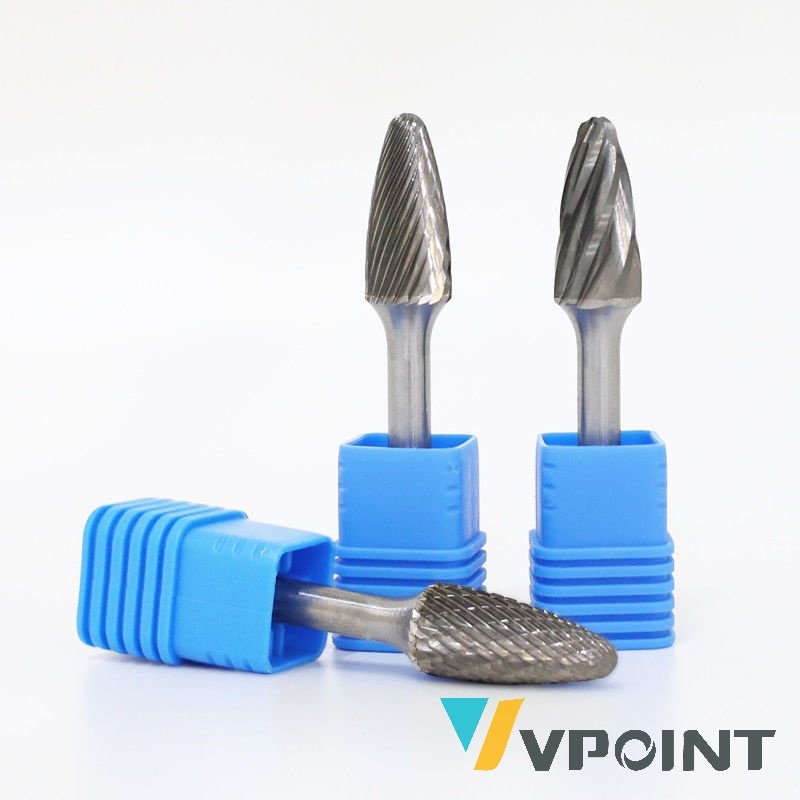
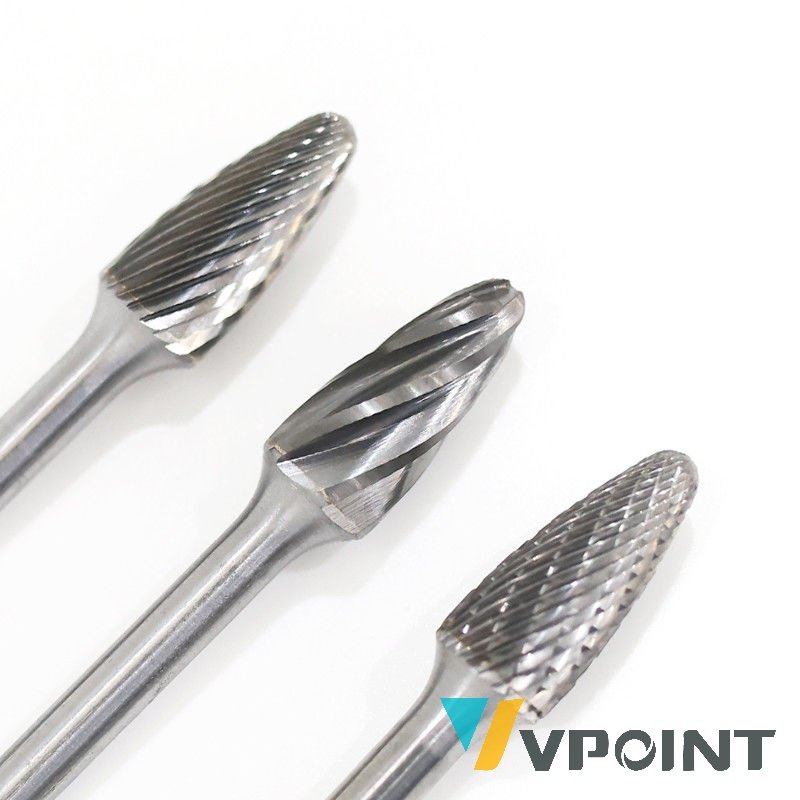

Design and Construction
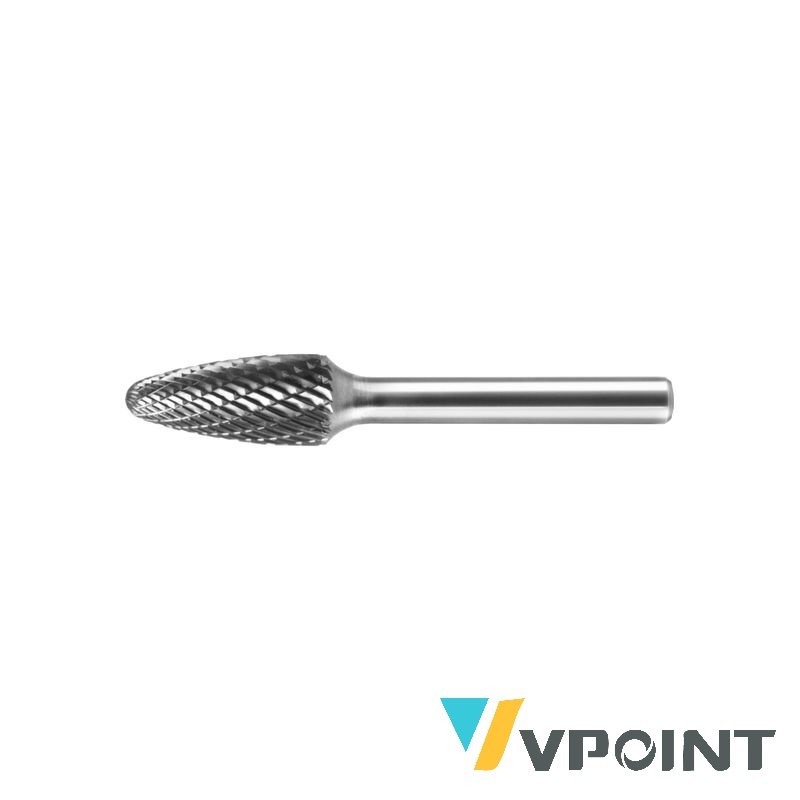
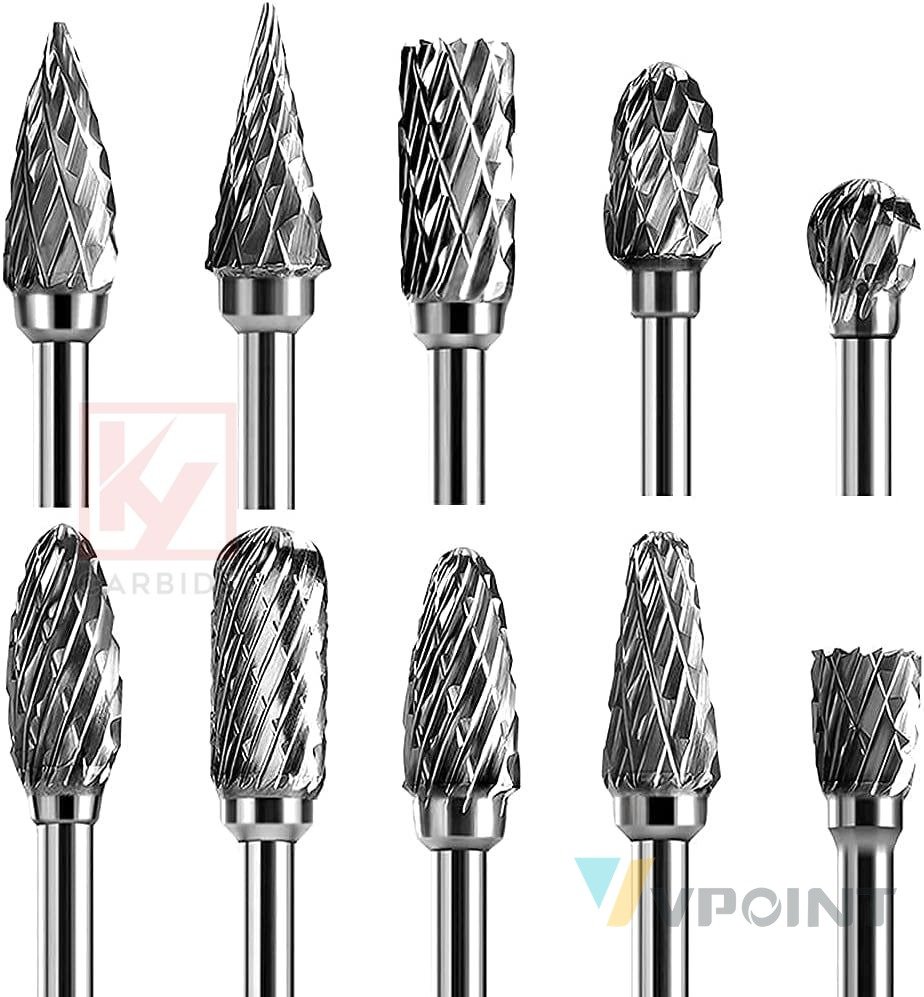
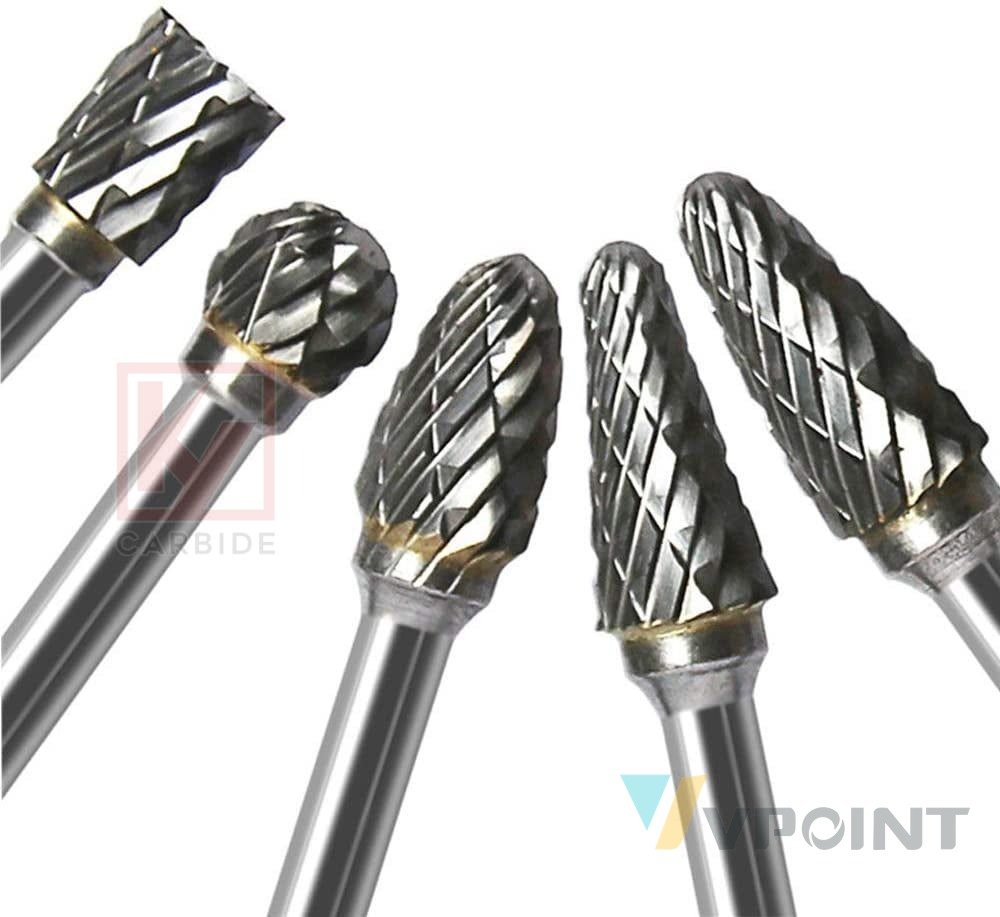
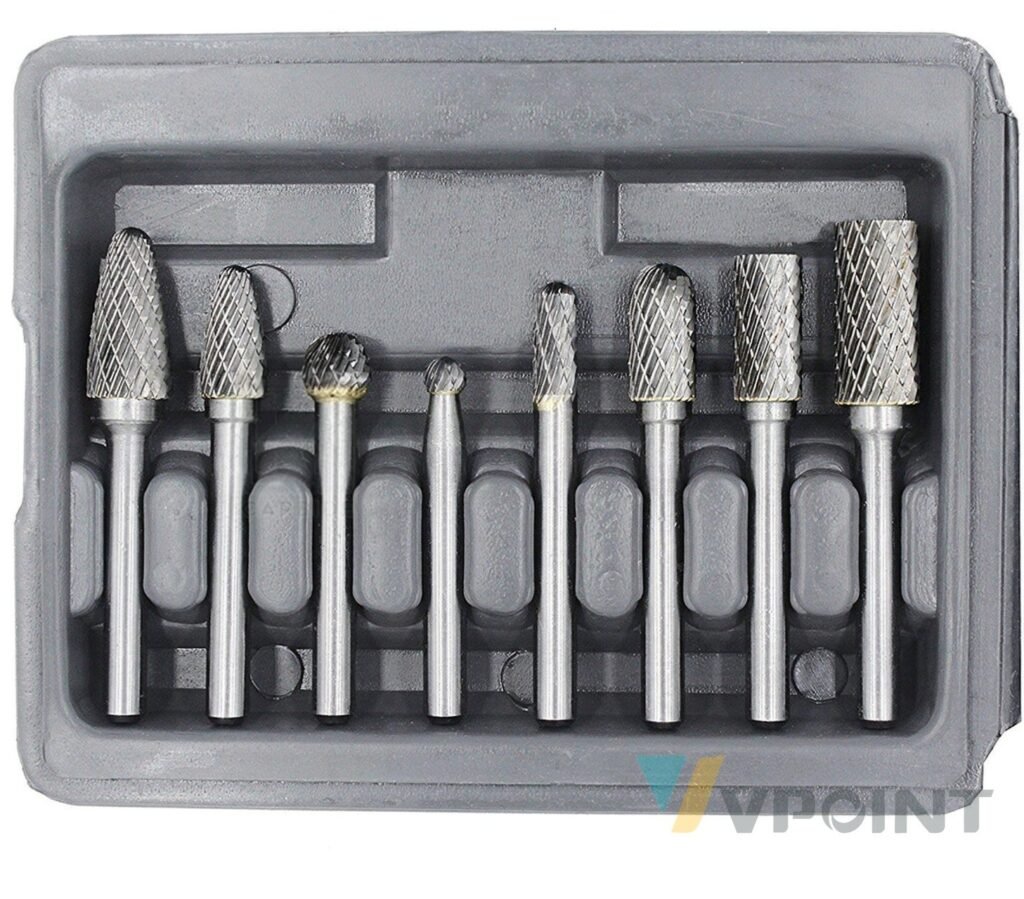
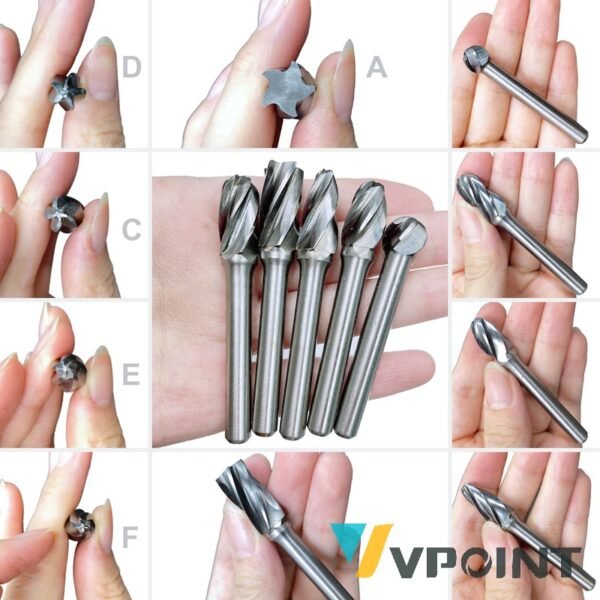
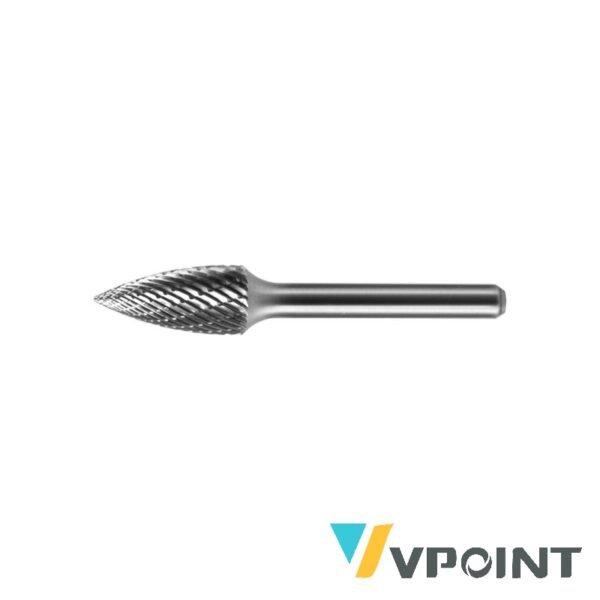
This set combines tree-shape-with-end-cut carbide burrs on 6 mm (1/4″) shanks. Heads are offered as solid carbide (3 mm head) or silver-brazed carbide heads (4-6 mm) on steel shanks. The coarse “aluminum tooth” (Aluma cut) flute opens the chip gullets so soft, gummy material such as aluminum and plastics clears instead of loading the flutes.
How It Works
Mounted in a die grinder or rotary tool, the burr is run at 6,000-50,000 RPM. The coarse single-row flutes shear soft material in large chips; the end cut allows plunge and finish work in corners and along edges.
Applications
Aluminum profiling, non-ferrous weld dressing, plastics and FRP trimming, pipe and tube deburring, porting and general die-grinder work.
Suitable Materials
Aluminum and other soft non-ferrous metals, plastics, FRP, rubber, wood. For hardened steel use a double-cut burr instead.
Field Cases
- Truck-bed repair shop: strips a 2 mm weld bead along 6061 sheet with the Aluma head in one pass – a double-cut burr on the same joint loaded twice and needed pick cleaning.
- Radiator shop: opens collapsed tube ends in copper-brass cores; the open gullets keep soft solder chips from packing.
- Pattern shop: roughs PVC and Renshape model blocks where fine flutes clog within seconds.
Performance Data
| Metric | Value / Observation |
|---|---|
| Flute efficiency gain | Optimised tooth geometry improves cutting efficiency by roughly 30-50% vs a mismatched cut (industry grinding data) |
| Starting speed, 6 mm in aluminium | About 40,000 RPM – high speed helps flick chips out of the gullets |
| Lubrication tip | A film of beeswax or cutting wax prevents aluminium welding to the flutes |
| Head hardness | 1,300-1,500 HV carbide vs 240-300 HV HSS |
Material Comparison: Cut Style Showdown for Aluminium Work
How the aluminium-tooth (Aluma) cut earns its keep against the two common alternatives – typical industry data:
| Factor | Aluma Cut (this set) | Standard Double Cut | HSS Burr |
|---|---|---|---|
| Flute pattern | Coarse open gullets (Aluma cut) | Crossed flutes (double cut) | Conventional flutes |
| Chip behaviour in aluminium | Large chips clear before they weld | Fine chips tend to pack the gullets | Chips smear and load fastest |
| Usable speed (6 mm head) | 15,000-25,000 RPM | 20,000-40,000 RPM | 20,000-40,000 RPM |
| Loading risk on 6061 aluminium | Low – designed for non-ferrous | High without lubricant | Highest |
| Finish left behind | Slightly rough, fast | Smooth | Smooth but only until it loads |
| Best role | Aluminium and soft non-ferrous removal | Steel, stainless, cast iron | Light finishing only |
Delivery Scope
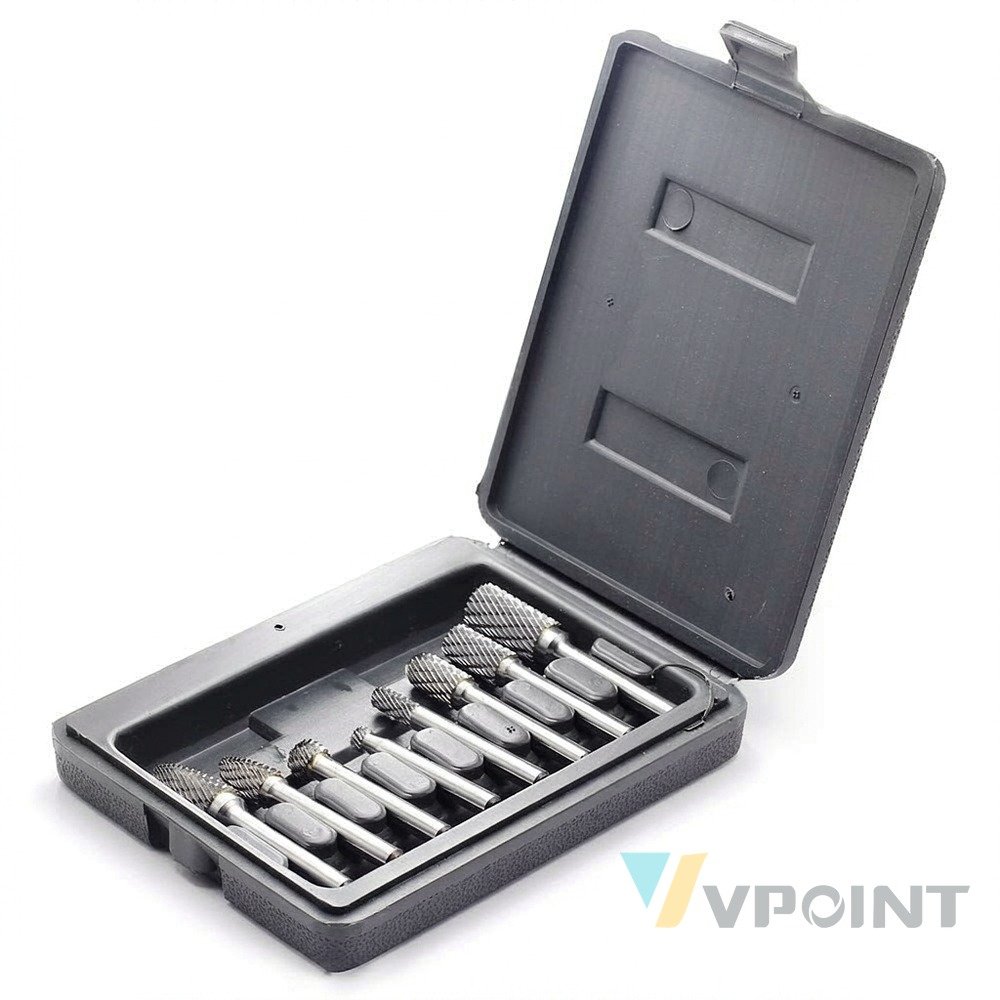
Set of burrs supplied in a plastic case. Custom head shapes, shank lengths and laser marking available on request.
Why Choose VPOINT
VPOINT TOOLS has manufactured precision cutting tools since 2008 in two production bases (Sichuan and Dongguan, China) under ISO 9001 quality management. Every carbide burr is supported by a one-year warranty, custom and non-standard engraving service, and regrinding service. Aluminum-cut flute geometry is ground in-house and can be tailored to your workpiece.
Precision & Quality Control
Each burr is checked for flute geometry, cutting-edge sharpness, shank runout and concentricity at micrometre level before packing; production batches are traceable and packed per ISO 9001 procedures.
Specifications
G shape (tree with end cut), coarse aluminum-tooth cut, 6 mm shank:
| Tool No. | Cut dia. (d1) | Cut length (l2) | Shank (d2) | Over length (l1) | Head |
|---|---|---|---|---|---|
| SG30314 | 3 mm | 14 mm | 3 mm | 38 mm | Solid carbide |
| SG30413 | 4 mm | 13 mm | 3 mm | 51 mm | Brazed head |
| SG30513 | 5 mm | 13 mm | 3 mm | 51 mm | Brazed head |
| SG30613 | 6 mm | 13 mm | 3 mm | 51 mm | Brazed head |
Frequently Asked Questions
Is the burr made of solid tungsten carbide?
Yes. The cutting head is solid tungsten carbide for the 3 mm head, or a silver-brazed tungsten carbide head on a steel shank for the 4-6 mm sizes.
Which shank sizes are available?
All burrs in this set use a 6 mm (1/4″) cylindrical shank for standard die grinders and collets.
What speed should I run the burr at?
Run between 6,000 and 50,000 RPM depending on the cutter diameter; use the lower end for larger diameters and the higher end for fine detail work.
Which materials can I machine with it?
Designed for aluminum and soft non-ferrous metals; also suitable for plastics, FRP and wood. Use double-cut burrs for hardened steel.
Do you accept custom or non-standard sizes?
Yes. VPOINT supports custom shapes, sizes, shank lengths and laser marking on non-standard orders (minimum order quantity applies).
Related Search Terms
aluminum cut carbide burr set, aluma cut rotary burr, 1/4 shank burr set for aluminium, SG series tree burr, die grinder burrs for aluminum, aluminium deburring tool, weld dressing rotary burr, fabrication deburring tool, steel shaping burr, metal carving bits, maintenance rotary files, grinder attachment burrs, cnc deburring tool, machine shop burrs, industrial carbide burrs, tool steel grinding