- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
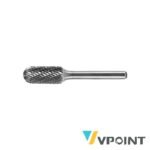
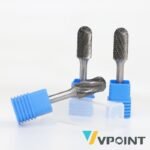
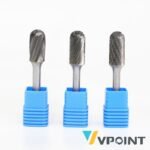
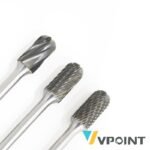



Design and Construction
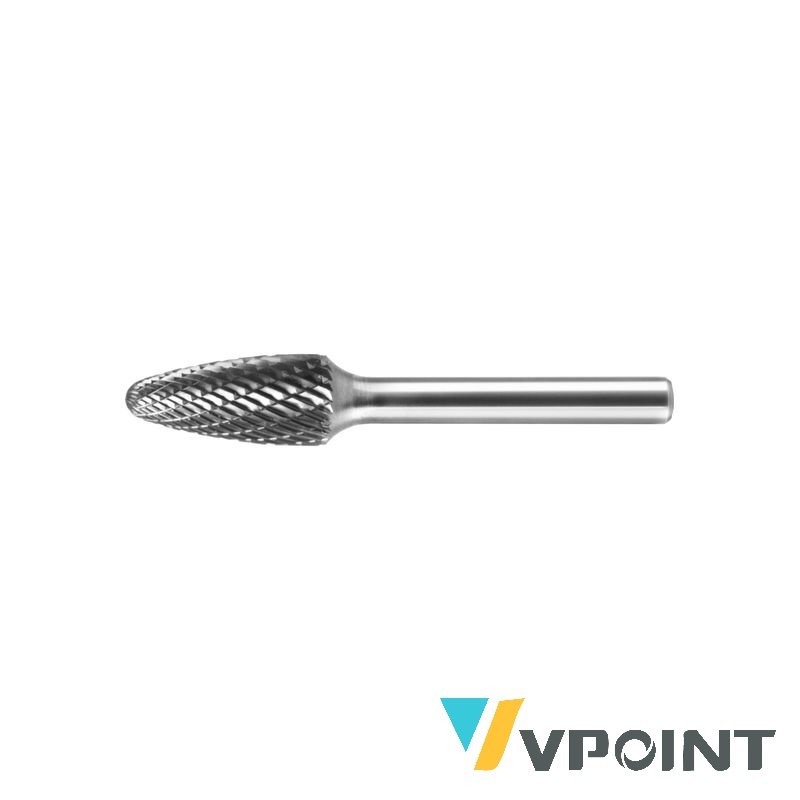
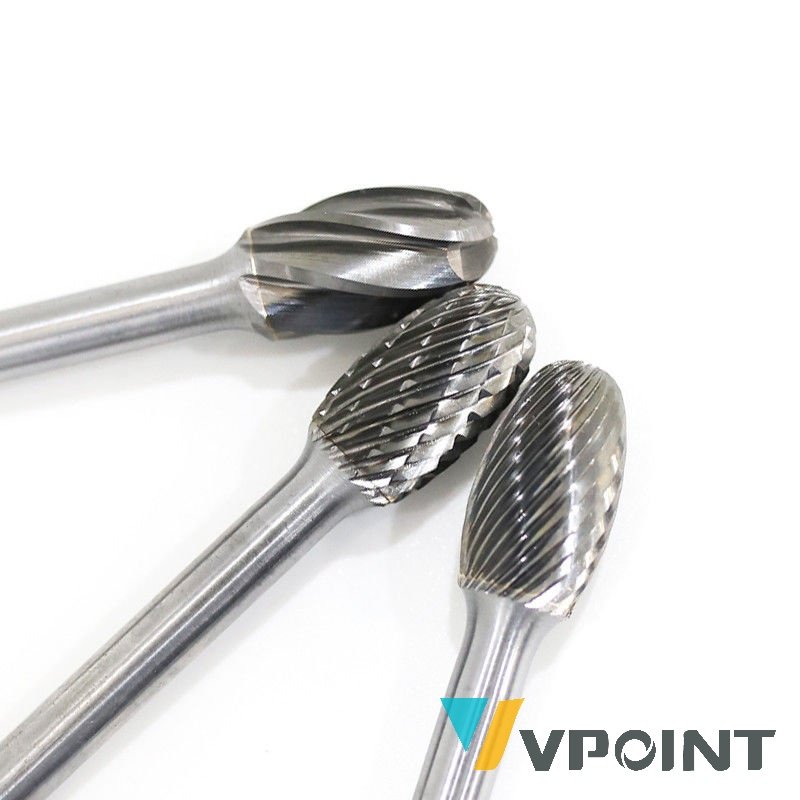
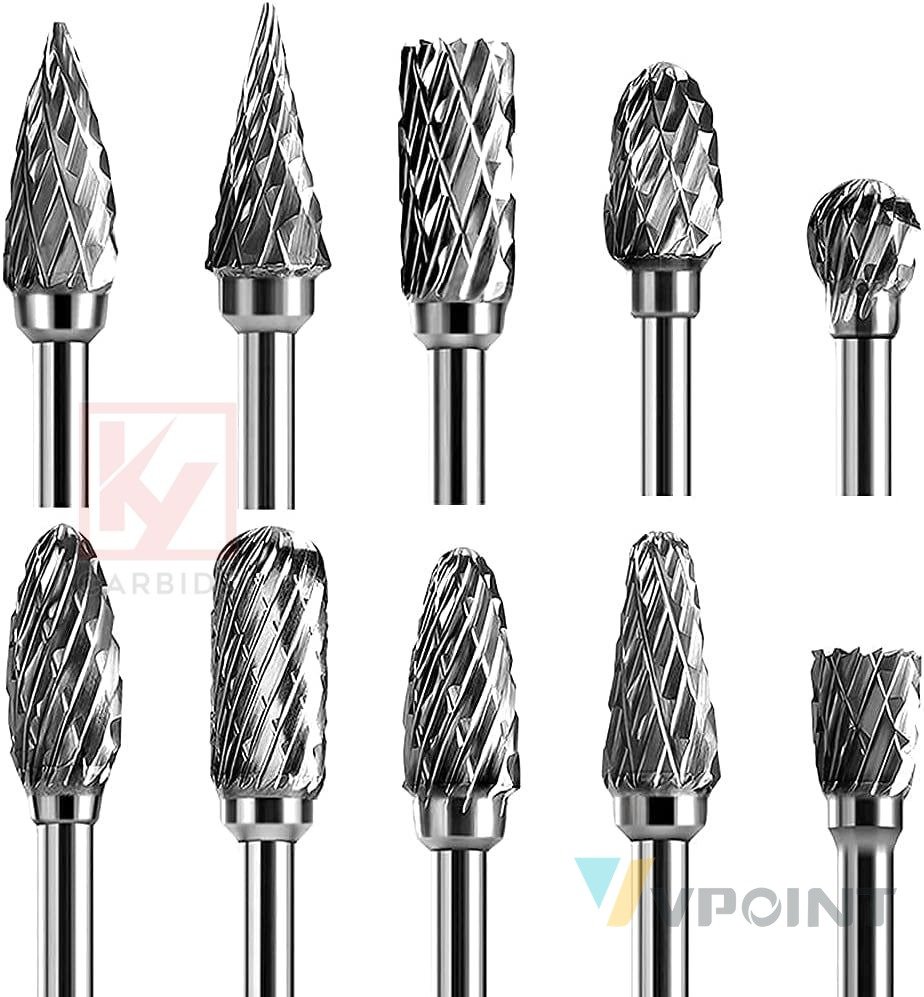
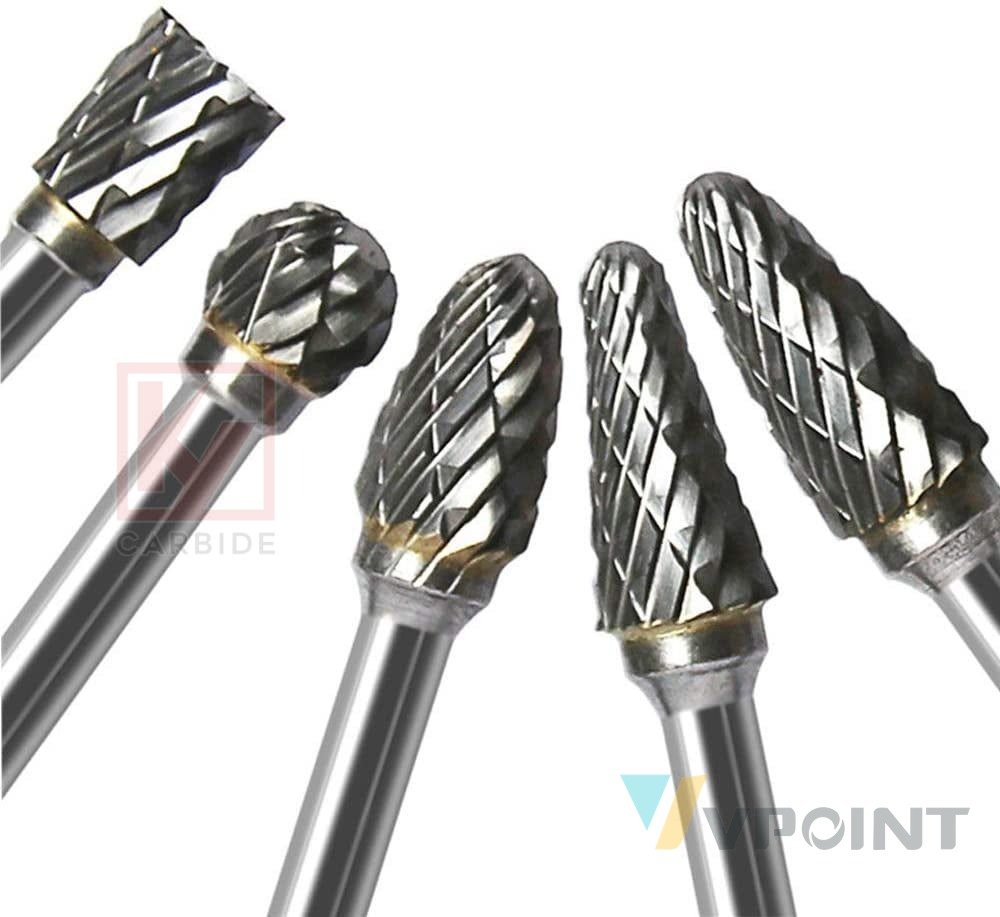
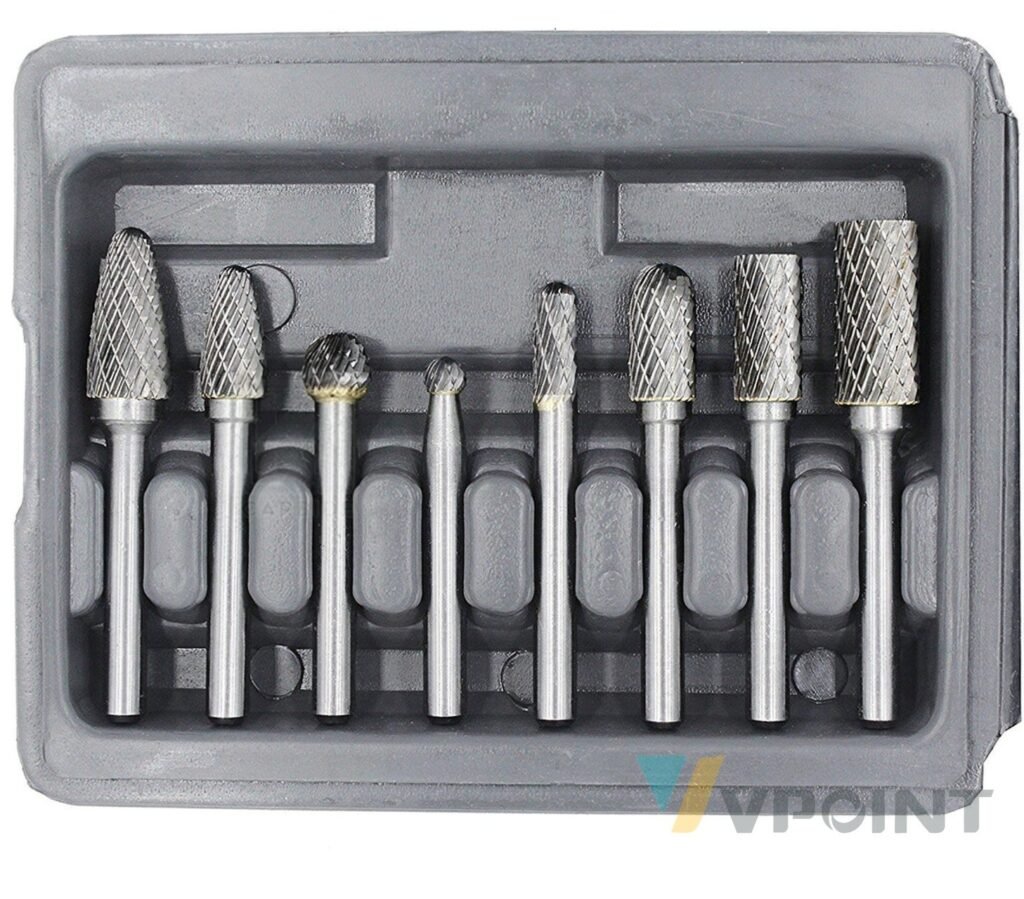
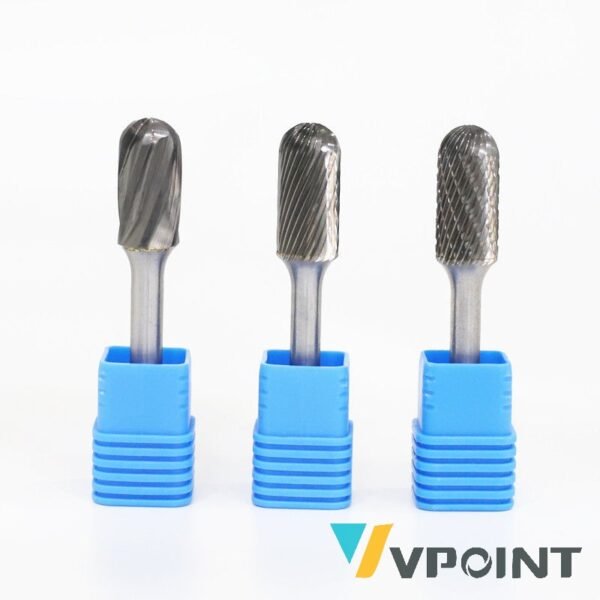
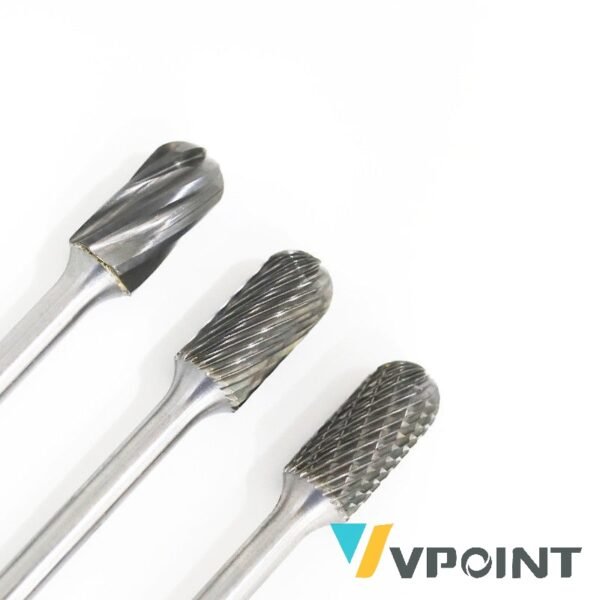
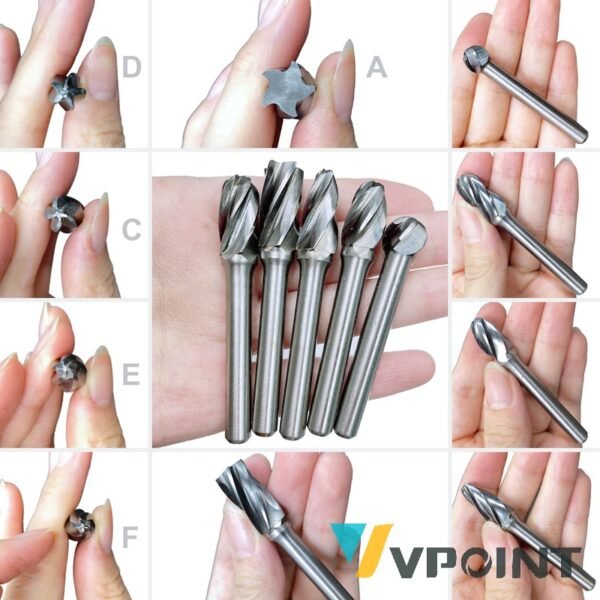
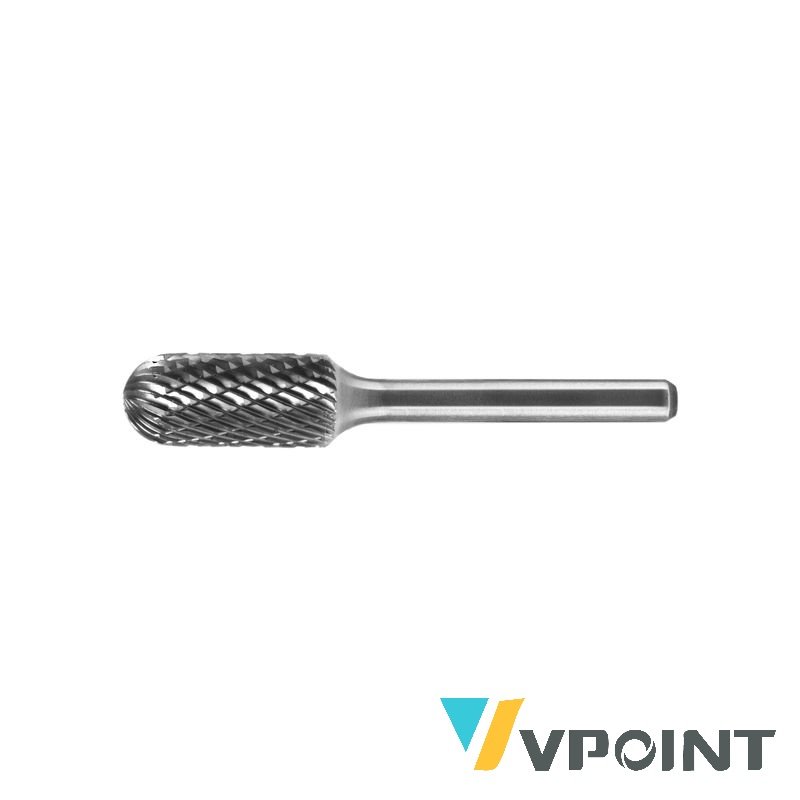
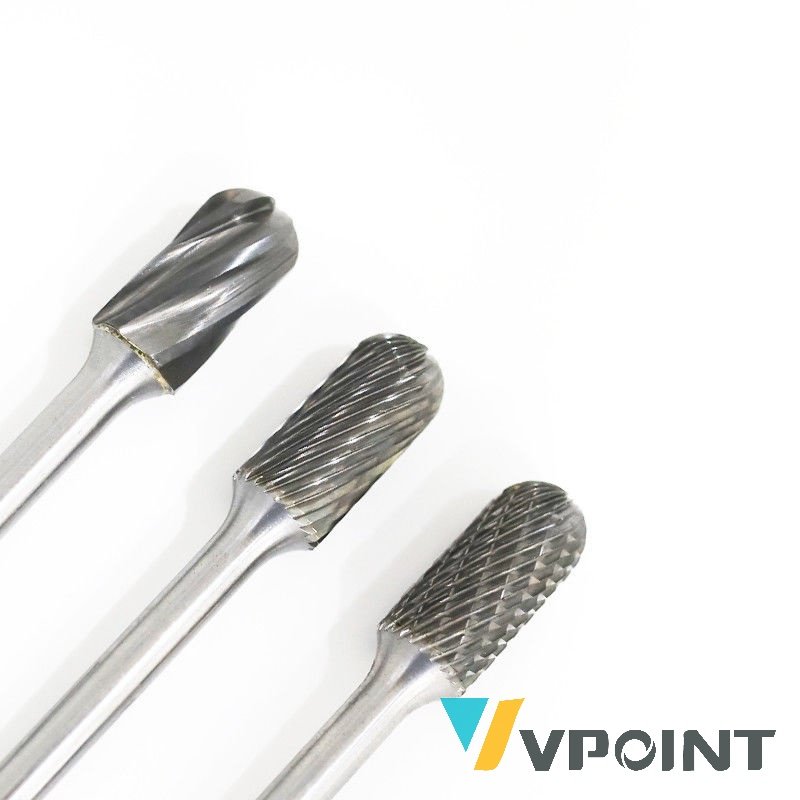
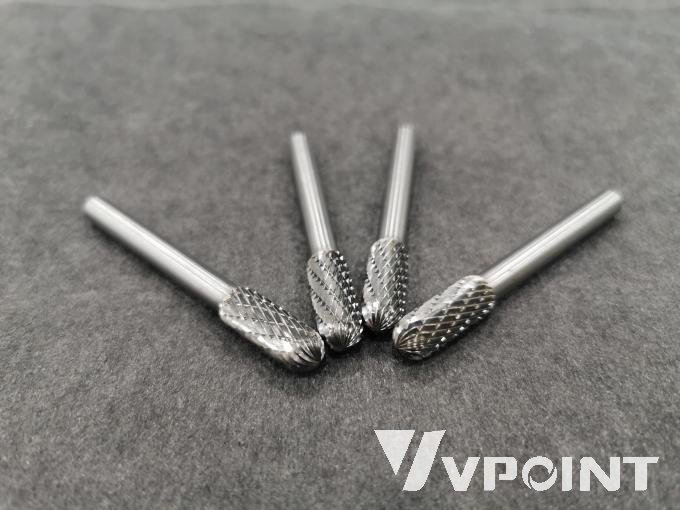
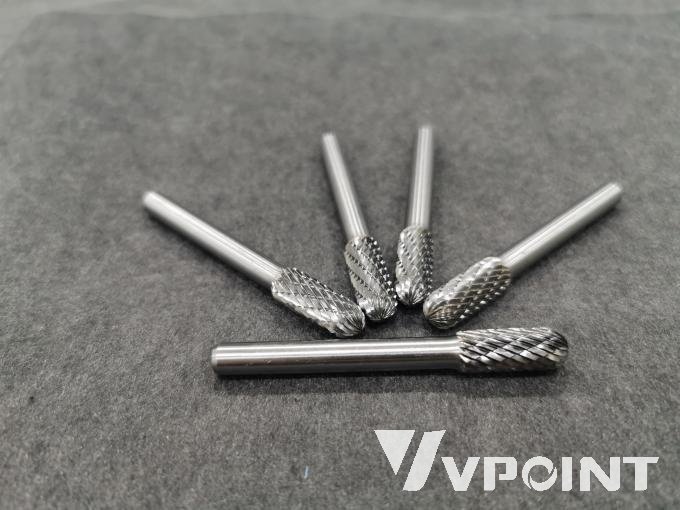
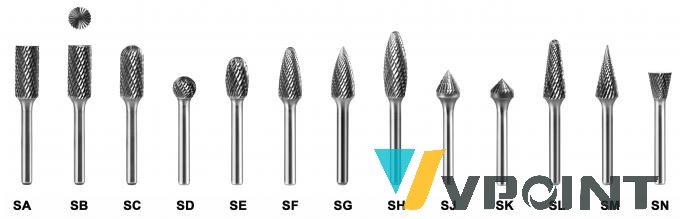
SA-SN series burrs are ground from integral tungsten carbide in thirteen head geometries: SA cylindrical, SB cylindrical with end cut, SC cylindrical ball nose, SD ball, SE oval, SF tree, SG pointed tree, SH flame, SJ 60-degree countersink, SK 90-degree countersink, SL ball-nosed cone, SM and SN taper shapes. The single (one-row) cut gives a smooth shearing action and a fine finish.
How It Works
At 6,000-50,000 RPM the single-cut flute peels material in continuous chips, producing a controlled finish with lower cutting pressure than double-cut styles.
Applications
Deburring, weld dressing, chamfering, contour finishing and engraving on steel, cast iron and stainless steel; head shape is selected to match the contour.
Suitable Materials
Steel, cast iron, stainless steel, copper, brass. Use aluminum-cut styles for soft non-ferrous material.
Field Cases
- Brass fitting shop: single-cut cylinder heads turn brass turning blanks down fast without the chatter a double cut introduces on free-machining brass.
- Cast-iron fettling: snatches riser pads off grey-iron castings; the long curling chip carries heat away from the edge.
- Repair shop: re-cuts a seized bolt slot on a mild-steel bracket where control of chip direction matters more than finish.
Performance Data
| Metric | Value / Observation |
|---|---|
| Removal per pass | Single cut removes the most material per pass on cast iron and steel (industry cutting data) |
| Best speed, 6 mm head | About 45,000 RPM starting in copper and cast iron |
| Grade note | YG-series integral carbide keeps edge integrity where HSS flutes roll over at 35 HRC |
| Control tip | Single cut pulls to one side – let the flute steer rather than forcing direction |
Material Comparison: Single Cut vs. Double Cut vs. Diamond Cut
Where the single-cut SA-SN series wins – typical industry data:
| Factor | Single Cut (this series) | Double Cut | Diamond Cut |
|---|---|---|---|
| Flute layout | One right-hand spiral | Right + left spiral | Jagged fine cross tooth |
| Chip formed | Long curling chip | Small broken chip | Micro chip |
| Cutting speed rating | Fastest removal per pass | Moderate | Fine finishing |
| Vibration feel | Higher – one edge family | Lower – balanced cutting | Lowest |
| Sweet spot | Cast iron, steel, copper, brass | Stainless, hardened steel | Hard-facing, hardened tools |
| Finish character | Clean, directional | Smooth, controlled | Very fine |
Delivery Scope
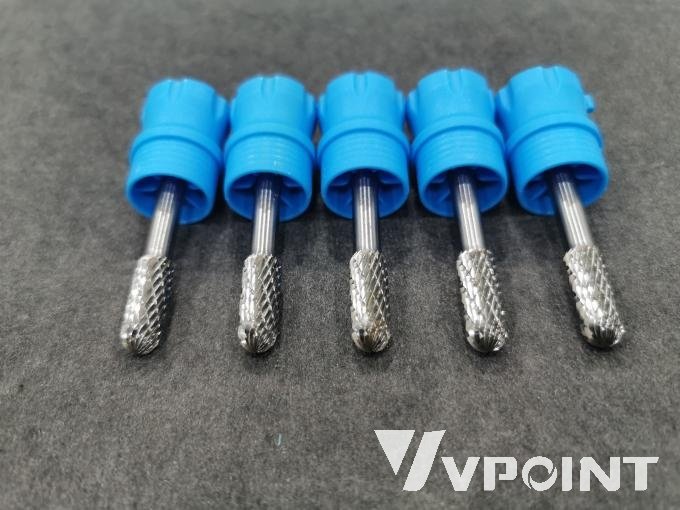
Single burr in a plastic tube; all 13 shapes can be supplied as a set. Custom shapes and laser marking on request.
Why Choose VPOINT
VPOINT TOOLS has manufactured precision cutting tools since 2008 in two production bases (Sichuan and Dongguan, China) under ISO 9001 quality management. Every carbide burr is supported by a one-year warranty, custom and non-standard engraving service, and regrinding service. Thirteen head geometries cover cylinder-to-flame contours without changing tools mid-job.
Precision & Quality Control
Each burr is checked for flute geometry, cutting-edge sharpness, shank runout and concentricity at micrometre level before packing; production batches are traceable and packed per ISO 9001 procedures.
Specifications
Available head geometries (single cut, 6 mm shank standard):
| Type | Head geometry |
|---|---|
| SA | Cylindrical shape |
| SB | Cylindrical with end cut |
| SC | Cylindrical ball nose |
| SD | Ball shape |
| SE | Oval shape |
| SF | Tree shape |
| SG | Pointed tree shape |
| SH | Flame shape |
| SJ | 60-degree countersink |
| SK | 90-degree countersink |
| SL | Ball-nosed cone |
| SM | Taper shape with radius end |
| SN | Taper shape with pointed end |

Frequently Asked Questions
Is the burr made of solid tungsten carbide?
Yes. The cutting head is integral tungsten carbide ground in the YG series grades.
Which shank sizes are available?
Standard shank is 6 mm (1/4″); other shank diameters and lengths are available on request.
What speed should I run the burr at?
Run between 6,000 and 50,000 RPM depending on the cutter diameter; use the lower end for larger diameters and the higher end for fine detail work.
Which materials can I machine with it?
Steel, cast iron, stainless steel, copper and brass; select aluminum-cut flutes for soft, gummy material.
Do you accept custom or non-standard sizes?
Yes. VPOINT supports custom shapes, sizes, shank lengths and laser marking on non-standard orders (minimum order quantity applies).
Related Search Terms
single cut carbide burr, SA-SN series rotary burrs, 13 shape carbide burr set, cylinder ball nose burr, single cut vs double cut burr, carbide burr for cast iron, weld dressing rotary burr, fabrication deburring tool, steel shaping burr, metal carving bits, maintenance rotary files, grinder attachment burrs, cnc deburring tool, machine shop burrs, industrial carbide burrs, tool steel grinding