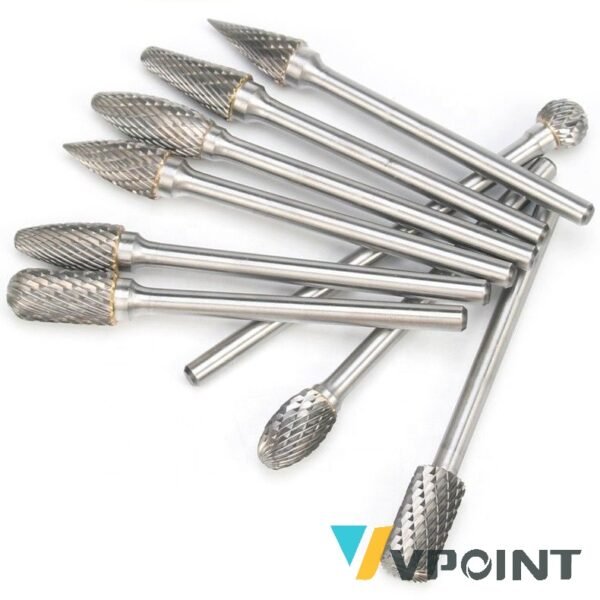
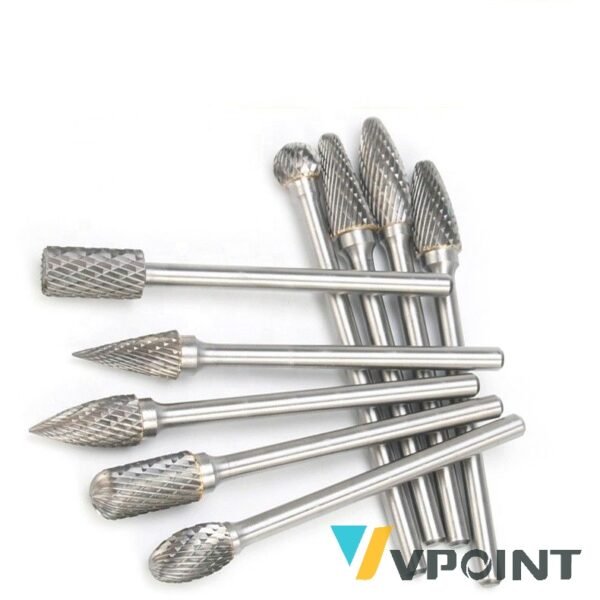
- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
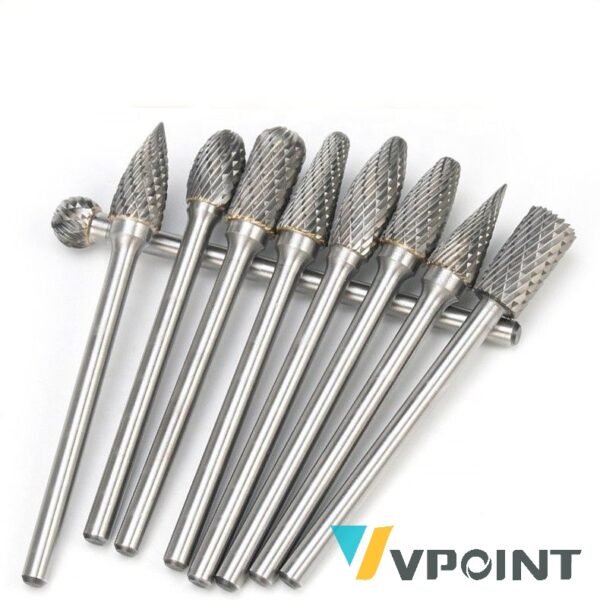

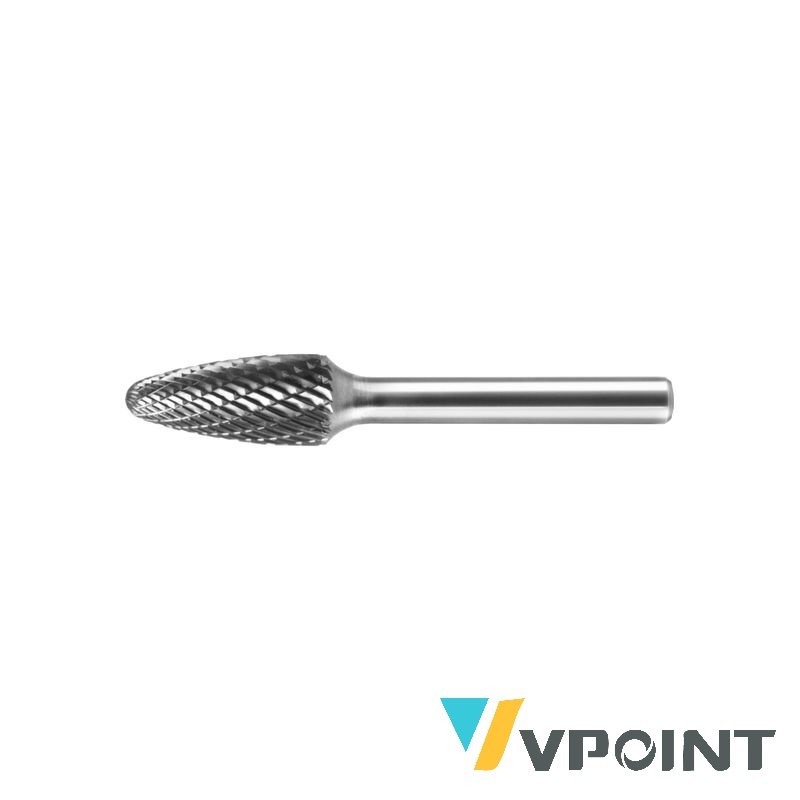
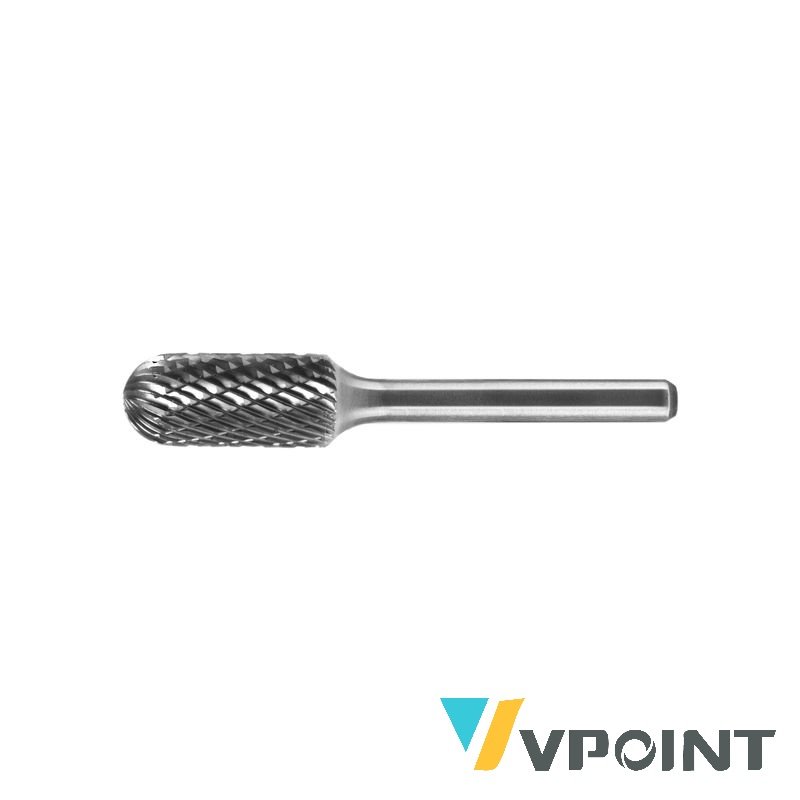
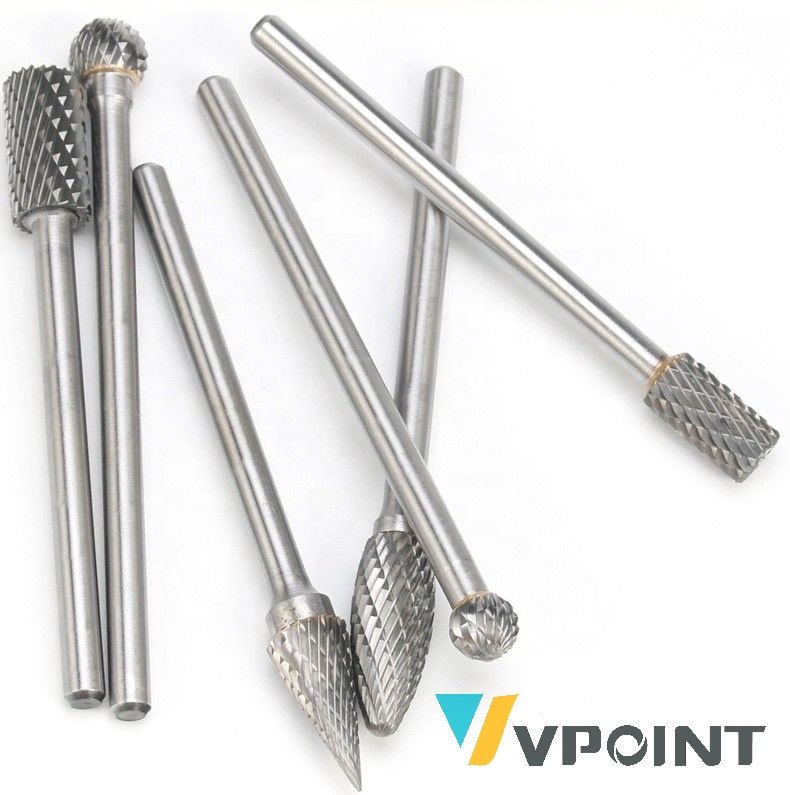
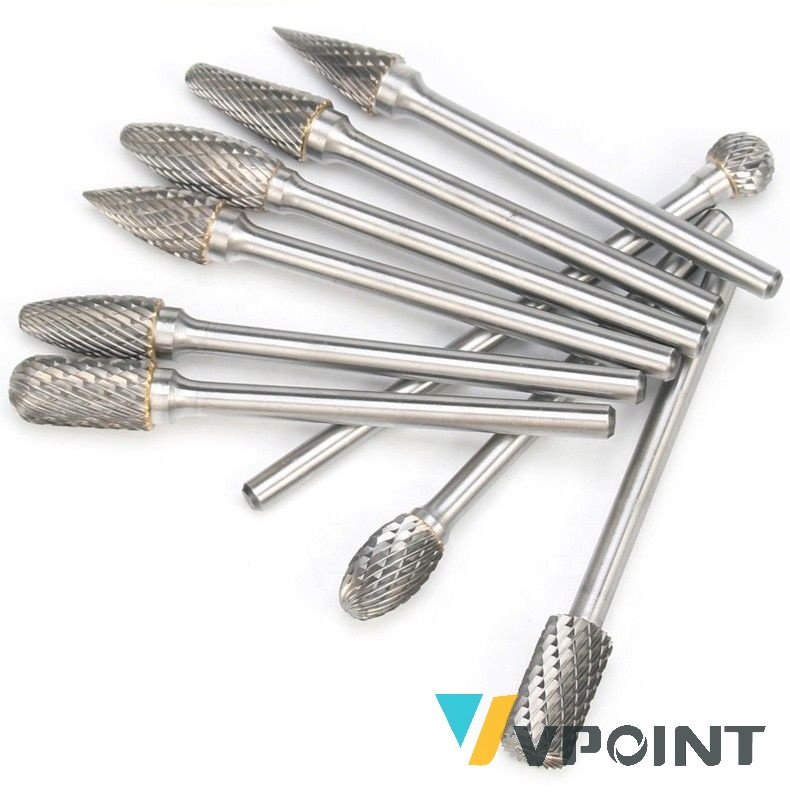
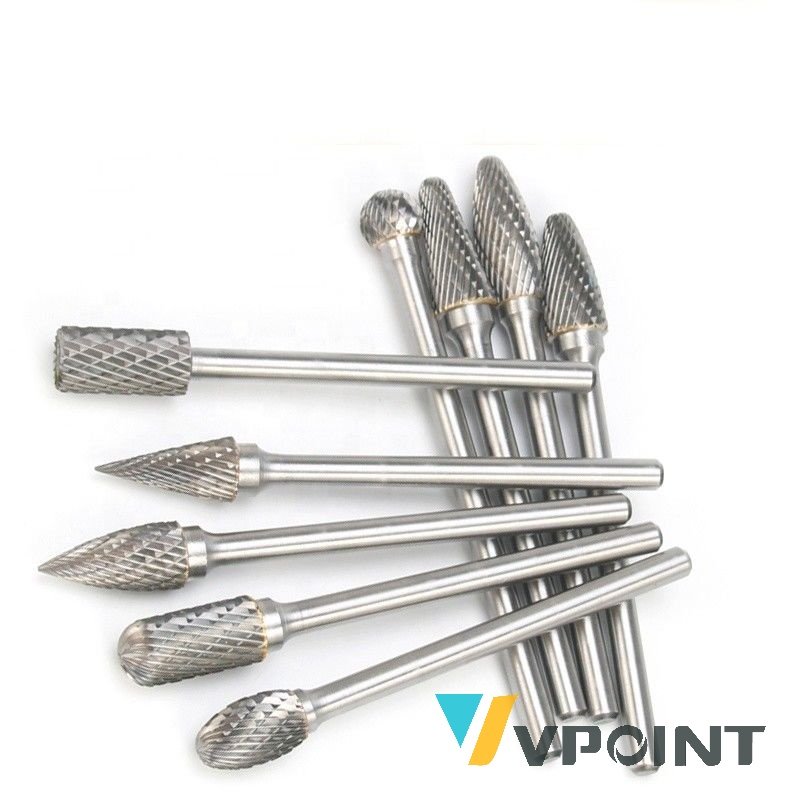
Design and Construction — a VPOINT long-shank carbide burr for deep cavities and reach work, sized for steel / stainless welds and similar work. YG8 carbide at HRA 89–91; die-grinder reference speeds are in the performance table below, with the flute-style guidance in the FAQ. ISO 9001 production, batch-verified, custom sizes from drawings.
Design and Construction
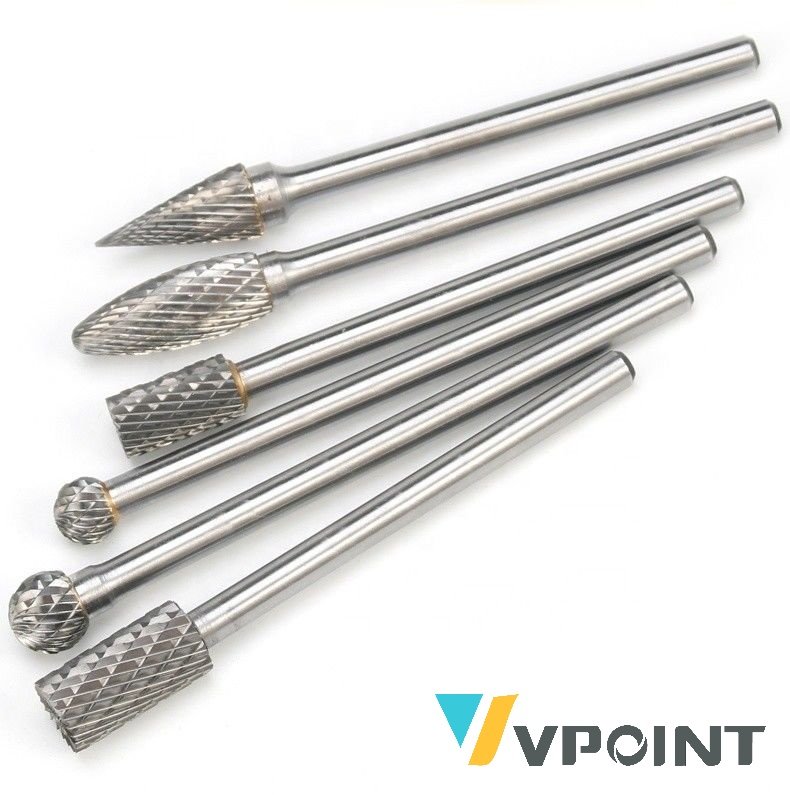
A standard double-cut long-shank carbide burr. The double-cut flute pattern breaks chips into small segments, which matters most in a deep recess where a long chip cannot escape past the head and shank.
How It Works
In a deep cavity the cut is limited by chip removal rather than by spindle power. Air blast, vacuum extraction and periodic pecking are the three practical routes; the double-cut pattern makes all three more effective by shortening the chip.
Applications
Deep pocket deburring, cast recess cleanup, internal weld dressing, enclosed cavity work.
Field Cases
- Foundry: air blast through the cavity kept the flutes clear on a deep recess.
- Fabrication: short peck cycles prevented chip packing on an internal weld.
- Die shop: vacuum extraction kept the working area visible during a long pass.
Performance Data
| Metric | Value / Observation |
|---|---|
| Cut pattern | Double cut (cross-cut flutes) |
| Chip form | Short, broken segments |
| Evacuation routes | Air blast / extraction / pecking |
| Limiting factor | Chip removal in deep recesses |
Suitable Materials
Cast iron, carbon and alloy steel, stainless steel, aluminium and non-ferrous alloys.
Standard reference values for guidance only — always adjust to the workpiece material, the machine spindle speed and the feed, and confirm on the actual part.
Material Comparison: Chip Evacuation: Air Blast vs Extraction vs Pecking
Three routes for clearing a deep cavity. Typical industry practice:
| Factor | Air Blast | Vacuum Extraction | Pecking / Retract |
|---|---|---|---|
| How chips leave | Blown out of the cavity | Sucked away at source | Retracted with the tool |
| Equipment needed | Compressed air | Vacuum / extraction unit | None |
| Visibility of the cut | Reduced by airborne dust | Best | Intermittent |
| Cycle time impact | None | None | Slightly longer |
| Best cavity | Open-ended recess | Enclosed cavity | Blind hole |
| Works with double cut | Yes | Yes | Yes |
Delivery Scope
Single burr; head shape, shank diameter and reach confirmed with the order.
Why Choose VPOINT
Deep work fails on chip packing, not power – the flute pattern and evacuation route are stated together.
Precision & Quality Control
Flute geometry, braze concentricity and head runout verified per lot with full batch traceability.
Specifications
Published specification:
| Item | Specification |
|---|---|
| Type | Standard double cut long shank burr |
| Flute | Double cut / cross-cut |
| Chip form | Short segments |
| Evacuation | Air, extraction or pecking |
| Workpiece | Cast iron, steel, stainless, aluminium |
| Inspection | Per-lot flute geometry |
Frequently Asked Questions
How deep can the long-shank version reach?
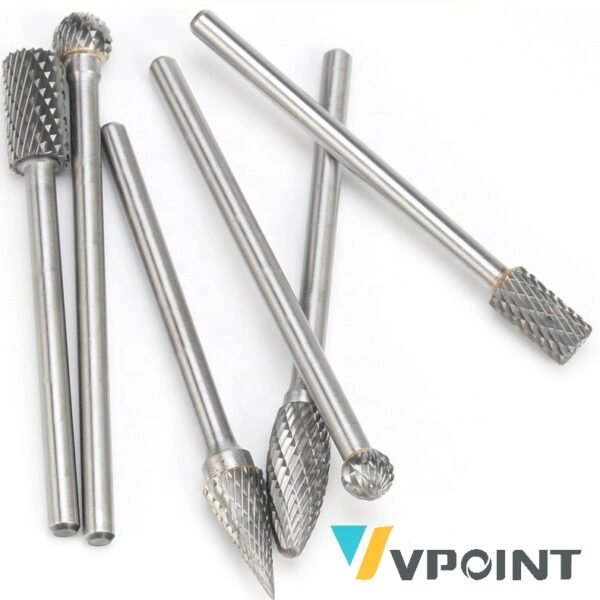
100, 150, 200 and 300 mm reach classes — pick the shortest reach that gets you there, because reach amplifies any collet runout.
How do I keep it from chattering?
Seat the shank fully, use light pressure, and let the flutes clear — long tools punish heavy hands.
Same head codes as standard burrs?
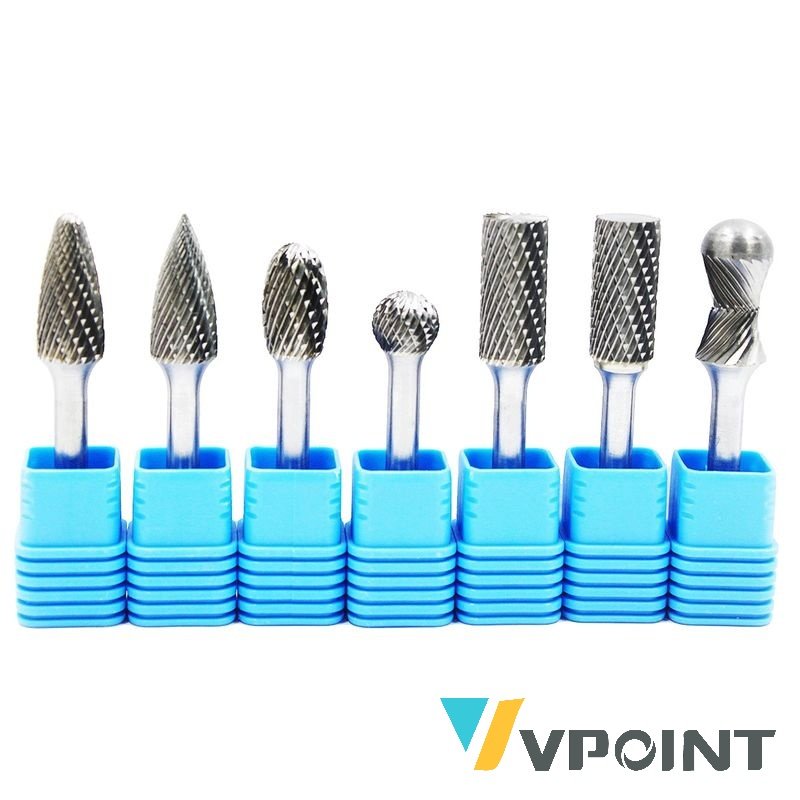
Yes — SA–SM contours carry over, so a long-shank burr matches the shape you already run on short shanks.
Why double cut for deep work?
It breaks chips into short segments that escape past the head instead of packing in the recess.
Which evacuation route is best?
Air blast for open recesses, extraction for enclosed cavities, pecking for blind holes.
Does pecking slow the job?
Slightly, but it prevents chip packing and tool loading on blind features.
Which materials?
Cast iron, steel, stainless, aluminium and non-ferrous alloys.
Is flute geometry checked?
Yes, per production lot with batch traceability.
Related Search Terms
double cut long shank burr, deep recess carbide burr, chip evacuation burr, cross cut extended burr, air blast die grinder, vacuum extraction burr, peck cycle deburring, cast recess cleanup tool, internal weld dressing burr, short chip carbide burr, blind hole rotary burr, double cut pattern, long shank flute clearing, deep pocket burr, chip packing prevention
Key words: carbide rotary burr, rotary burr set, double cut carbide burr, aluminium cut burr, tire reamer bit, burr blanks, carbide burr 6mm shank, TiAlN coated burr, rotary file, carbide burr for steel, carbide burr for aluminum, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, metal deburring, weld seam removal, weld cleanup, weld bead blending, weld bevel prep, porting cylinder heads, engine port work, casting cleanup, mould and die work, mold polishing, fabrication cleanup, plasma-cut edge smoothing, mill scale removal, rust removal, tube notching, exhaust weld grinding, frame repair, tool and die, art metalwork, knife making, steel deburring, stainless steel finishing, cast iron repair, aluminum porting, non-ferrous shaping, hardened steel grinding
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification