- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide Particles
- Carbide Composite Rods
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling


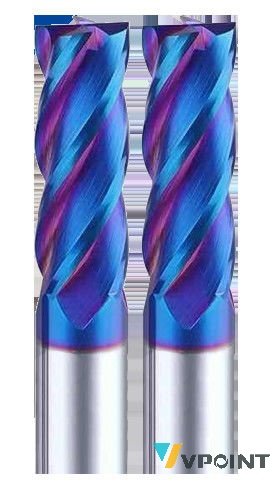
Design and Construction
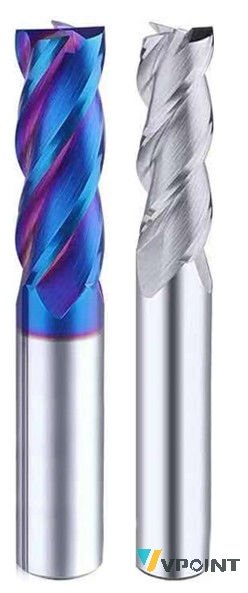
A DLC-coated flat tungsten carbide end mill offered across a 1-10 flute range. The flat end produces a square pocket floor; flute count is the selectable variable that sets chip space, core diameter and the number of cutting edges engaged.
How It Works
A single flute clears the largest chip and suits soft, gummy materials at high feed; two to four flutes are the general-purpose range for steel; six or more flutes suit shallow finishing passes in harder materials where chip volume is small. The DLC coating reduces friction in stainless steel.
Applications
Carbon steel and stainless CNC milling, flat-bottom pockets, finishing with high flute counts, gummy materials with low flute counts.
Field Cases
- Stainless shop: a higher flute count improved finish on a shallow flat-bottom pass.
- Jobbing cell: a low flute count cleared long chips in gummy material without clogging.
- Pocket work: the flat end produced a square floor in a single pass.
Performance Data
| Metric | Value / Observation |
|---|---|
| Flute range | 1 to 10 |
| End geometry | Flat / square |
| Coating | DLC |
| Primary materials | Carbon steel, stainless steel |
Suitable Materials
Carbon steel and stainless steel primarily; low flute counts also suit aluminium and copper alloys where chip volume is high.
Material Comparison: Flute Count Selection: 1 / 2-4 / 6-10
Choosing flute count by chip volume and material. Typical industry practice:
| Factor | 1 Flute | 2-4 Flutes | 6-10 Flutes |
|---|---|---|---|
| Chip space per flute | Largest | Moderate | Smallest |
| Core diameter | Smallest | Moderate | Largest |
| Cutting edges engaged | One | Two to four | Six or more |
| Best chip type | Long, gummy chips | Steel chips | Fine finishing chips |
| Typical axial engagement | Deep | General | Shallow |
| Finish potential | Adequate | Good | Best |
| Best workpiece | Aluminium, copper, plastics | Carbon and stainless steel | Hardened steel finishing |
Delivery Scope
Single end mill; flute count and diameter confirmed with the order.
Why Choose VPOINT
Flute count is a published option from 1 to 10, so the tool fits the material rather than forcing one geometry.
Precision & Quality Control
Flute spacing, edge preparation, coating adhesion and runout verified per lot with ISO 9001 batch traceability.
Specifications
Published specification:
| Item | Specification |
|---|---|
| Type | DLC coated flat end mill |
| Flute options | 1 to 10 |
| End geometry | Flat / square |
| Coating | DLC |
| Workpiece | Carbon steel, stainless steel |
| Inspection | Per-lot flute spacing and coating check |
Frequently Asked Questions
How many flutes should I choose?
Low counts clear large chips in gummy materials; 2-4 is general steel work; 6-10 suits shallow finishing passes.
Why DLC for stainless?
The low-friction coating reduces built-up edge in sticky stainless steels.
Does the flat end leave a square floor?
Yes – the flat end produces a square pocket floor with sharp internal corners.
Can a 10-flute tool slot?
Not recommended – chip space is too small for a full-width slot.
What is verified per lot?
Flute spacing, edge preparation, coating adhesion and runout.
Related Search Terms
1 to 10 flute end mill, DLC coated flat end mill, flute count selection, carbon steel CNC end mill, stainless steel milling cutter, single flute end mill, high flute count finishing, 6 flute end mill, flat bottom pocket cutter, DLC stainless milling, chip space flute count, gummy material end mill, square end DLC cutter, variable flute end mill, CNC flat end mill