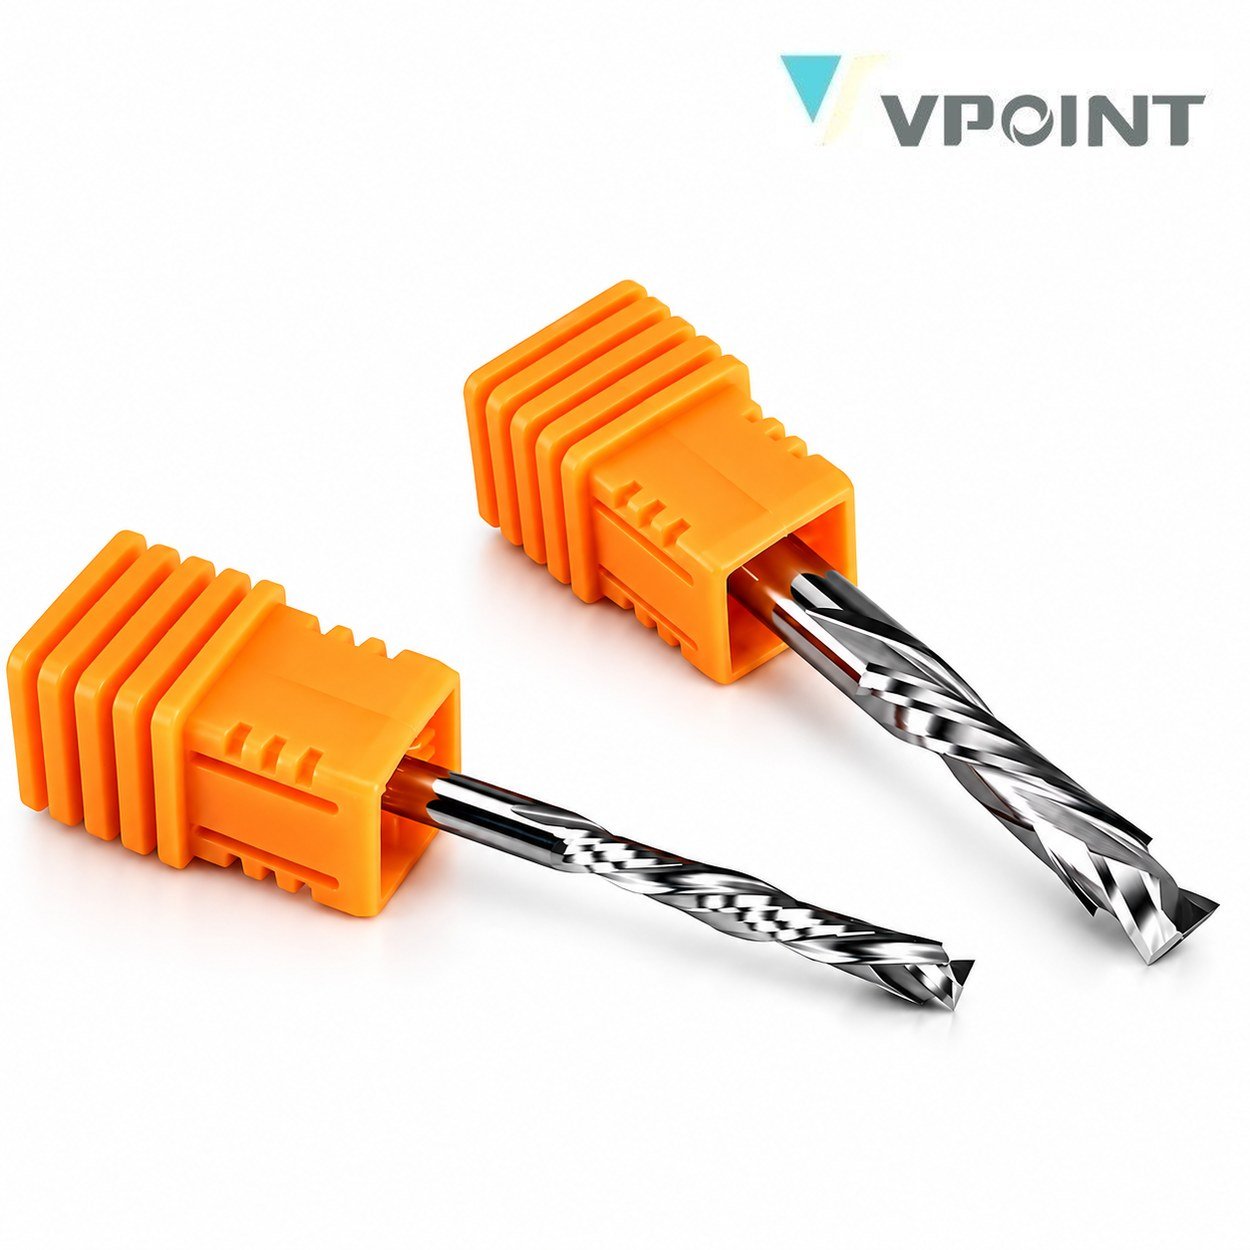
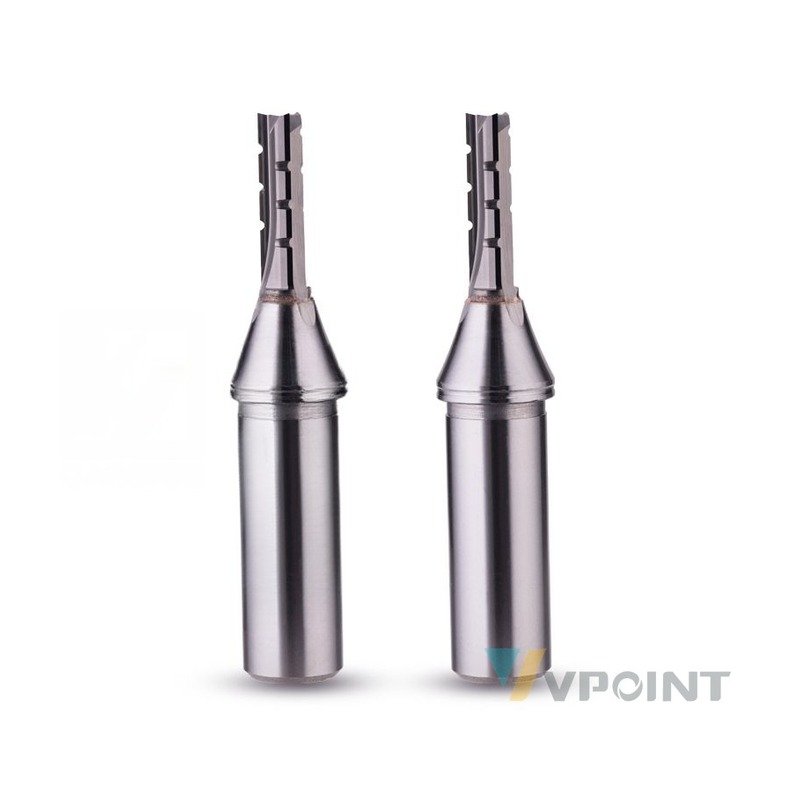
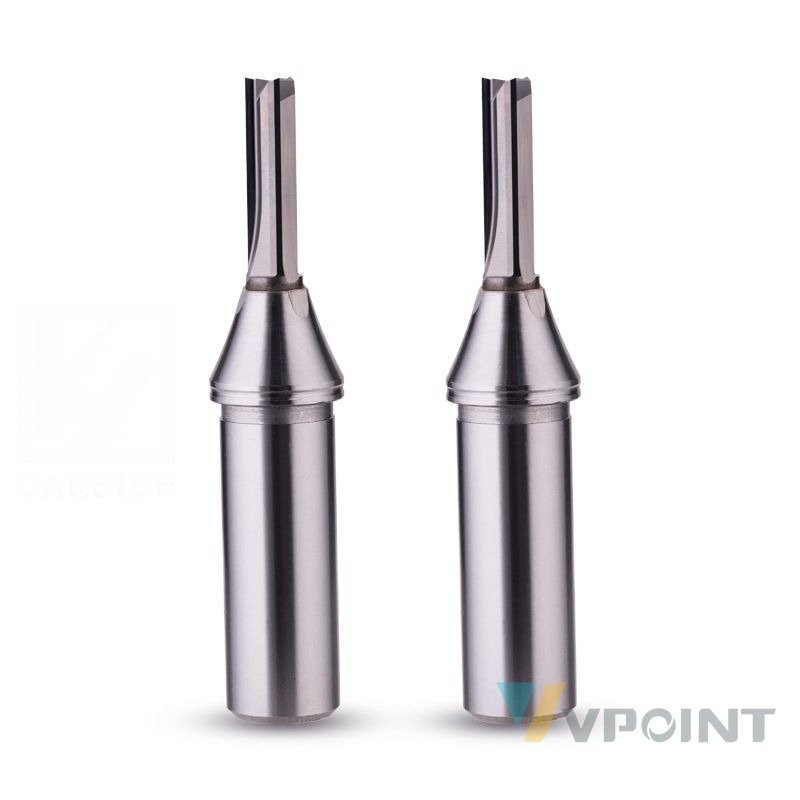
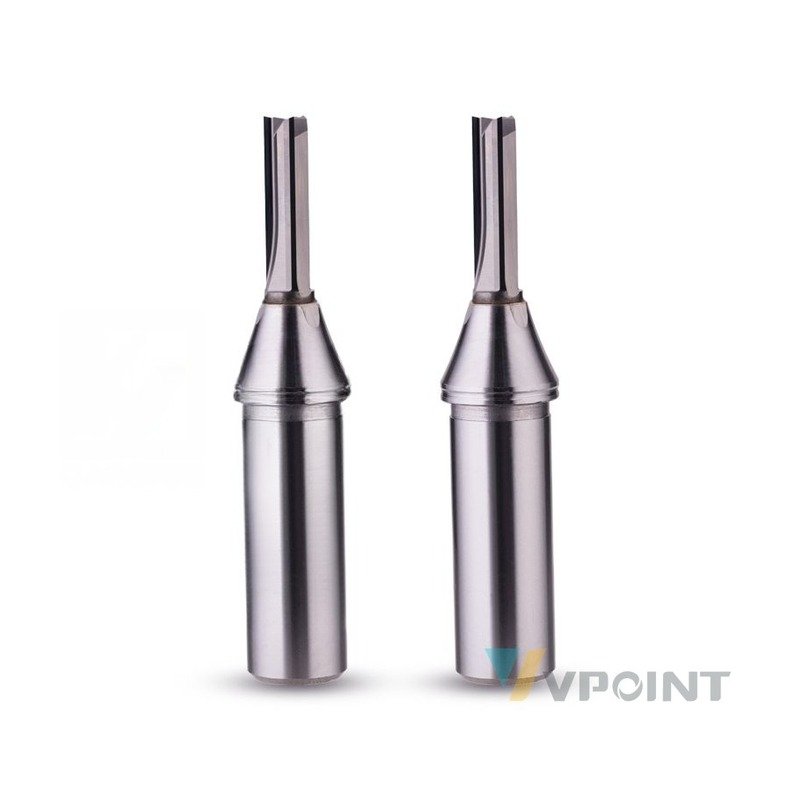
Solid Carbide Two-Flute Compression Router Bit for Woodworking Production
This solid carbide compression router bit combines opposing spiral cutting sections for routing panel materials, offered in cutting diameters from 1 to 12 mm with matching cutting lengths and shanks. Two flutes clear chips in both directions of the compression cut.
Design and Construction
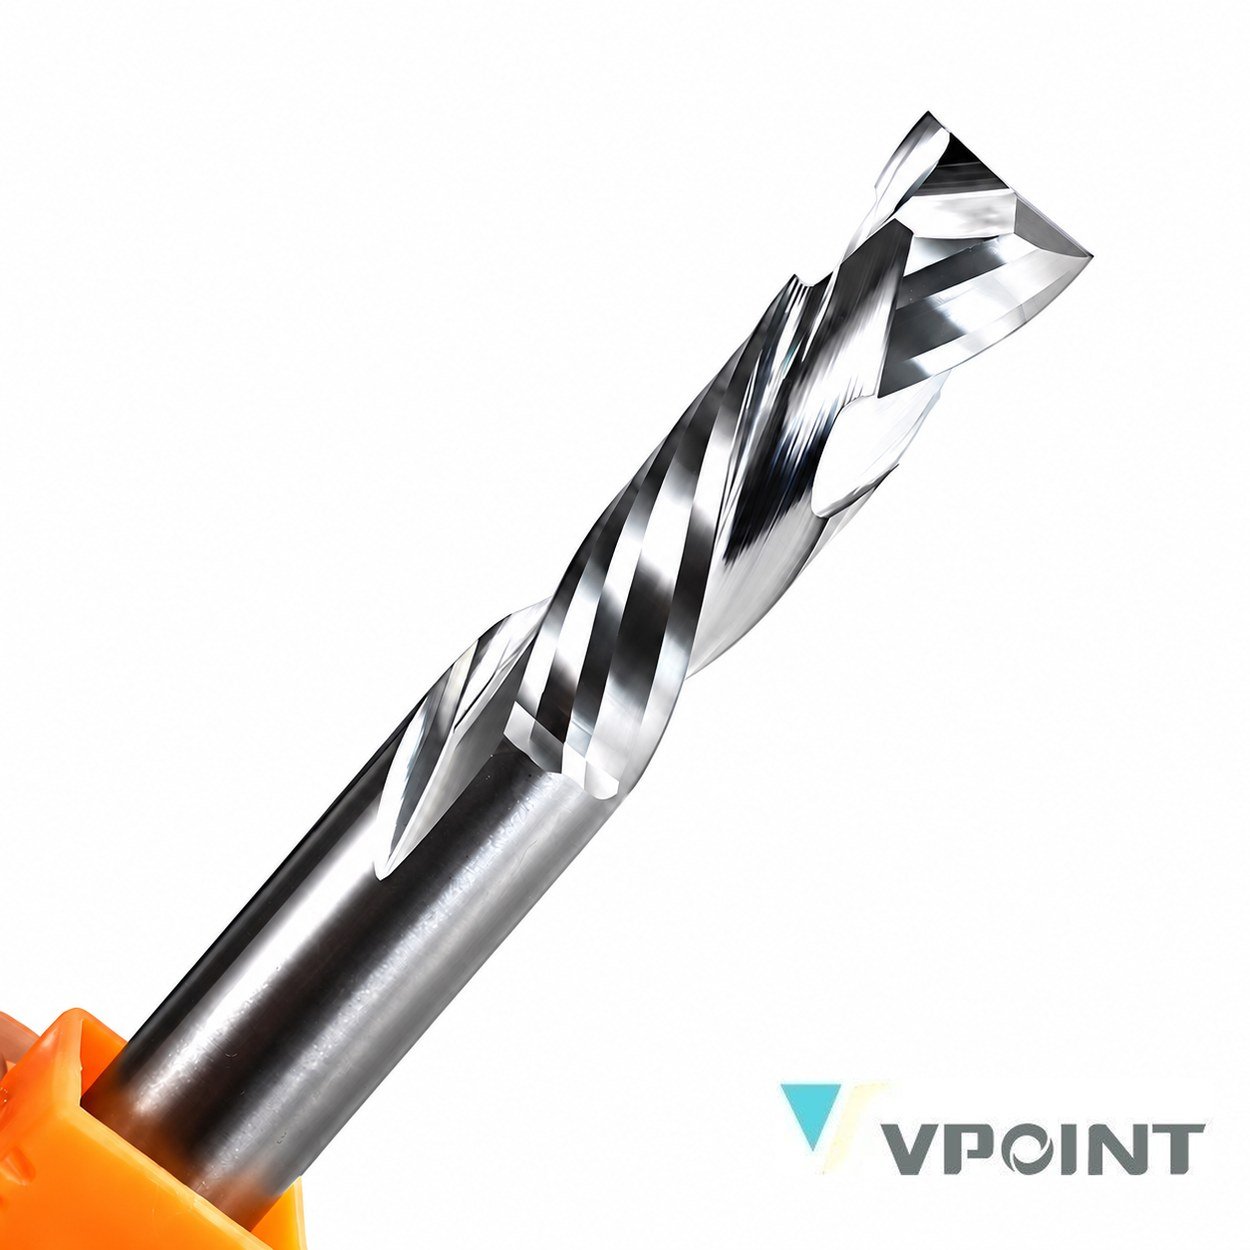
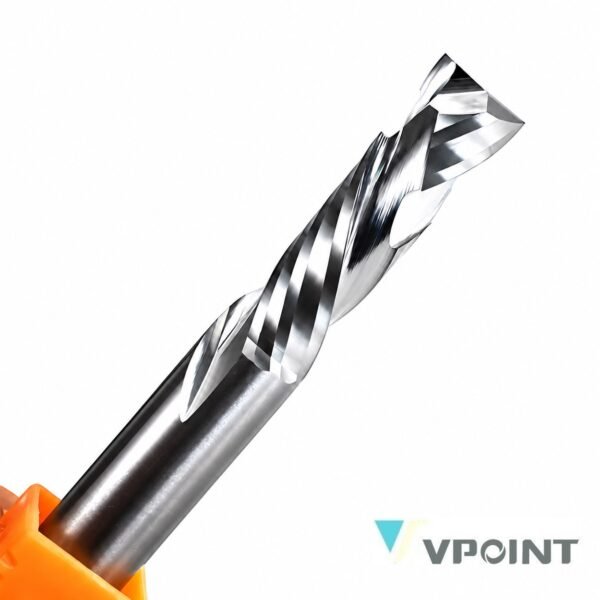
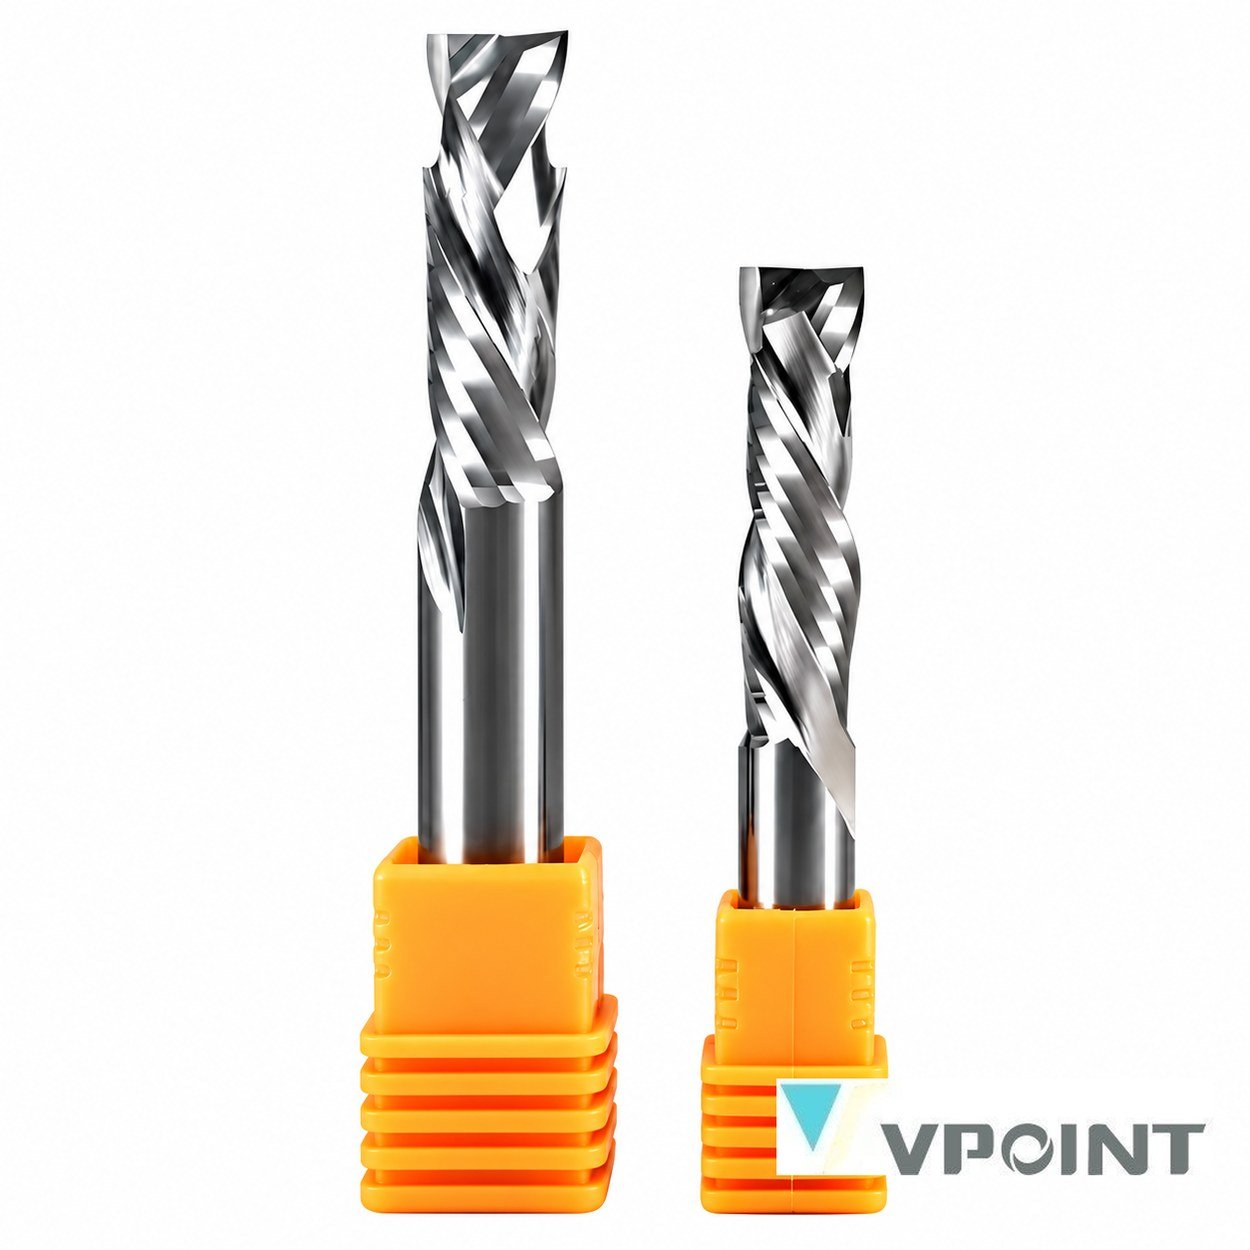
+The lower section shears upward and the upper section shears downward, pressing fibres toward the panel core — the compression geometry that keeps both faces clean in one pass. The chart lists cutting diameters 1–12 mm, cutting lengths 4–42 mm, shank diameters 3.175, 4, 6 and 8 mm and overall lengths 38–75 mm as complete configurations. The series is produced in the Sichuan and Dongguan, China manufacturing bases.
How It Works
+In the CNC router the bit plunges and traces the nesting path at full panel depth: the up-shear section holds the bottom veneer while the down-shear section holds the top coating. The two flutes evacuate chips from both directions, and the solid-carbide body keeps the compression transition stable through long nesting runs.
Applications
- Compression (up-down shear) routing of nested panels on CNC routers, engraving machines and precision engraving equipment
- Through-cutting veneered board, plywood, MDF, particleboard and selected plastic boards including PVC
Suitable Materials
- Veneered board, plywood, MDF, particleboard and selected plastics including PVC, subject to grade and application review
- Suitability depends on the specific material grade, panel thickness and machining parameters; confirm the application before ordering
Material Comparison: High-Speed Steel (HSS) Tool vs. Solid Carbide Tool
+Typical industry data for reference. Actual results depend on the workpiece grade, machine condition and feed rate.
| Property |
High-Speed Steel (HSS) Tool |
Solid Carbide Tool |
| Cutting edge hardness |
≈ 60–65 HRC (HSS) |
1,500–2,000 HV (solid carbide) |
| Heat resistance of the edge |
Loses hardness above ≈ 315 °C |
Retains hardness up to ≈ 1,000 °C |
| Edge life on abrasive panels |
Baseline (1×) |
5–10× longer edge life |
| Feed rate at equal quality |
Lower |
Higher |
| Sharpness retention on MDF / particleboard |
Dulls quickly |
Holds the edge through long runs |
| Regrinding cycles over tool life |
Limited |
More regrinds |
| Cut edge quality as the edge wears |
More fuzzing and tearout |
Consistent clean walls |
| Rigidity in long tools |
Lower |
Higher (solid carbide body) |
| Typical machines |
Light-duty routers and drills |
CNC machining centres, multi-spindle borers |
| Cost per hole / metre of cut |
Higher over long runs |
Lower over long runs |
Delivery Scope
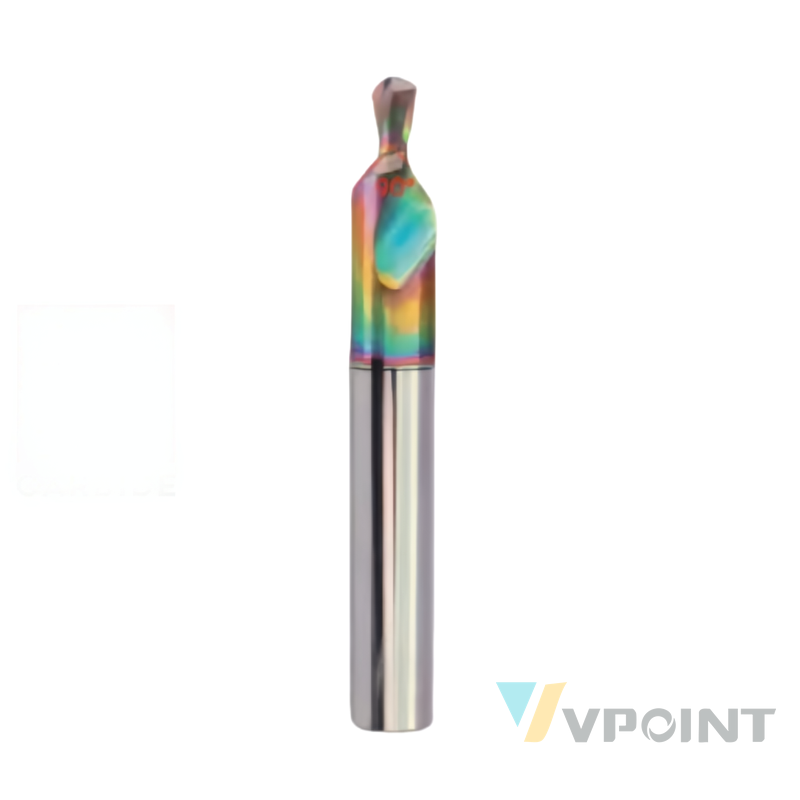
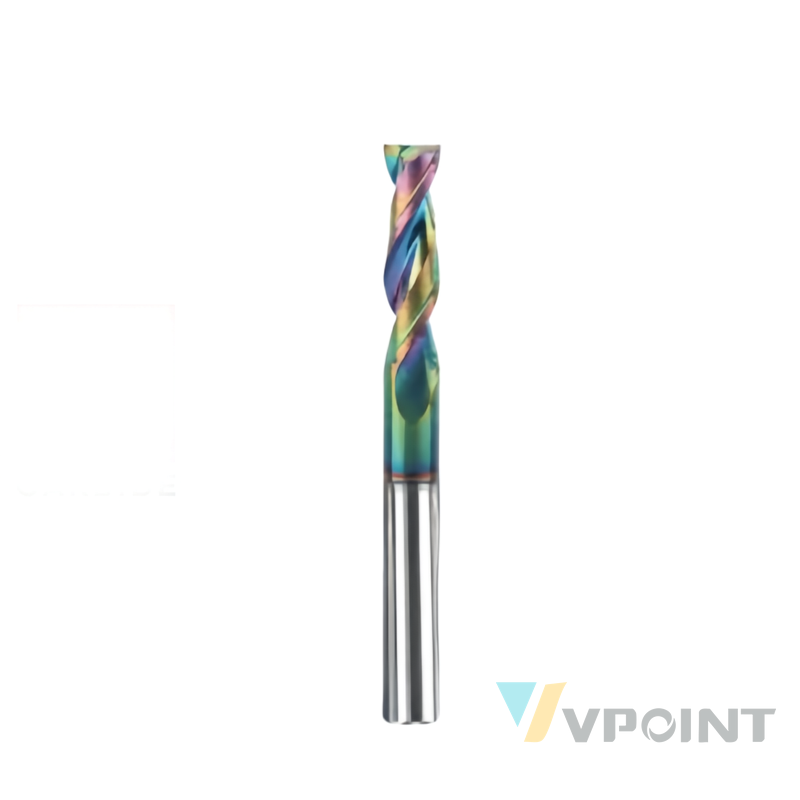
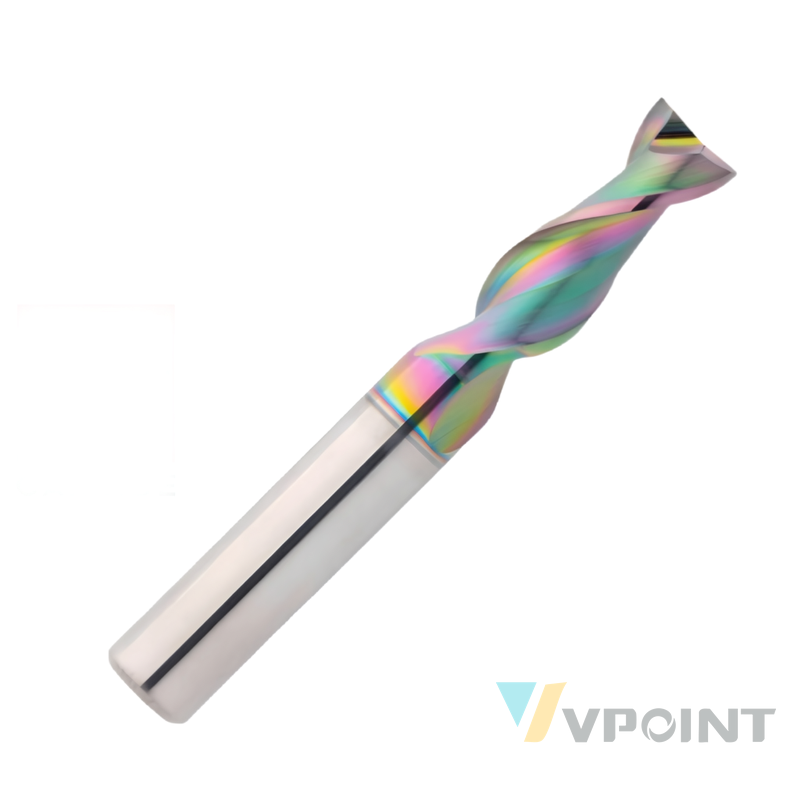
Select a complete table row — dimensions from different rows are not combined. The gallery shows silver-finish cutters and a coated option; confirm the finish when ordering (the coating chemistry is not specified).
+Each order also includes an inspection record. Send the panel type and thickness, required cutting diameter and cutting length, collet/shank size, CNC machine model and cutting operation, and confirm the compression transition point for through-cutting.
Why Choose VPOINT
+VPOINT supports this carbide tool series with:
- One-year warranty on every tool
- Custom diameters, shanks and rotations produced to order
- Regrinding service to extend tool life
- Factory direct since 2008, ISO 9001 certified
- Dual manufacturing bases in Sichuan and Dongguan, China
Precision & Quality Control
+Every compression router bit is inspected before shipment: cutting diameter, shank diameter and tool runout are checked against the specification table at micron level. Production follows an ISO 9001 process with batch traceability, so reorders match the original configuration.
Specifications
The table below reproduces the original specification chart. Dimensions are in millimetres; each row is a complete configuration (d = cutting diameter, h = cutting length, D = shank diameter, L = overall length).
| C |
u |
t |
t |
i |
n |
g |
|
d |
i |
a |
m |
e |
t |
e |
r |
|
d |
|
( |
m |
m |
) |
| C |
u |
t |
t |
i |
n |
g |
|
l |
e |
n |
g |
t |
h |
|
h |
|
( |
m |
m |
) |
| S |
h |
a |
n |
k |
|
d |
i |
a |
m |
e |
t |
e |
r |
|
D |
|
( |
m |
m |
) |
| O |
v |
e |
r |
a |
l |
l |
|
l |
e |
n |
g |
t |
h |
|
L |
|
( |
m |
m |
) |
| 3 |
. |
1 |
7 |
5 |
| 1 |
2 |
| 3 |
. |
1 |
7 |
5 |
| 3 |
8 |
| 3 |
. |
1 |
7 |
5 |
| 1 |
7 |
| 3 |
. |
1 |
7 |
5 |
| 3 |
8 |
| 3 |
. |
1 |
7 |
5 |
| 2 |
2 |
| 3 |
. |
1 |
7 |
5 |
| 4 |
5 |
| 3 |
. |
1 |
7 |
5 |
| 2 |
5 |
| 3 |
. |
1 |
7 |
5 |
| 5 |
0 |
| 3 |
. |
1 |
7 |
5 |
| 2 |
8 |
| 3 |
. |
1 |
7 |
5 |
| 5 |
0 |
| 3 |
. |
1 |
7 |
5 |
| 3 |
2 |
| 3 |
. |
1 |
7 |
5 |
| 5 |
5 |
Frequently Asked Questions
Which diameters and shanks are listed?
+The chart lists cutting diameters from 1 to 12 mm, cutting lengths from 4 to 42 mm, shank diameters of 3.175, 4, 6 and 8 mm and overall lengths from 38 to 75 mm, as complete configurations.
Can rows be mixed?
+No. Each table row is one complete configuration; dimensions from different rows are not combined.
What panel thickness suits compression routing?
+The compression transition point must sit within the panel thickness. Send the panel type and thickness so the cutting length and transition are confirmed for through-cutting.
What should I send for a quotation?
+Panel type and thickness, required cutting diameter and cutting length, collet/shank size, CNC machine model and cutting operation, plus the finish (silver or coated).
+Key words: solid carbide compression router bit, two flute compression bit, CNC nesting bit, up down shear router bit