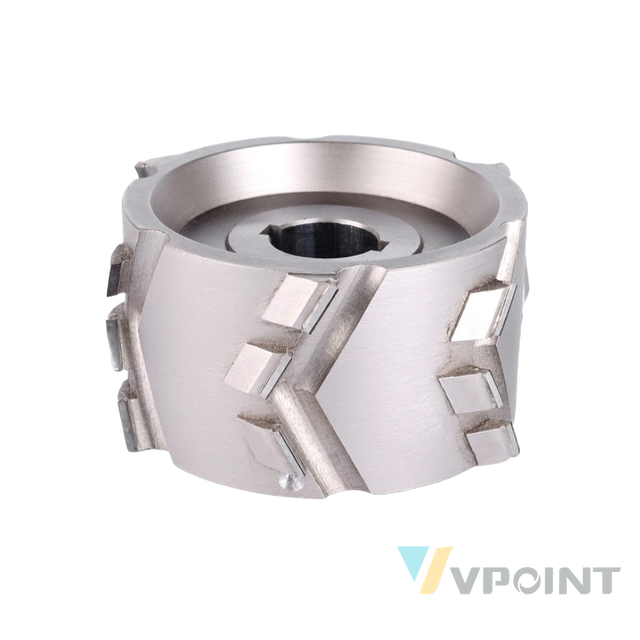
Aluminum Body Pre-Milling Cutter with PCD Inserts for Edge Banding Machines — a VPOINT end mill tool for CNC milling, sized for MDF and similar workpieces. The specification table below lists dimensions; the performance data table gives standard reference speeds and feeds to start with, and the FAQ covers selection, parameters and service. ISO 9001 production, batch-verified, custom sizes from drawings.
Aluminum Body Pre-Milling Cutter with PCD Inserts for Edge Banding Machines
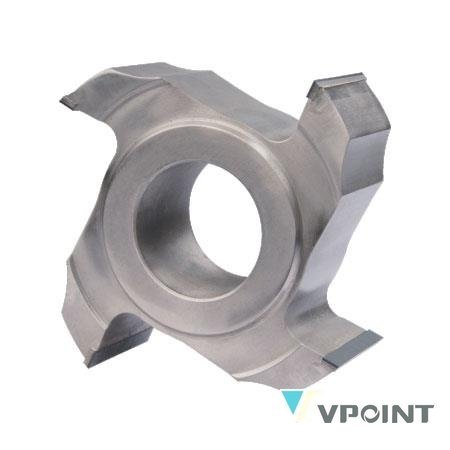
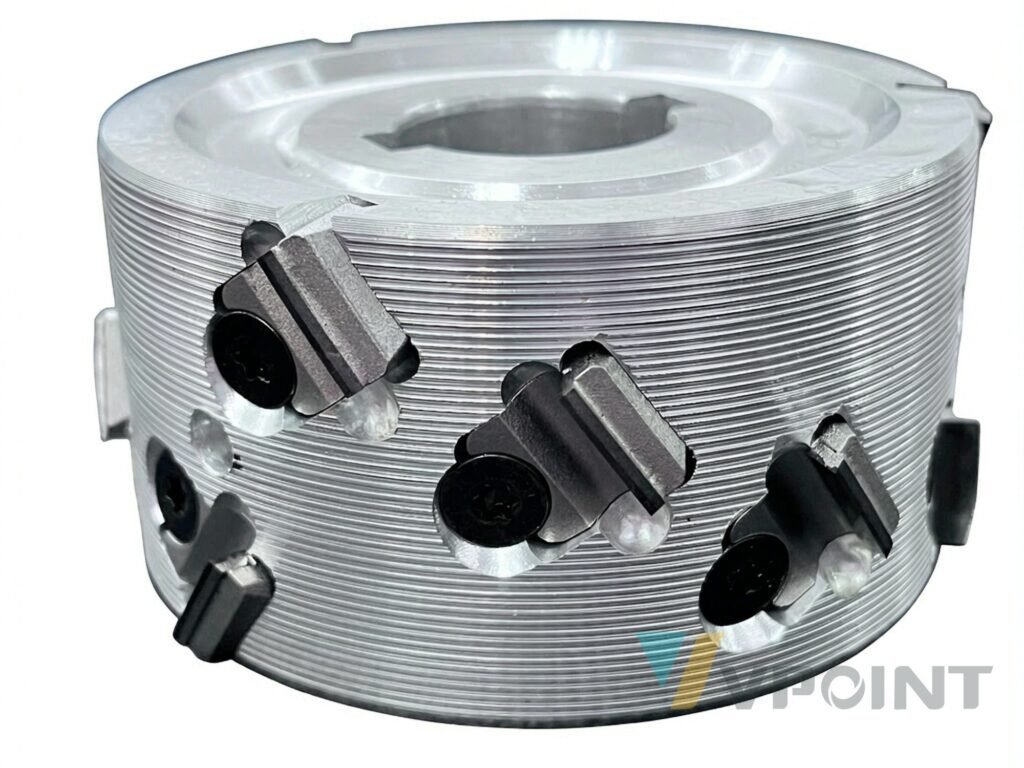
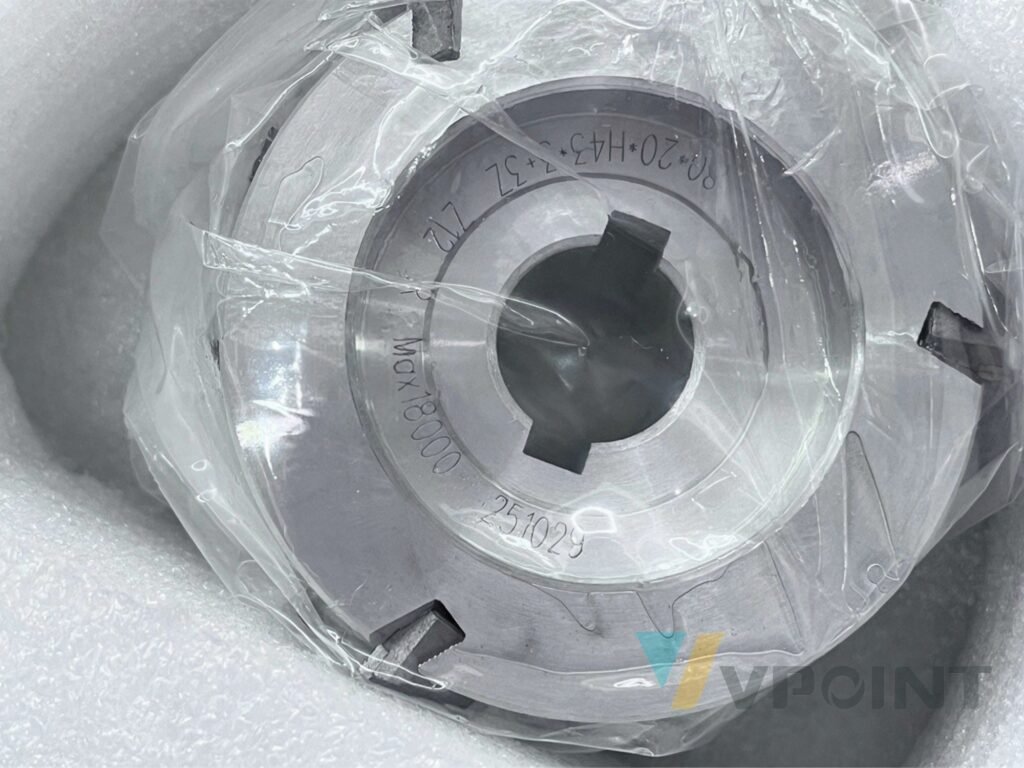
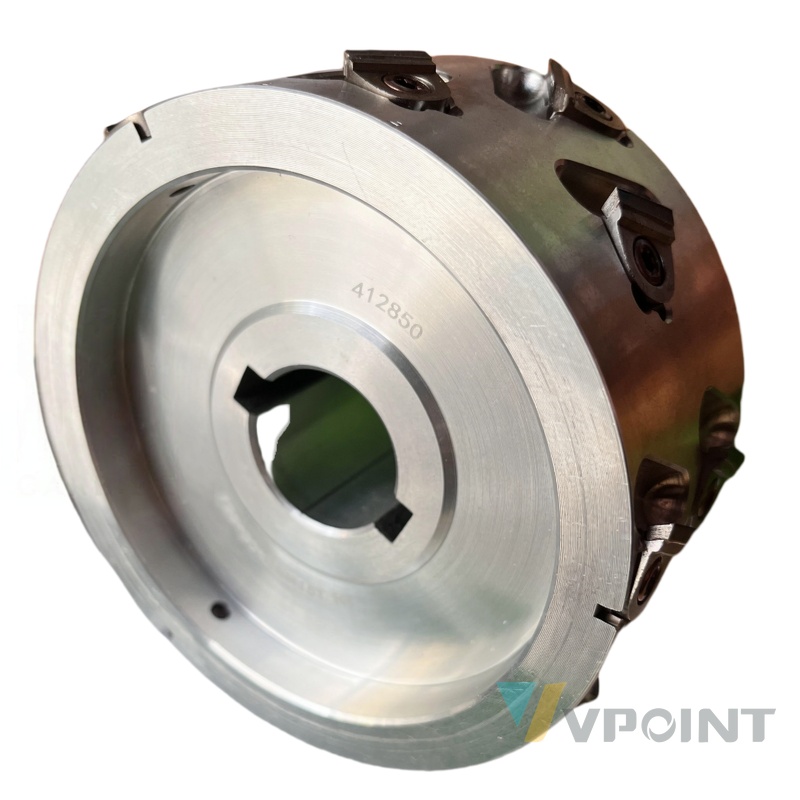
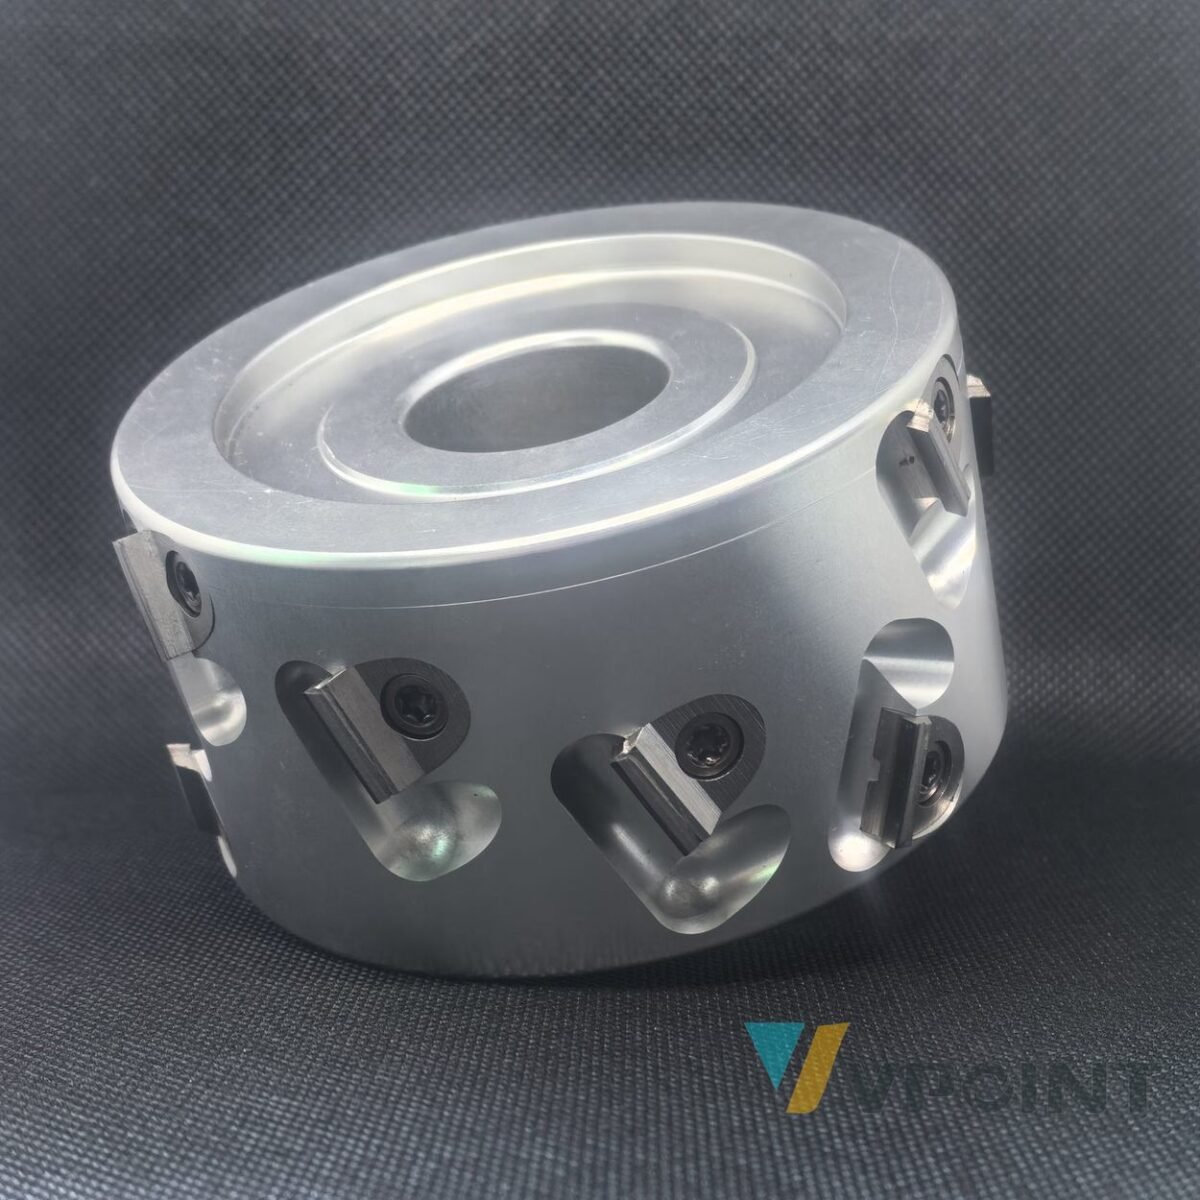
This aluminum-body pre-milling cutter uses detachable PCD inserts for panel-edge preparation before edge banding. The body is machined from aluminum with a hardened surface, and the cutting inserts are mounted in machined seats with mechanical fixing.
Design and Construction
The aluminum cutter body has a hardened surface and detachable cutting inserts held in precision-machined seats. Insert removal allows replacement or regrinding to be assessed separately from the body; confirm the insert design and service condition before reuse.
How It Works
In operation the inserts present the PCD cutting edge to the panel surface as the cutter rotates in the pre-milling unit. Worn or damaged inserts are removed individually, so the body is retained and only the inserts are replaced or reconditioned, reducing long-run tooling cost.
Applications
- Pre-milling on edge banding machines with insert-type cutter heads
- Panel furniture and cabinet production
- Applications where insert replacement is preferred over solid-head replacement
Suitable Materials
- MDF and density fibreboard
- Veneered panels and composite boards
- Calcium-silicate board — reviewed case by case
Material Comparison: Tungsten Carbide vs. Diamond (PCD) Cutter Head
Typical industry data for reference. Actual results depend on the panel grade, machine condition and feed rate.
| Property |
Tungsten Carbide Cutter Head |
Diamond (PCD) Cutter Head |
| Cutting material hardness |
1,500–2,000 HV |
7,000–9,000 HV |
| Service life on MDF / particleboard |
Baseline (1×) |
10–20× longer edge life |
| Regrinding / refurbishing cycles |
2–4 times |
5–8 times |
| Cut edge quality |
Ra 0.4–0.8 µm, more fuzzing |
Ra 0.2–0.4 µm, cleaner edge |
| Thermal conductivity |
≈ 100 W/m·K |
≈ 500 W/m·K, heat cleared faster |
| Friction coefficient |
≈ 0.3 |
≈ 0.05–0.1, lower cutting force |
| Chipping risk on brittle panels |
Higher at high feed |
Lower, stable edge at high feed |
| Cutter change frequency |
More frequent |
Fewer changes, less downtime |
| Cost per metre of edge |
Higher over long runs |
Lower over long runs |
Delivery Scope
Each order includes the selected cutter head configuration, protective packaging and an inspection record. Matched pairs, keyed bores and non-standard heights are produced to order after the machine details are confirmed.
Why Choose VPOINT
- One-year warranty on every cutter head
- Custom and non-standard sizes supported, including keyed bores and matched pairs
- Regrinding service to extend tool life
- Factory direct since 2008, ISO 9001 certified
- Dual manufacturing bases in Sichuan and Dongguan, China
Precision & Quality Control
Every cutter head is inspected at micron level before shipment: bore diameter, mounting runout, body concentricity and insert seat geometry are checked against the drawing. Production follows an ISO 9001 process with batch traceability, so reorders match the original configuration.
Specifications
Send the body diameter, bore, cutting height, insert arrangement, rotation and edge-bander model with the enquiry. For insert replacement or regrinding, include photos of the body and the existing insert seats so the configuration is confirmed.
Performance Data
Standard reference values for guidance only — always adjust to the edge bander feed, machine condition and tool wear, and confirm on the actual panel.
| Material |
Typical spindle speed |
Typical feed |
Notes |
| MDF |
20,000–24,000 rpm |
12–18 m/min |
PCD premill heads hold edge on abrasive MDF |
| particleboard |
18,000–22,000 rpm |
12–18 m/min |
Grit-resistant diamond edges for long runs |
| veneered composite panels |
18,000–20,000 rpm |
10–14 m/min |
Two-stage 2+2 / 3+3 geometry |
| solid wood edge bands |
16,000–20,000 rpm |
10–14 m/min |
Adjust per feed of the edge bander |
Frequently Asked Questions
Are the inserts replaceable?
Yes. The PCD inserts are detachable and can be replaced or sent for regrinding separately from the aluminum body. Confirm the insert design and service condition before reuse.
What details are needed for a matching quote?
Body diameter, bore, cutting height, insert arrangement, rotation and the edge-bander model, plus a current-tool photo or dimensioned drawing where available.
Is the body reusable after insert replacement?
The hardened aluminum body is retained; insert seats are checked during service. Include photos of the body and seats so condition can be assessed.
Can non-standard body sizes be made?
Yes. Custom body diameters, bores and insert arrangements are produced after the machine details are confirmed.
Key words: aluminum PCD pre-milling cutter, insert cutter head, edge banding pre-milling, detachable PCD inserts, PCD premill cutter, pre-milling cutter head, edge banding premill, PCD edge banding cutter, premilling router bit, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, spoilboard surfacing ROI, nested-based manufacturing, furniture manufacturing, furniture factory, cabinet making, panel furniture, kitchen cabinet production, woodworking machinery, CNC router, woodworking cutting tools, acrylic sheet, solid wood, particleboard, chipboard, plywood, rubber sheet, rubber board, hardwood, softwood, MDF, HDF, flycutter, planing bit, surfacing bit, slab flattening bit, bottom cleaning bit, spoilboard leveller, rabbeting bit
What spindle speed and feed should I set for premilling MDF?
+Start near 20,000–24,000 rpm spindle speed with the edge bander feed around 12–18 m/min, then fine-tune so the premill removes the saw overhang and old glue line in one clean pass.
Why PCD instead of brazed tungsten carbide for premilling?
+On abrasive MDF and particleboard, PCD edges last 10–20 times longer (typical industry data cited in our comparison table above), so the bander runs far longer between tool changes.
How often should the premill knives be rotated or replaced?
+Rotate the reversible inserts at the first sign of glue-line fuzzing; each edge has several usable sections, so a fresh edge takes seconds on the machine.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification
Related Search Terms
PCD router bit, PCD spiral router bit, diamond router bit, PCD tips, diamond compression end mill, PCD shank cutter, PCD helicoidal cutter, PCD vs brazed tungsten carbide, diamond cutting tool for MDF, PCD tooling for chipboard, polycrystalline diamond router bit, aluminum, milling, cutter