- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling

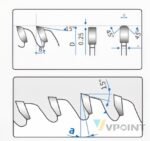


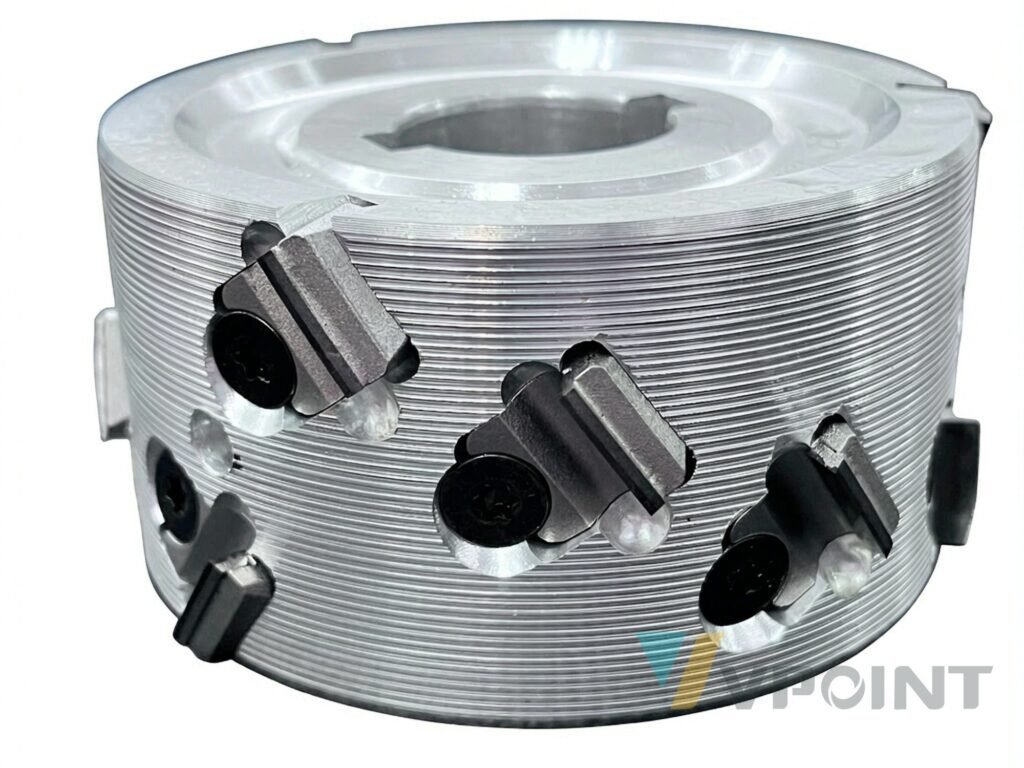
Design and Construction — a VPOINT router bit tool for CNC routing and nesting, sized for MDF and similar workpieces. The specification table below lists dimensions; the performance data table gives standard reference speeds and feeds to start with, and the FAQ covers selection, parameters and service. ISO 9001 production, batch-verified, custom sizes from drawings.
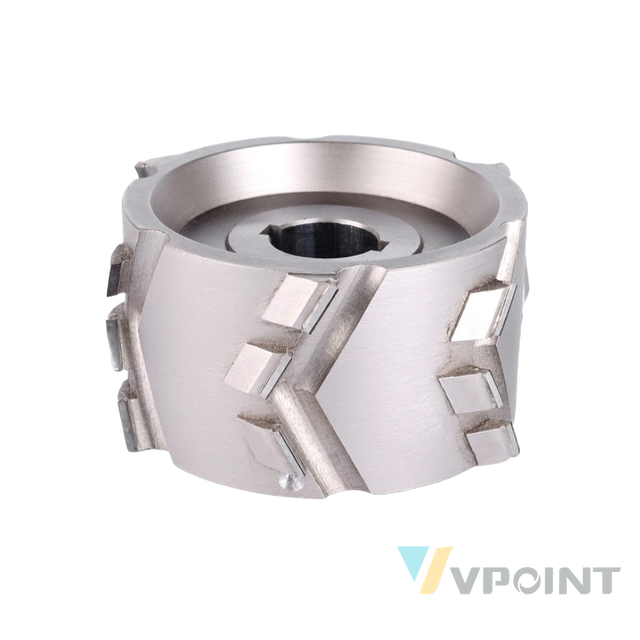
The VP118626 diamond lamello slotting knife cuts biscuit-joinery slots, with 100.4 mm diameter blades on 22 or 30 mm bores and 7 mm cutting width in three- and six-tooth versions. PCD tips hold the slot width in abrasive-faced panels across long production runs.
Design and Construction
The VP118626 diamond lamello slotting knife is a PCD-tipped cutter for Lamello (biscuit) joinery slots. The 100.4 mm diameter blades run 22 or 30 mm bores with 7 mm cutting width in 3-tooth and 6-tooth versions, plus an 80 mm / 16 mm-bore variant and a 3 mm-width 16-tooth version. Two small 12.7 mm tools with 9.4 mm shanks (H22) cover router-based slot cutting.


How It Works
The cutter plunges or feeds to cut the flat biscuit slot: PCD teeth hold the slot width and depth in abrasive boards, so biscuits seat with consistent fit. The multi-tooth versions spread the cutting load for smoother slot walls.
Applications
- Lamello / biscuit joinery slot cutting
- Slot cutting on panel furniture lines
- Router-based slot cutting (12.7 mm shank tools)
- MDF and plywood joinery slots
Suitable Materials
- Melamine-faced particleboard
- MDF
- Veneered plywood
- Solid wood

The PCD edge keeps slot width and depth constant in abrasive boards, holding biscuit fit across long runs.
Material Comparison: PCD vs. Tungsten Carbide
The figures below are typical industry data for production woodworking. PCD does not replace carbide in every job — carbide remains the right choice for low-volume general work — but on abrasive sheet goods the difference in blade life is decisive.
| Property | PCD Diamond (This Blade) | Tungsten Carbide |
|---|---|---|
| Hardness | 7,000–9,000 HV | 1,500–2,000 HV |
| Tool life on MDF / particleboard / melamine | 15–20× longer (500–1,200 h) | 30–60 h (baseline) |
| Tool life on solid hardwood | 10–13× longer (800–2,000 h) | 80–150 h (baseline) |
| Tool life on abrasive boards (fibre cement / composites) | 10–15× longer | baseline |
| Edge renewal | Limited regrinds — the economics come from 15–20× longer intervals between changes, not regrind count | 4–6 regrinds at shorter intervals |
| Cut finish | Ra ≤ 0.2 μm achievable, stable over the blade life | Ra ~0.8 μm typical, degrades as teeth wear |
| Thermal conductivity | 540–560 W/m·K — heat leaves the tooth tip fast | ~80 W/m·K |
| Friction coefficient | ≈ 0.05 — lower cutting forces and heat | ≈ 0.3 |
| Suited for | Abrasive engineered wood, laminates, composites, fibre cement, non-ferrous metals | General-purpose solid-wood work; the economic choice at lower volumes |
Figures are typical published values; actual blade life depends on the workpiece material, feed rate, depth of cut, machine condition and maintenance schedule.
Delivery Scope
Single cutter. Order by part number with the diameter, bore, width and tooth count stated in the specifications table below.
Why Choose VPOINT
- One-year warranty on every blade — defects in material or workmanship are covered for 12 months from delivery.
- Custom tooling — diameters, kerfs, bores and tooth counts built to your drawing or sample.
- Non-standard fabrication — sizes outside the standard catalogue, including bore re-sizing and tooth-count changes.
- Resharpening service — blades return to service after regrinding at a fraction of new-blade cost.
- Factory-direct since 2008 — ISO 9001 manufacturing in Sichuan and Dongguan, China; 40Cr chrome-molybdenum steel bodies; no trading intermediaries.
Send a drawing, a sample or a worn blade, and our engineering team will quote the exact specification you need.
Precision & Quality Control
Every blade is inspected before shipment. Outside diameter, kerf thickness, plate thickness, bore diameter and tooth count are measured against the values listed in the specifications table, and tooth geometry (hook angle, bevel angle) is verified against the design drawing. Blades are stress-checked for runout and tension before packing.
Blades measuring outside tolerance do not ship. Inspection is performed under our ISO 9001 quality system, with batch records retained for traceability.
Specifications
| Part No. | SIZE mm | ØD | Ød | B | Z |
|---|---|---|---|---|---|
| VP118626 | D100.4*d22*H7*Z3 | 100.4 | 22 | 7 | 3 |
| VP118626 Z6 | D100.4*d22″H7*Z6 | 100.4 | 22 | 7 | 6 |
| VP118626 d30 | D100.4*d30*H7*Z6 | 100.4 | 30 | 7 | 6 |
| VP118626 D80 | D80*d16*H7*Z6 | 80 | 16 | 7 | 6 |
| VP118626-2T | D12.7*d9.4*H22*Z2 | 12.7 | 9.4 | 55 | 5 |
| VP118626-3T | D12.7*d9.4*H22*Z3 | 12.7 | 9.4 | 55 | 6 |
| VP118626-B3 | D100.4*d22*H3*Z16 | 100.4 | 22 | 3 | 16 |
Performance Data
Standard reference values for guidance only — always adjust to the edge bander feed, machine condition and tool wear, and confirm on the actual panel.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| MDF | 20,000–24,000 rpm | 12–18 m/min | PCD premill heads hold edge on abrasive MDF |
| particleboard | 18,000–22,000 rpm | 12–18 m/min | Grit-resistant diamond edges for long runs |
| plywood / veneered panels | 18,000–22,000 rpm | 12–16 m/min | Clean glue-line removal before banding |
| veneered composite panels | 18,000–20,000 rpm | 10–14 m/min | Two-stage 2+2 / 3+3 geometry |
| solid wood edge bands | 16,000–20,000 rpm | 10–14 m/min | Adjust per feed of the edge bander |
Frequently Asked Questions
What is the Diamond Lamello Slotting Knife used for?
The VP118626 diamond lamello slotting knife is a PCD-tipped cutter for Lamello (biscuit) joinery slots.
How do I choose the right size?
Refer to the specification table on this page: part numbers fix the cutting diameter, shank and cutting length. State the diameter, shank and cutting length you need when ordering.
Which materials does it suit?
Typical materials include Melamine-faced particleboard, MDF, Veneered plywood. Confirm the material grade and machining conditions for the specific tool before ordering.
Can I order a custom version?
Yes. Send the profile drawing or item code together with the workpiece material, machine model, cutting direction and quantity. Tools are produced to order, and each tool is packed in an individual plastic box.
Key words: lamello slotting knife, biscuit joinery cutter, diamond slot cutter, PCD slotting knife, PCD premill cutter, pre-milling cutter head, edge banding premill, PCD edge banding cutter, premilling router bit, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, spoilboard surfacing ROI, nested-based manufacturing, furniture manufacturing, furniture factory, cabinet making, panel furniture, kitchen cabinet production, woodworking machinery, CNC router, woodworking cutting tools
What spindle speed and feed should I set for premilling MDF?
+Start near 20,000–24,000 rpm spindle speed with the edge bander feed around 12–18 m/min, then fine-tune so the premill removes the saw overhang and old glue line in one clean pass.
Why PCD instead of brazed tungsten carbide for premilling?
+On abrasive MDF and particleboard, PCD edges last 10–20 times longer (typical industry data cited in our comparison table above), so the bander runs far longer between tool changes.
How often should the premill knives be rotated or replaced?
+Rotate the reversible inserts at the first sign of glue-line fuzzing; each edge has several usable sections, so a fresh edge takes seconds on the machine.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification