
- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
Acrylic Wood Single Blade Spiral Milling Cutter

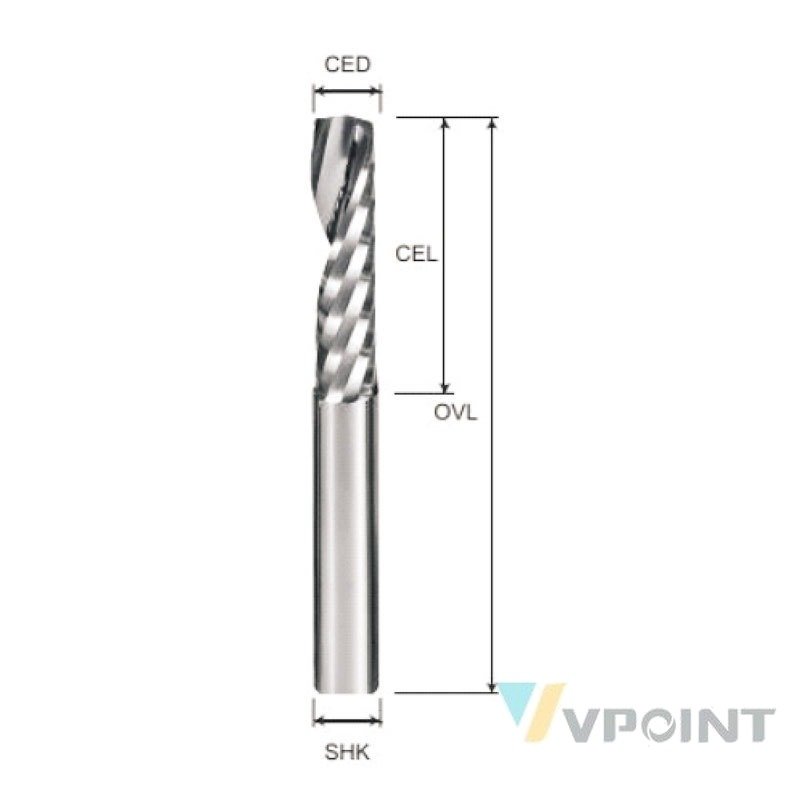
Design and Construction — a VPOINT end mill tool for CNC milling, sized for MDF and similar workpieces. The specification table below lists dimensions; the performance data table gives standard reference speeds and feeds to start with, and the FAQ covers selection, parameters and service. ISO 9001 production, batch-verified, custom sizes from drawings.
Design and Construction
The acrylic/wood single-blade spiral milling cutter carries a single spiral flute on a tungsten carbide body. Shank diameters (SHK) run 3.175–12 mm, cutting-edge diameters (CED) 1–12 mm, cutting edge lengths (CEL) 4–62 mm and overall lengths (OVL) 38–120 mm, as listed in the specifications table.
How It Works
A single spiral flute gives the chip maximum evacuation space: the edge shears acrylic cleanly and the spiral lifts chips out of the slot, keeping the cut wall clear and cool. This is the geometry for crisp edges in acrylic and clean grooves in wood on CNC routers.
Applications
- Acrylic cutting and engraving on CNC routers
- Wood grooving and slotting
- Sign and display fabrication
- Clean-edge profile cutting
Suitable Materials
- Acrylic (PMMA)
- Solid wood
- MDF and plywood
- Plastic sheet
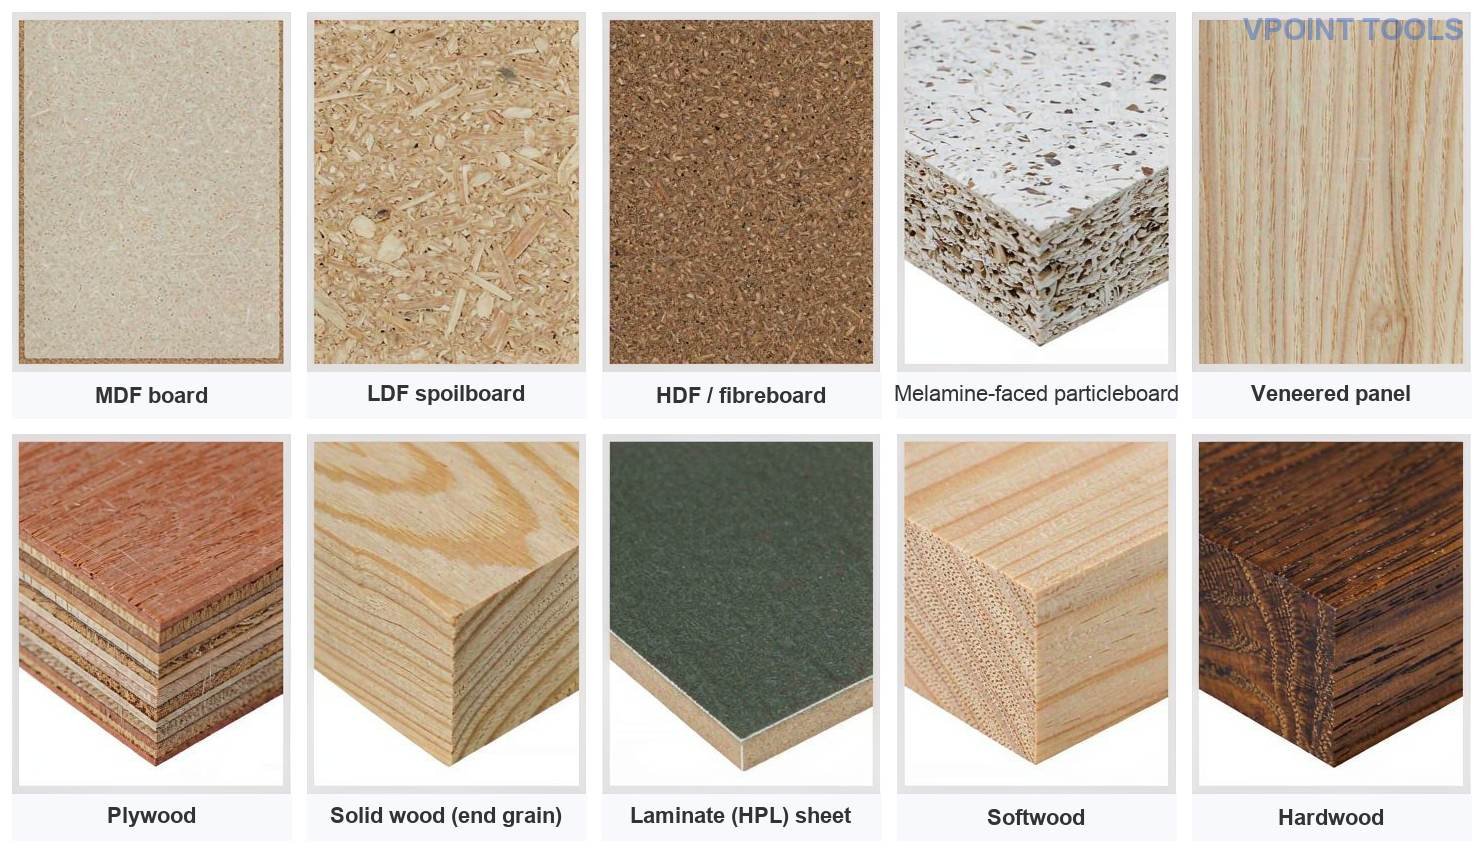
The single spiral flute keeps chips out of the cut, holding edge clarity in acrylic and clean walls in wood.
Material Comparison: Tungsten Carbide vs. PCD
The figures below are typical industry data for CNC tooling. Tungsten carbide is the economic standard for general CNC routing — tough, regrindable and available in every geometry. PCD wins on very high-volume abrasive work; this page covers the carbide line, and the comparison shows where each material wins so you can match the tool to the job.
| Property | Tungsten Carbide (This Tool) | PCD Diamond |
|---|---|---|
| Hardness | 1,500–2,000 HV | 7,000–9,000 HV |
| Tool life on MDF / particleboard / melamine | 30–60 h (baseline) | 15–20× longer (500–1,200 h) |
| Tool life on solid hardwood | 80–150 h (baseline) | 10–13× longer (800–2,000 h) |
| Edge renewal | 4–6 regrinds at shorter intervals | 5–8 regrinds, each removing only 0.2–0.3 mm of diamond |
| Surface finish | Ra ~0.8 μm typical, degrades as the edge wears | Ra ≤ 0.2 μm achievable, stable over the tool life |
| Thermal conductivity | ~80 W/m·K | 540–560 W/m·K — heat leaves the edge fast |
| Friction coefficient | ≈ 0.3 | ≈ 0.05 — lower cutting forces |
| Fracture toughness | Higher — tolerates interrupted cuts and impacts better | Lower — needs stable, vibration-free setups |
| Suited for | General-purpose CNC routing in wood, panels, acrylic; the economic standard | Very high-volume abrasive panel work; non-ferrous metals |
Figures are typical published values; actual tool life depends on the workpiece material, feed rate, depth of cut, machine condition and maintenance schedule.
Delivery Scope
Single cutter. Order by part number with the shank, cutting-edge diameter and cutting length stated in the specifications table below.
Why Choose VPOINT
- One-year warranty on every cutter — defects in material or workmanship are covered for 12 months from delivery.
- Custom tooling — diameters, shanks, cutting lengths and flute configurations built to your drawing or sample.
- Non-standard fabrication — sizes outside the standard catalogue, including special geometries.
- Resharpening service — cutters return to service after regrinding at a fraction of new-tool cost.
- Factory-direct since 2008 — ISO 9001 manufacturing in Sichuan and Dongguan, China; no trading intermediaries.
Send a drawing, a sample or a worn tool, and our engineering team will quote the exact specification you need.
Precision & Quality Control
Every cutter is inspected before shipment. Shank diameter, cutting-edge diameter, cutting length and overall length are measured against the values listed in the specifications table, and cutting edge runout is verified on the assembled tool.
Tools measuring outside tolerance do not ship. Inspection is performed under our ISO 9001 quality system, with batch records retained for traceability.
Specifications
| Part NO. | SHK | CED | CEL | OVL |
|---|---|---|---|---|
| 10060104 | 3.175 | 1 | 4 | 38 |
| 10061507 | 3.175 | 1.5 | 7 | 38 |
| 10061512 | 3.175 | 1.5 | 12 | 38 |
| 10060208 | 3.175 | 2 | 8 | 38 |
| 10060212 | 3.175 | 2 | 12 | 38 |
| 10060215 | 3.175 | 2 | 15 | 38 |
| 10060217 | 3.175 | 2 | 17 | 38 |
| 10060222 | 3.175 | 2 | 22 | 45 |
| 10062508 | 3.175 | 2.5 | 8 | 38 |
| 10062512 | 3.175 | 2.5 | 12 | 38 |
| 10062515 | 3.175 | 2.5 | 15 | 38 |
| 10062517 | 3.175 | 2.5 | 17 | 38 |
| 10062522 | 3.175 | 2.5 | 22 | 45 |
| 10063112 | 3.175 | 3.175 | 12 | 38 |
| 10063115 | 3.175 | 3.175 | 15 | 38 |
| 10063117 | 3.175 | 3.175 | 17 | 38 |
| 10063122 | 3.175 | 3.175 | 22 | 45 |
| 10063125 | 3.175 | 3.175 | 25 | 50 |
| 10063132 | 3.175 | 3.175 | 32 | 55 |
| 10063142 | 3.175 | 3.175 | 42 | 70 |
| 10063152 | 3.175 | 3.175 | 52 | 75 |
| 10060415 | 4 | 4 | 15 | 45 |
| 10060422 | 4 | 4 | 22 | 45 |
| 10060425 | 4 | 4 | 25 | 50 |
| 10060428 | 4 | 4 | 28 | 50 |
| 10060432 | 4 | 4 | 32 | 55 |
| 10060442 | 4 | 4 | 42 | 70 |
| 10060452 | 4 | 4 | 52 | 75 |
| 10060525 | 5 | 5 | 25 | 50 |
| 10060528 | 5 | 5 | 28 | 55 |
| 10060532 | 5 | 5 | 32 | 60 |
| 10060625 | 6 | 6 | 25 | 50 |
| 10060628 | 6 | 6 | 28 | 60 |
| 10060632 | 6 | 6 | 32 | 60 |
| 10060642 | 6 | 6 | 42 | 75 |
| 10060652 | 6 | 6 | 52 | 85 |
| 10060662 | 6 | 6 | 62 | 100 |
| 10060825 | 8 | 8 | 25 | 60 |
| 10060832 | 8 | 8 | 32 | 60 |
| 10060842 | 8 | 8 | 42 | 75 |
| 10060852 | 8 | 8 | 52 | 85 |
| 10060862 | 8 | 8 | 62 | 100 |
| 10061032 | 10 | 10 | 32 | 75 |
| 10061042 | 10 | 10 | 42 | 85 |
| 10061052 | 10 | 10 | 52 | 100 |
| 10061062 | 10 | 10 | 62 | 120 |
| 10061232 | 12 | 12 | 32 | 75 |
| 10061242 | 12 | 12 | 42 | 85 |
| 10061252 | 12 | 12 | 52 | 100 |
| 10061262 | 12 | 12 | 62 | 120 |
Key words: single flute spiral bit, acrylic router bit, acrylic cutting cutter, CNC acrylic end mill, solid carbide end mill, CNC end mill, compression router bit, upcut spiral bit, downcut spiral bit, single flute end mill, two flute end mill, spiral flutes end mill, slotting end mill, profiling end mill, steel slotting cutter, aluminium end mill, acrylic end mill, nano coating end mill, corn milling cutter, edge rounding cutter, flat bottom end mill, ball nose end mill, furniture manufacturing, furniture factory, cabinet making, acrylic sheet, solid wood, particleboard, chipboard, plywood, rubber sheet, rubber board, hardwood, softwood, MDF, HDF, melamine board, laminated board, flycutter, planing bit, surfacing bit, slab flattening bit, bottom cleaning bit, spoilboard leveller, rabbeting bit
Performance Data
Standard reference values for guidance only — always adjust to machine rigidity, clamping and tool wear, and confirm on the actual workpiece.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| MDF | 18,000–22,000 rpm | 6–10 m/min | Nesting and grooving; watch heat at small diameters |
| particleboard | 16,000–20,000 rpm | 5–8 m/min | Reduce feed if the face starts to chip |
| plywood | 16,000–20,000 rpm | 5–8 m/min | Keep the compression or shear geometry inside the panel |
| veneered board | 18,000–20,000 rpm | 5–7 m/min | Light finish passes protect the veneer |
| acrylic | 18,000–22,000 rpm | 4–8 m/min | Polish passes at reduced feed for clear edges |
| solid wood | 15,000–20,000 rpm | 4–9 m/min | Grain direction affects finish; climb-cut when possible |
Frequently Asked Questions
What spindle speed suits MDF?
Begin near 18,000–22,000 rpm with the feed around 6–10 m/min, then tune by chip load and finish. Rubbing means raise the feed; burning means drop it.
Up-cut or down-cut for this job?
Up-cut pulls chips up and away but can fuzz the top face; down-cut presses the top face down. Match the flute direction to the face you care about.
How deep can I cut in one pass?
Stay within the cutting length and keep passes inside the listed geometry; deeper single passes raise deflection and heat.
Where do these reference values come from?
They are standard reference ranges for this tool family, compiled from our specification sheets and common workshop practice — always confirm on the actual workpiece.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification
Related Search Terms
solid carbide end mill, CNC end mill, compression router bit, upcut spiral bit, downcut spiral bit, single flute end mill, two flute end mill, spiral flutes end mill, slotting end mill, profiling end mill, steel slotting cutter, aluminium end mill, acrylic end mill, nano coating end mill, corn milling cutter

Reviews
There are no reviews yet.