- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling


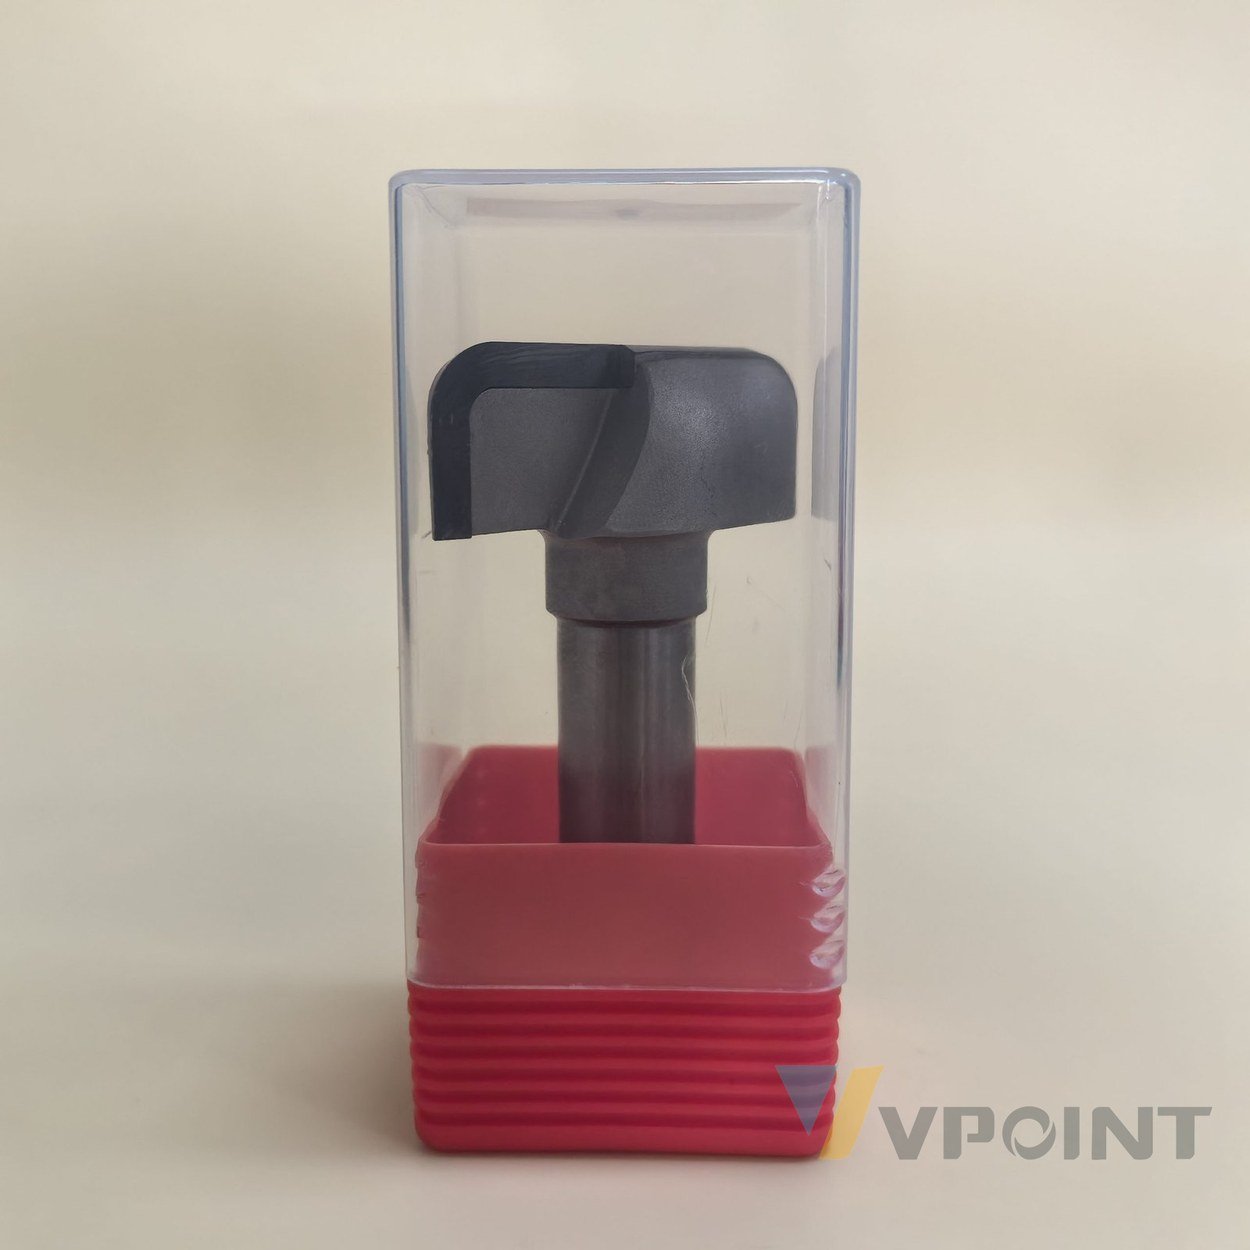
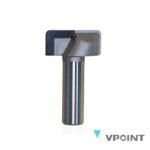
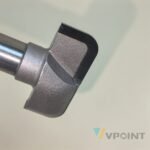
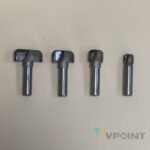
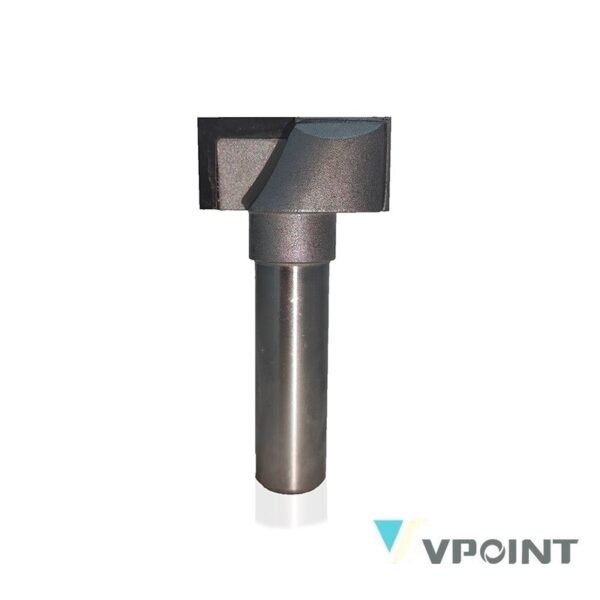

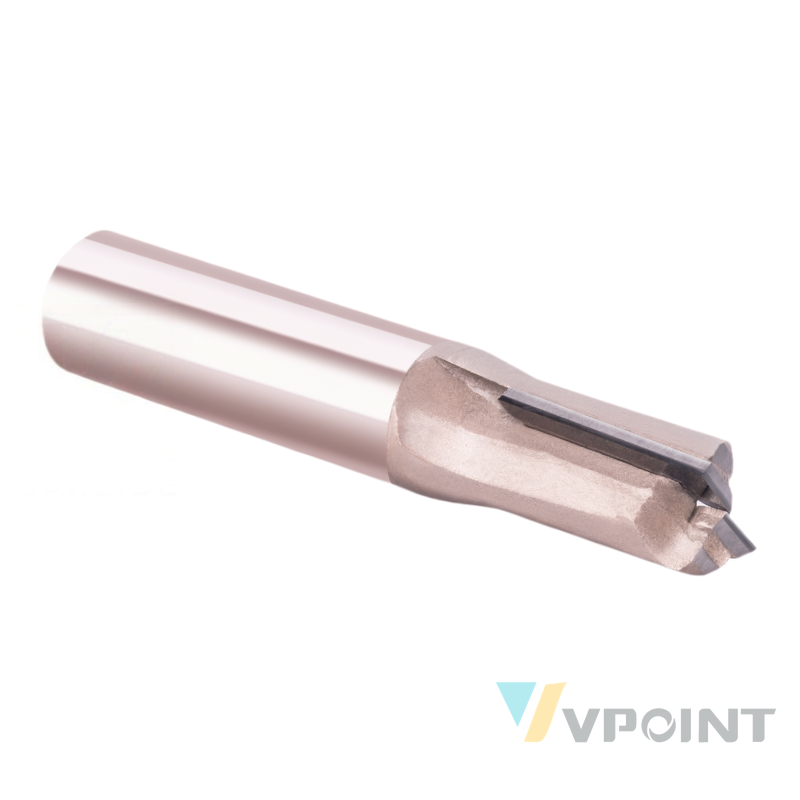
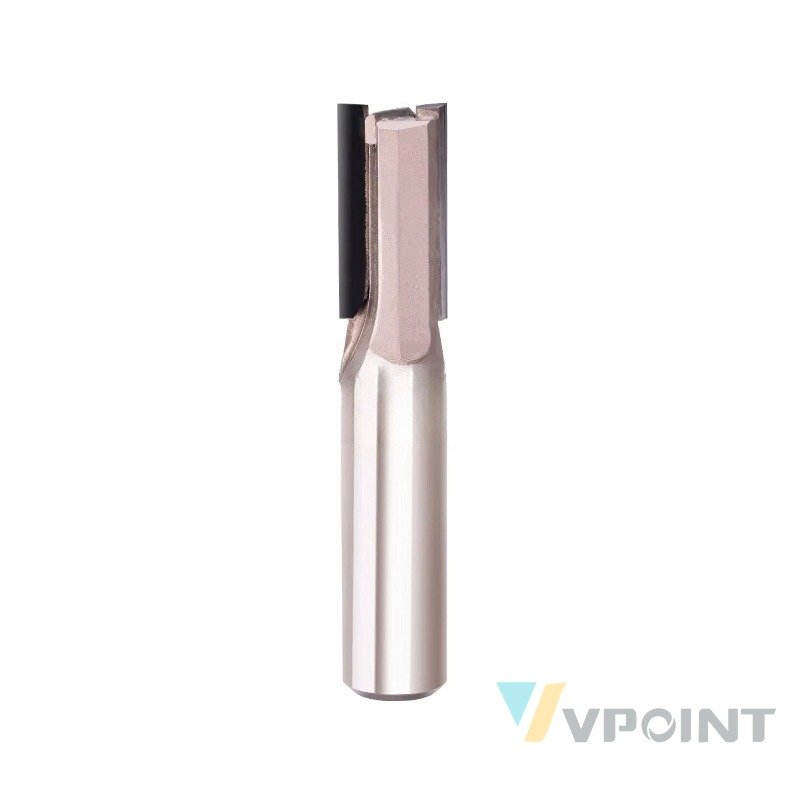
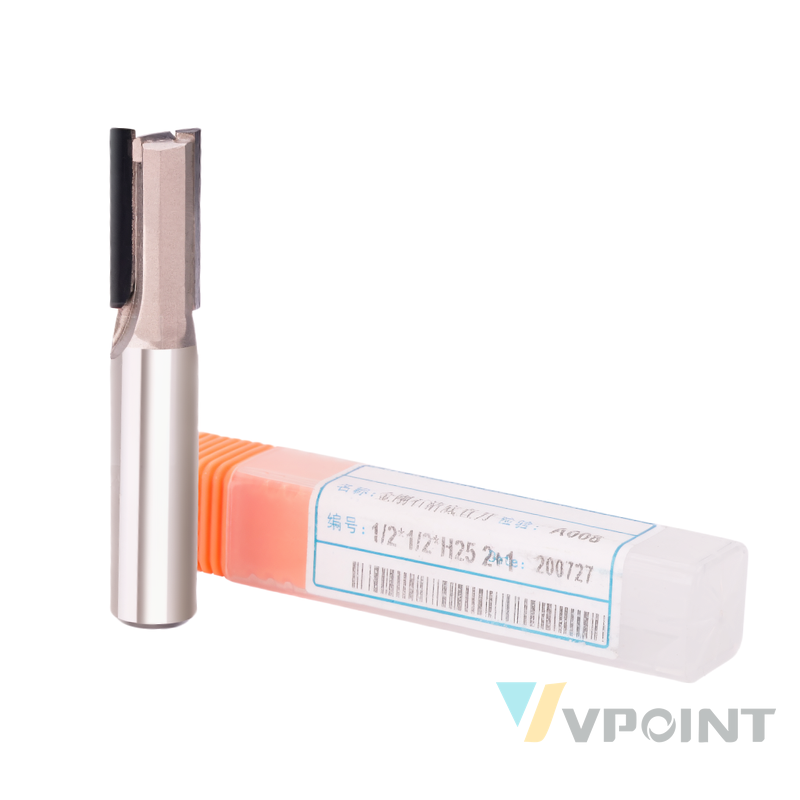
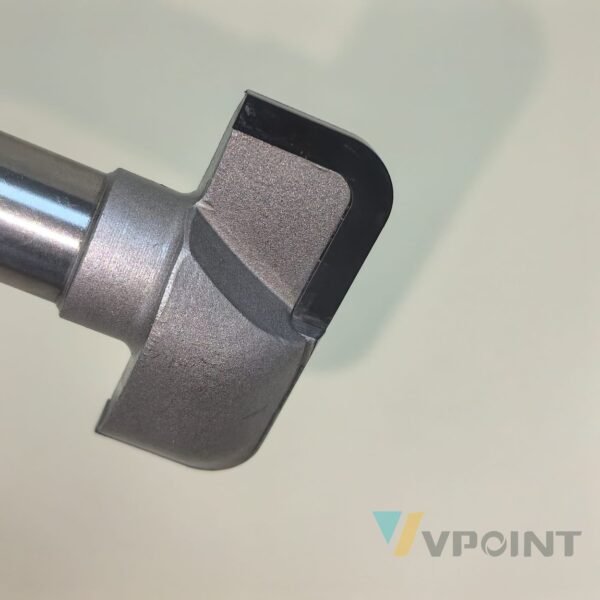
PCD Bowl & Tray Bits for CNC Woodworking — a VPOINT PCD straight router bit for flat-bottom grooving and spoilboard work, sized for MDF and similar workpieces. Start near 20,000–24,000 rpm / 10–15 m/min (standard reference values in the performance table below); the specification table lists diameters, cut lengths and shanks. Diamond edges hold 15–20× carbide life on abrasive panels. ISO 9001 production, batch-verified, custom sizes from drawings.
PCD Bowl & Tray Bits for CNC Woodworking
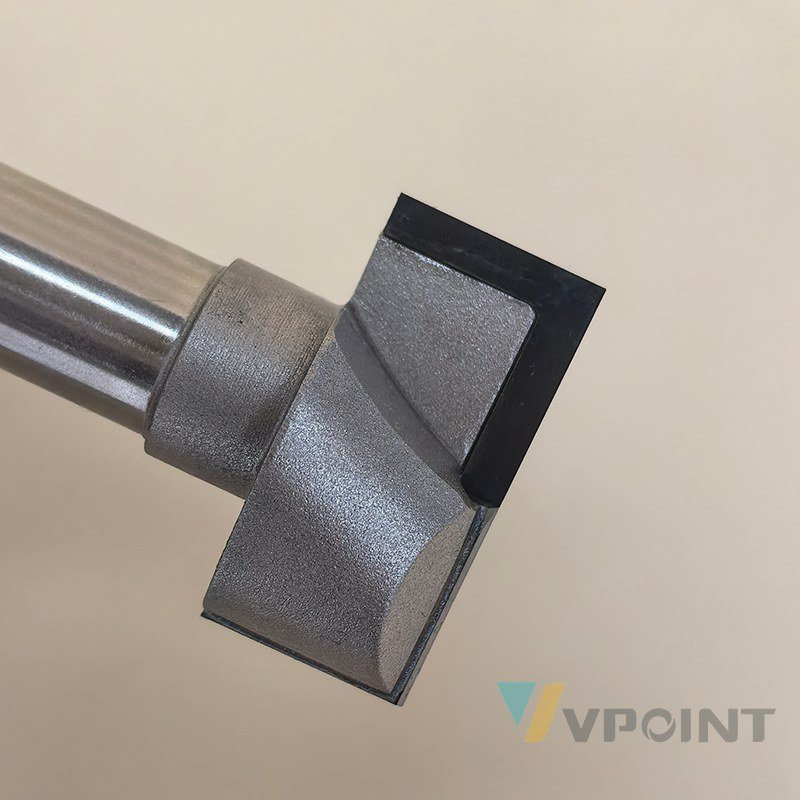
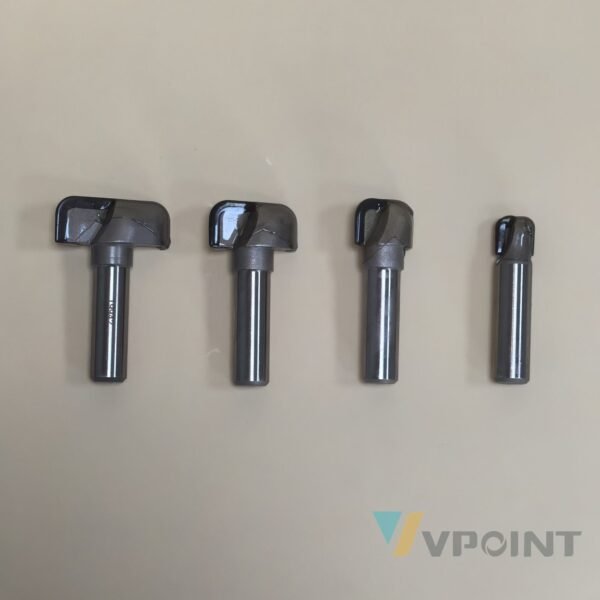
PCD bowl & tray bits machine bowl and tray recesses, container profiles, lettering and sign work on compatible CNC woodworking machines. Thirteen configurations cover cutting diameters from 12.7 to 47.68 mm with corner radii from 1.59 to 15.9 mm, in 12.7 mm and 6.35 mm shanks.
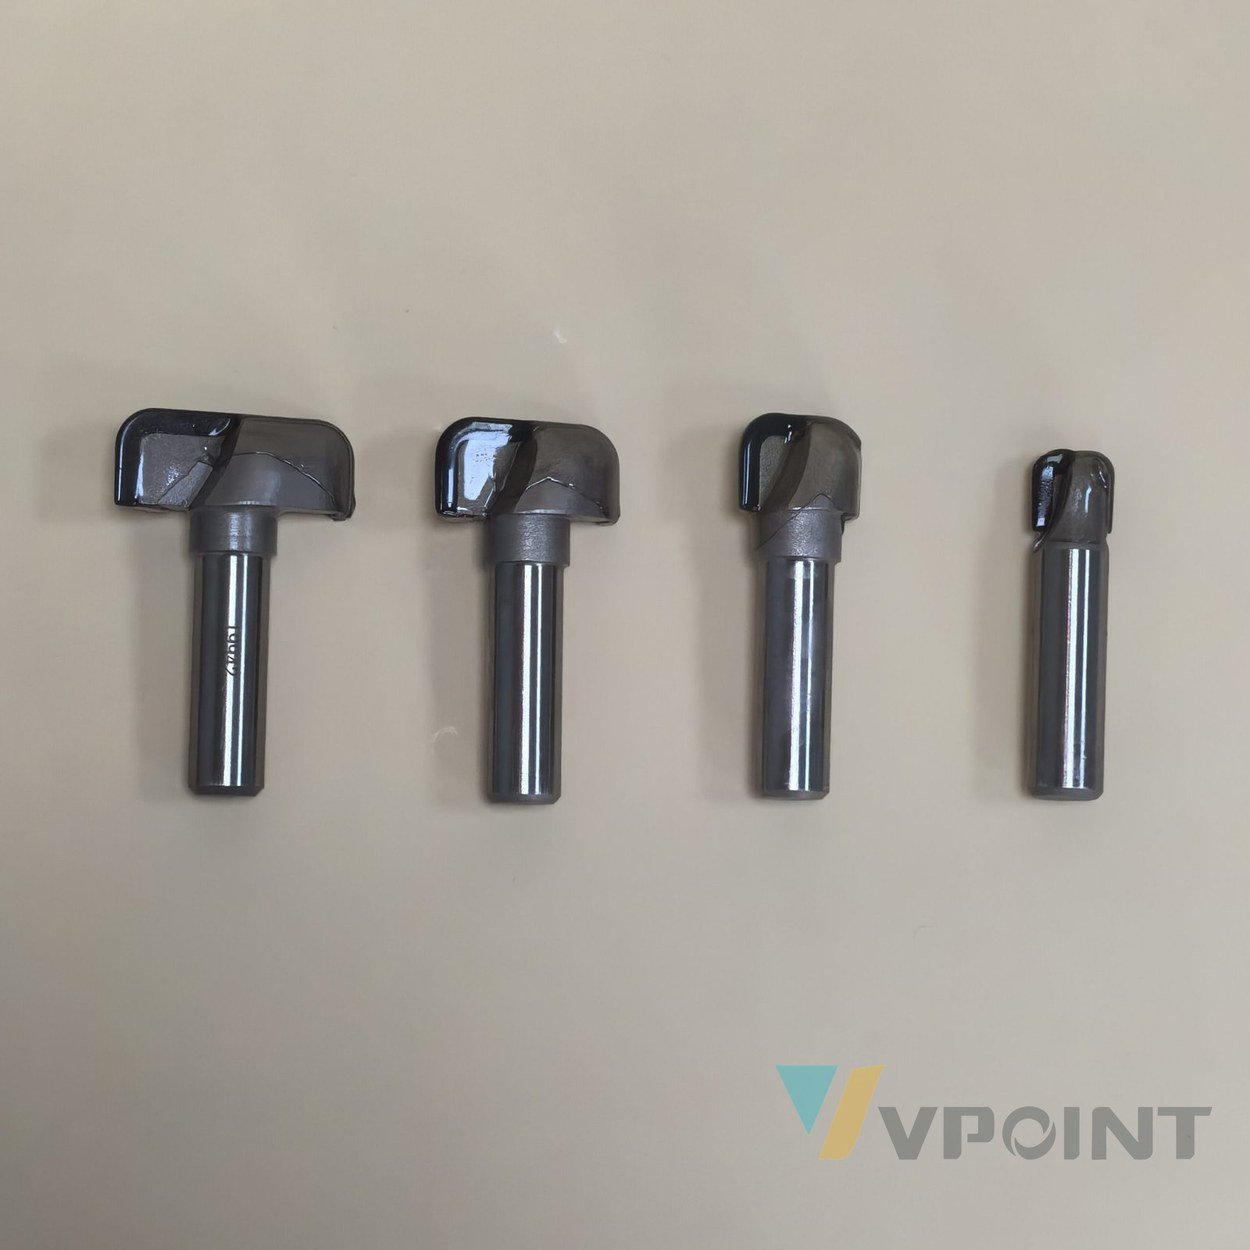
Design and Construction
+The cutting edge is polycrystalline diamond (PCD) brazed onto a 40Cr chrome-molybdenum steel body with a round-nose bowl profile. The radius R sets the corner curvature of the recess, and the cutting diameter D sets the sweep of each pass. The series is produced in the Sichuan and Dongguan, China manufacturing bases.
How It Works
+The bit is plunged into the workpiece and traced along the recess path; the round-nose profile shears a smooth round-bottomed channel whose corner radius follows the tool radius. Overlapping passes widen the recess to the tray outline, and depth of cut sets the recess depth. Send the required bottom shape, corner radius, recess depth and workpiece thickness so the profile is matched to the job.
Applications
- Bowl and tray recesses
- Container profiles
- Lettering and sign work
- For compatible CNC woodworking machines, engraving machines and routing machines
Suitable Materials
- MDF, chipboard and calcium board, subject to grade and application review
- Suitability depends on the specific material grade, profile and machining conditions; confirm the application before ordering
Material Comparison: Traditional Brazed Tungsten Carbide vs. Diamond (PCD) Router Bit
+Typical industry data for reference. Actual results depend on the workpiece grade, machine condition and feed rate.
| Property | Traditional Brazed Tungsten Carbide Router Bit | Diamond (PCD) Router Bit |
|---|---|---|
| Cutting material hardness | 1,500–2,000 HV | 7,000–9,000 HV |
| Edge life on MDF / particleboard | Baseline (1×) | 15–20× longer edge life |
| Edge life on solid wood | Baseline (1×) | 10–13× longer edge life |
| Edge life on acrylic | Baseline (1×) | 10–15× longer edge life |
| Regrinding / refurbishing cycles | 2–4 times | 5–8 times |
| Cut edge quality | Ra 0.4–0.8 µm, more fuzzing | Ra 0.2–0.4 µm, cleaner edge |
| Thermal conductivity | ≈ 100 W/m·K | ≈ 500 W/m·K, heat cleared faster |
| Friction coefficient | ≈ 0.3 | ≈ 0.05–0.1, lower cutting force |
| Chipping risk on brittle panels | Higher at high feed | Lower, stable edge at high feed |
| Cost per metre of cutting | Higher over long runs | Lower over long runs |
Delivery Scope
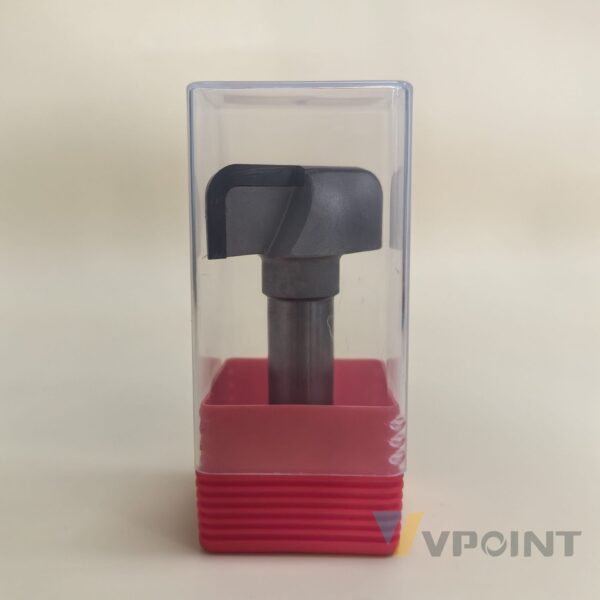
Each tool is packed in an individual plastic box.
+Each order also includes an inspection record. Custom configurations are produced after the workpiece material, machine model and required dimensions are confirmed.
Why Choose VPOINT
+VPOINT supports this series with:
- One-year warranty on every router bit
- Custom and non-standard diameters, cutting heights and shanks produced to order
- Regrinding service to extend tool life
- Factory direct since 2008, ISO 9001 certified
- Dual manufacturing bases in Sichuan and Dongguan, China
Precision & Quality Control
+Every bowl & tray bit is inspected before shipment: cutting diameter, shank diameter, cutting height and tool runout are checked against the specification table at micron level. Production follows an ISO 9001 process with batch traceability, so reorders match the original configuration.
Specifications
The table below is transcribed from the original product chart. D denotes cutting diameter, H cutting height, R radius and d shank diameter. The source chart contains inconsistent overall-length and tooth-count entries; confirm these fields and the final configuration before ordering. Each row is a separate configuration.
| Item code | D (mm) | H (mm) | R (mm) | d (mm) |
|---|---|---|---|---|
| LH09001 | 12.7 | 6.09 | 1.59 | 12.7 |
| LH09002 | 14.29 | 6.88 | 2.38 | 12.7 |
| LH09003 | 15.88 | 8.18 | 3.18 | 12.7 |
| LH09004 | 20.64 | 8 | 3.97 | 12.7 |
| LH09005 | 22.22 | 9.26 | 4.76 | 12.7 |
| LH09006 | 25.4 | 10.85 | 6.35 | 12.7 |
| LH09007 | 28.62 | 12.46 | 7.96 | 12.7 |
| LH09008 | 31.75 | 14.52 | 9.52 | 12.7 |
| LH09009 | 34.9 | 17.2 | 11.11 | 12.7 |
| LH09010 | 38.1 | 18 | 12.7 | 12.7 |
| LH09011 | 44.46 | 20 | 14.29 | 12.7 |
| LH09012 | 47.68 | 22 | 15.9 | 12.7 |
| LH09013 | 12.7 | 6.09 | 1.59 | 6.35 |
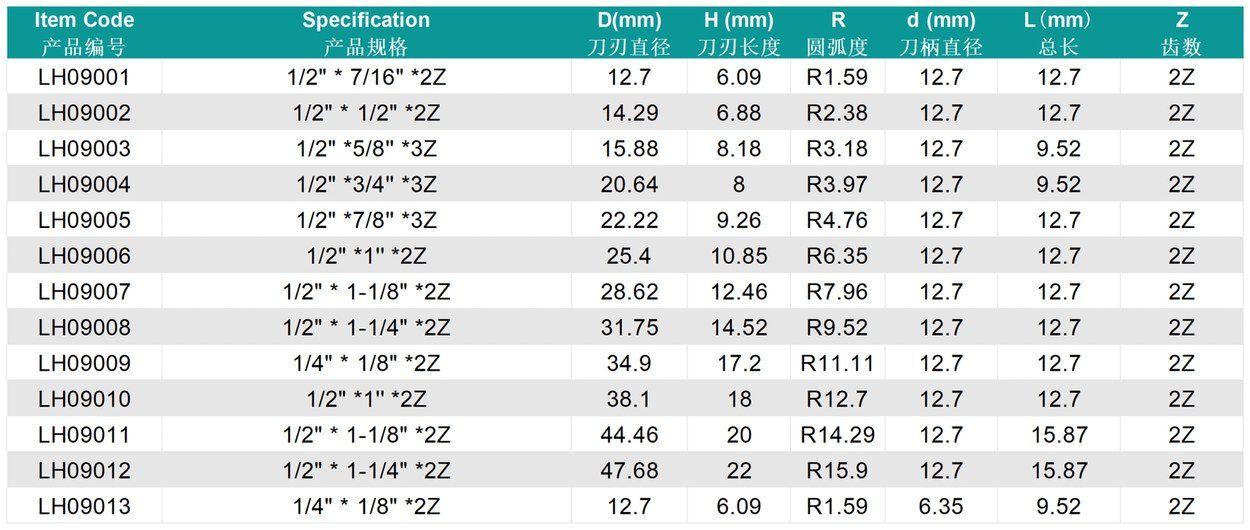
Original specification chart with 13 configurations

Bowl profile with D, H and R dimensions
Performance Data
Standard reference values for guidance only — always adjust to machine rigidity, clamping and tool wear, and confirm on the actual workpiece.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| MDF | 20,000–24,000 rpm | 10–15 m/min | PCD holds edge on abrasive MDF |
| particleboard | 18,000–22,000 rpm | 8–12 m/min | Grit-resistant diamond edges |
Frequently Asked Questions
Which diameters and radii are available?
+Thirteen configurations with cutting diameters from 12.7 to 47.68 mm and radii from 1.59 to 15.9 mm. Twelve rows use a 12.7 mm shank and row LH09013 uses a 6.35 mm shank.
How do I match the bit to my tray design?
+Send the required bottom shape, corner radius, recess depth and workpiece thickness. The radius R sets the corner curvature of the recess, so it must match the drawing.
Can it cut calcium board?
+Calcium board is listed for this product subject to grade and application review. Provide the exact board composition, grade and thickness so suitability is confirmed before production.
What should I send for a custom request?
+The item code or required profile drawing, tool dimensions, workpiece material, machine model, cutting direction and quantity, plus a reference photo or current-tool drawing where available.
+Key words: PCD bowl tray bit, round nose router bit, CNC tray recess bit, diamond bowl router bit, PCD straight router bit, diamond straight bit, PCD slotting cutter, PCD groove cutter, diamond tipped router bit, PCD router bit, PCD spiral router bit, diamond router bit, PCD tips, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, furniture manufacturing, furniture factory, cabinet making, panel furniture, kitchen cabinet production
What feed should I start with on MDF?
+Begin near 10–15 m/min at 20,000–24,000 rpm. Straight PCD flutes cut without lifting the panel, so a steady moderate feed gives the cleanest flat bottom; tune by chip load.
Why choose PCD for straight-flute work?
+On abrasive MDF and particleboard the diamond edges last 15–20 times longer than brazed carbide (typical industry data), keeping the groove width constant across long runs.
Are these bits suitable for spoilboard surfacing?
+Yes — the bottom-cleaning versions level MDF and LDF beds evenly. Multiple passes with light overlap give the flattest table.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification