- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling



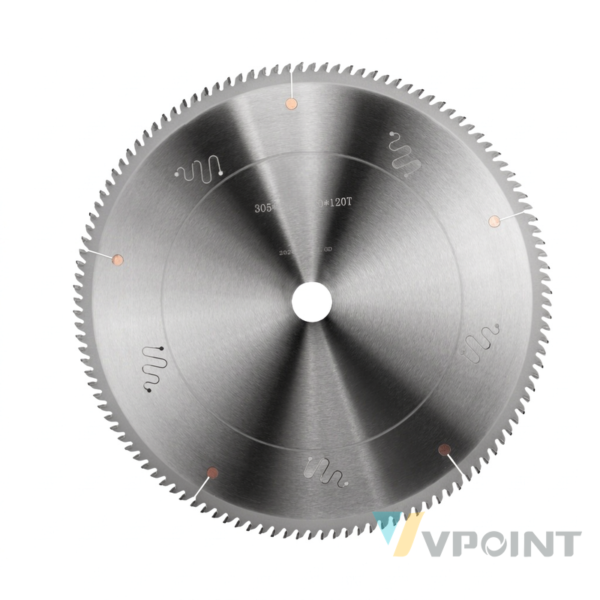
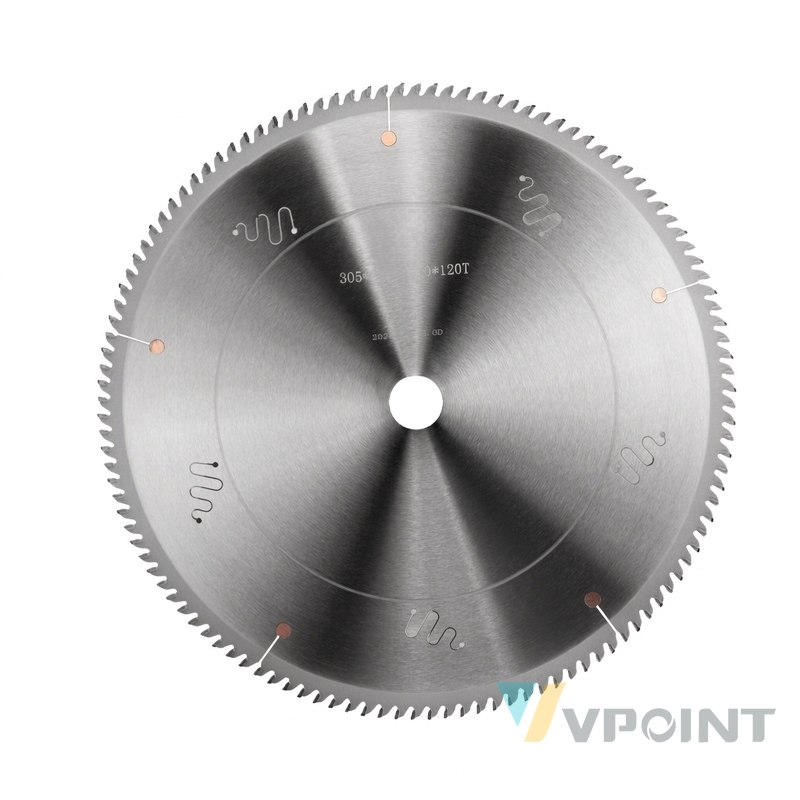
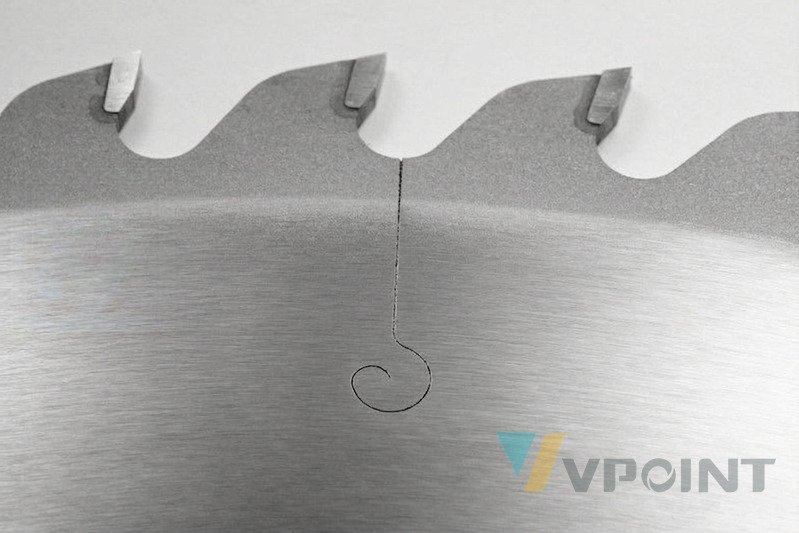
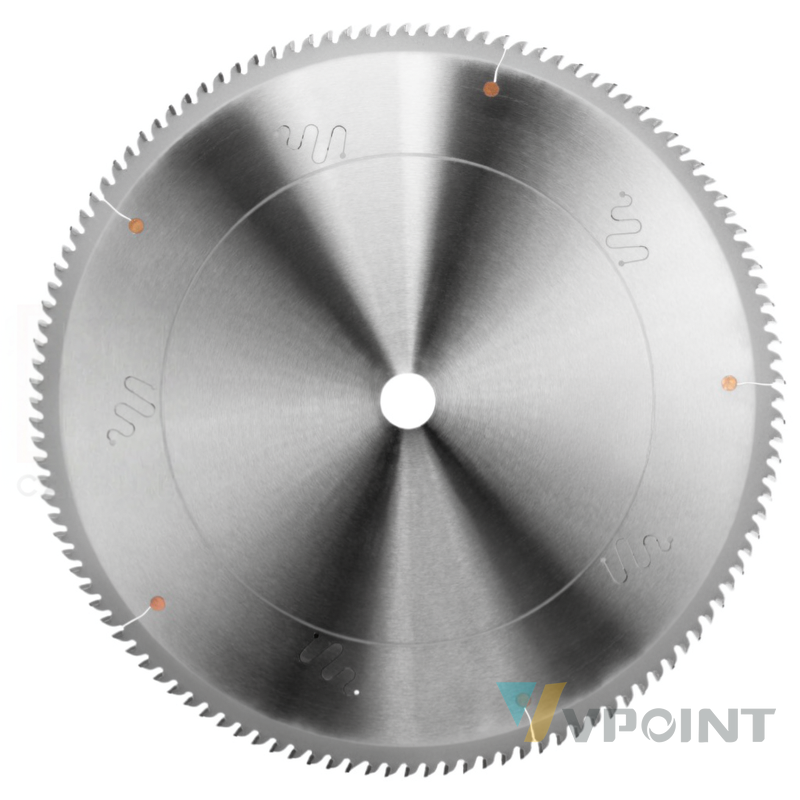
Design and Construction — a VPOINT woodworking cutting tool for panel sizing and crosscut work, sized for chipboard / particleboard and similar workpieces. The specification table below lists dimensions; the performance table gives standard reference values to start with, and the FAQ covers selection and service. ISO 9001 production, batch-verified, custom sizes from drawings.
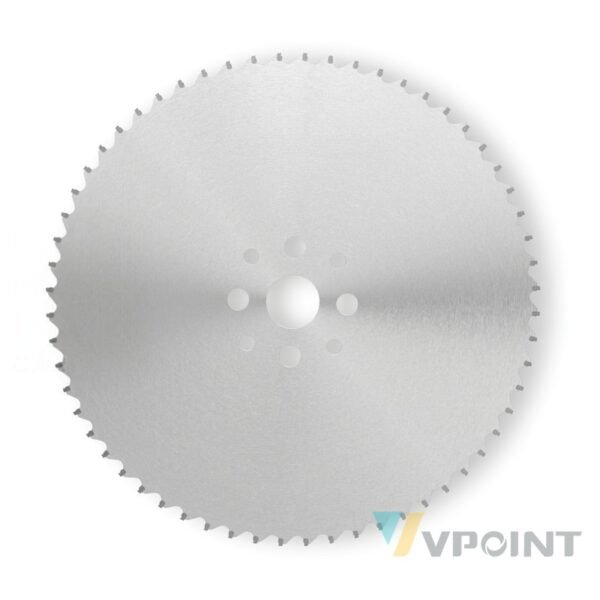
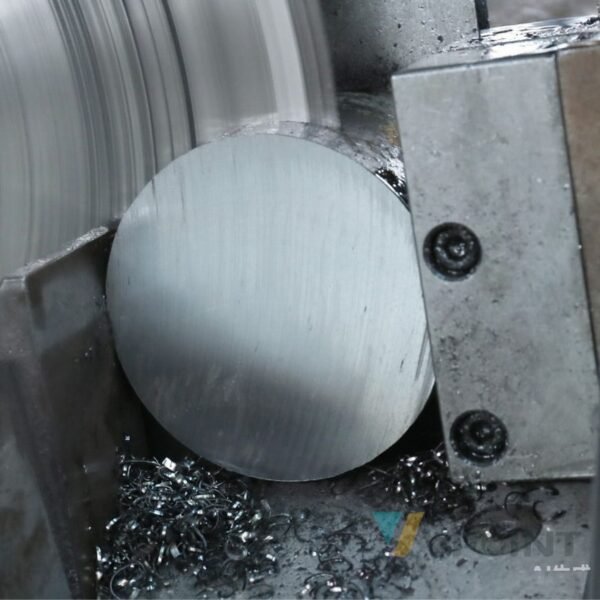
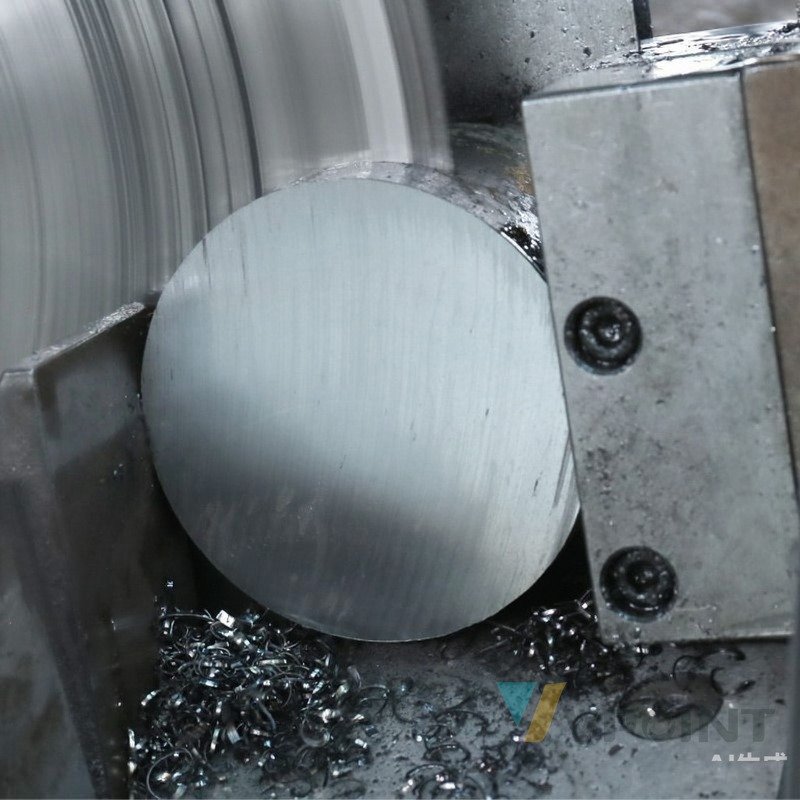
Explore high-performance cold saws for cutting high carbon steel with precision. These saws ensure clean, accurate cuts with minimal heat, preserving the steel’s integrity. Ideal for industries like automotive and metalworking, they offer durability, extended tool life, and efficient cutting solutions. Enhance productivity and reduce waste with our advanced cold saw technology.
Explore high-performance cold saws for cutting high carbon steel with precision. These saws ensure clean, accurate cuts with minimal heat, preserving the steel’s integrity. Ideal for industries like automotive and metalworking, they offer durability, extended tool life, and efficient cutting solutions. Enhance productivity and reduce waste with our advanced cold saw technology.
Characteristics:
1. Customized steel plate with rare alloy
2. Cermet alloy teeth
3. Special angle design
4. Perfect straight cutting Mirror surface
5. Durable
| Application | For high carbon steel cutting |
| Equipment | High precise cold saw machine |
| RPM | V=70-100m/min |
| The amount of cut per tooth | Bar FZ=0.04-0.07 Tube FZ=0.03-0.06 |
| Material | C≤0.75% Carbon steel, Alloy steel |
| Tips | Cermet alloy |

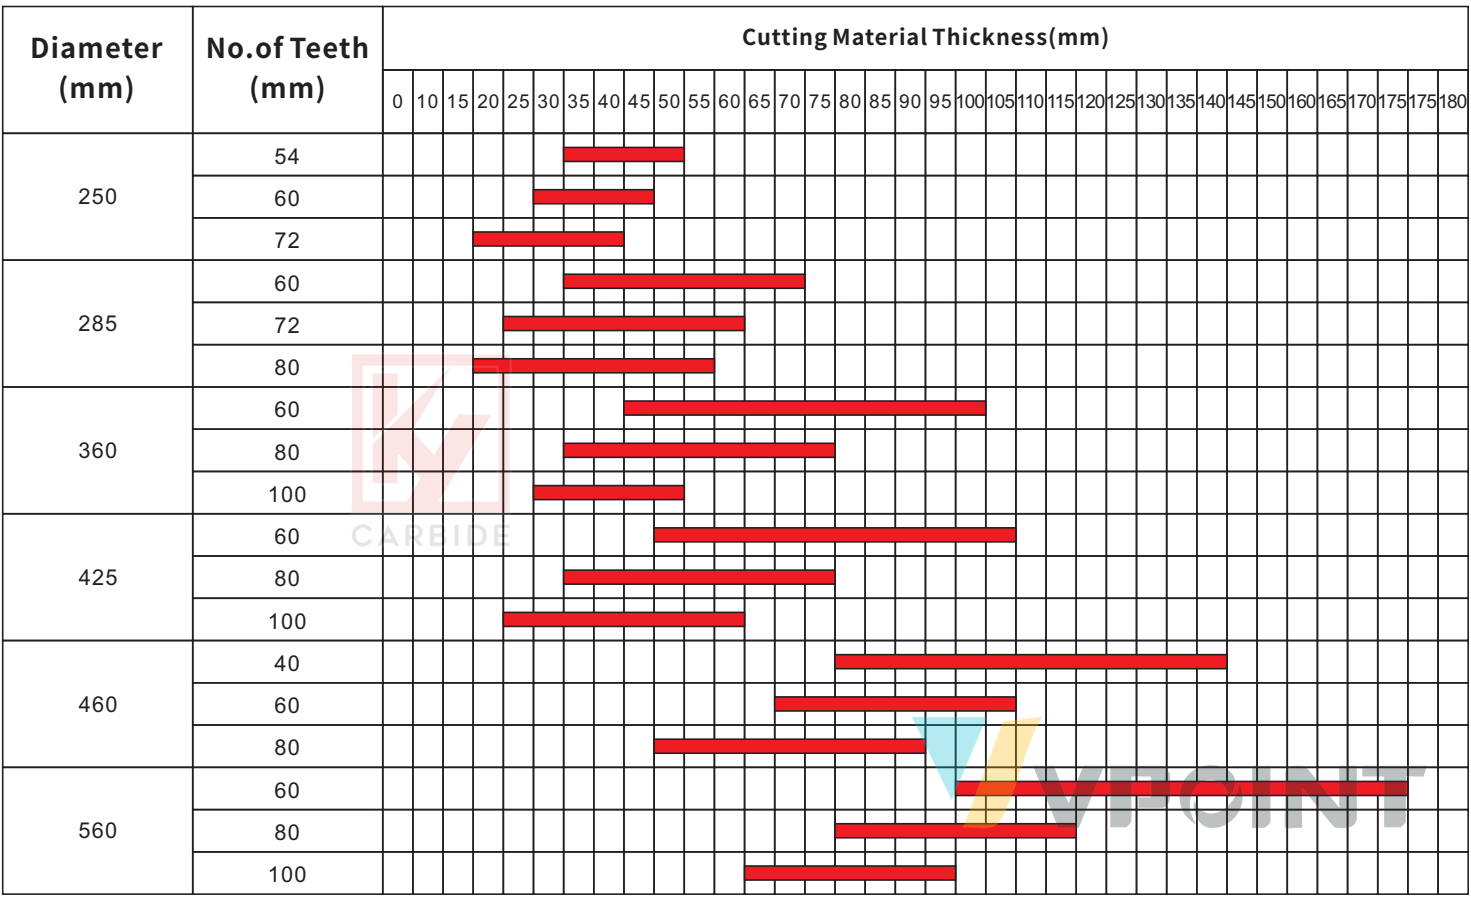
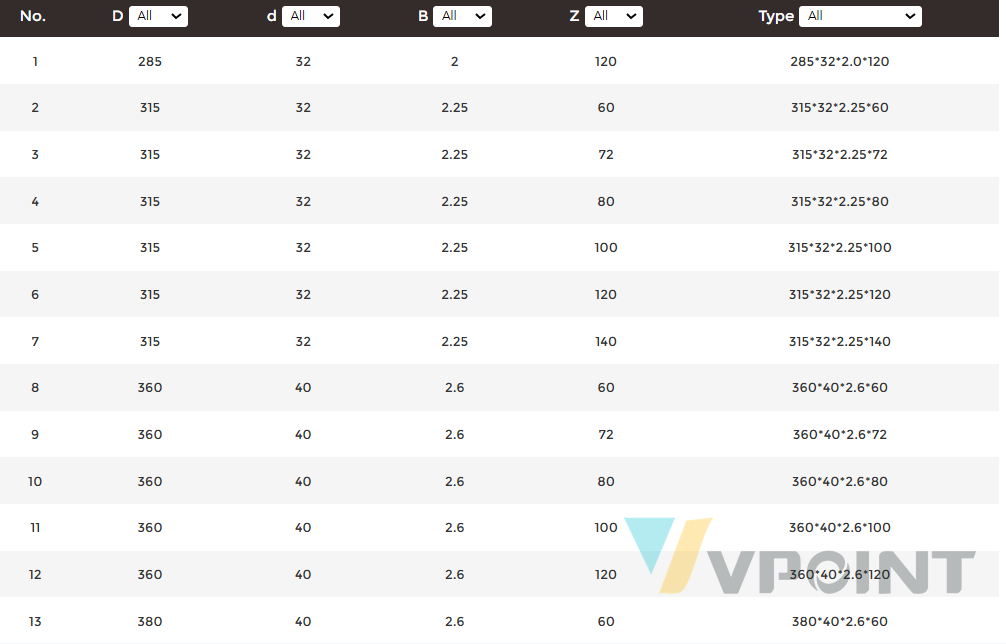
Cold saws for high carbon steel cutting offer precision, durability, and efficiency. Designed to provide clean cuts with minimal heat, they preserve the material’s integrity, making them ideal for industries like automotive and metalworking. These saws enhance productivity, extend tool life, and reduce material waste.
Design and Construction
The cold saw for high carbon steel cutting carries tungsten carbide teeth for high-precision cold saw machines: cutting speed 70-100 m/min, feed per tooth 0.04-0.07 mm (bar) and 0.03-0.06 mm (tube), for material up to C 0.75% carbon steel and alloy steel. The specifications table lists the full data as stated by the factory.
How It Works
High-carbon and alloy steels are harder than plain carbon: the slower speed range and lower feed per tooth keep each carbide tooth in its efficient range, and the cold-saw action keeps the cut face free of heat damage.
Applications
- Cold sawing high carbon steel
- Alloy steel bar and tube cutting
- Precision end faces on hard steel
- Bearing and tool steel components
Suitable Materials
- High carbon steel (C ≤ 0.75%)
- Alloy steel
- Steel bar and tube
- Hardened steel components
Slower speed and controlled feed keep the carbide edge efficient on hard carbon and alloy steels.
Material Comparison: Tungsten Carbide vs. High-Speed Steel (HSS) Body
These blades are carbide-tipped. The figures below are typical industry data showing where carbide tipping and high-speed steel each win, so you can match the material to the job.
| Property | Tungsten Carbide | High-Speed Steel (HSS) Body |
|---|---|---|
| Hardness | 89–91 HRA (carbide-tipped) | 65–67 HRC (M2/M42 HSS body) |
| Hot hardness | Keeps hardness at ~900–1,000 °C | Softens above ~600 °C |
| Feed and speed | Higher cutting speeds and feeds on steel | Moderate speeds; gentler on the saw |
| Re-conditioning | Tips re-tipped by the factory | Re-ground in-house many times |
| Best suited for | Production cutting of medium and high carbon steel | General-purpose cutting and cost-sensitive work |
Delivery Scope
Single blade. Order by the specification stated in the specifications table below.
Why Choose VPOINT
- One-year warranty on every cutter — defects in material or workmanship are covered for 12 months from delivery.
- Custom tooling — diameters, shanks, cutting lengths and flute configurations built to your drawing or sample.
- Non-standard fabrication — sizes outside the standard catalogue, including special geometries.
- Resharpening service — cutters return to service after regrinding at a fraction of new-tool cost.
- Factory-direct since 2008 — ISO 9001 manufacturing in Sichuan and Dongguan, China; no trading intermediaries.
Send a drawing, a sample or a worn tool, and our engineering team will quote the exact specification you need.
Precision & Quality Control
Every cutter is inspected before shipment. Shank diameter, cutting-edge diameter, cutting length and overall length are measured against the values listed in the specifications table, and cutting edge runout is verified on the assembled tool.
Tools measuring outside tolerance do not ship. Inspection is performed under our ISO 9001 quality system, with batch records retained for traceability.
Key words: high carbon cold saw blade, alloy steel saw blade, cold saw carbide, hard steel cutting blade, saw blade, panel saw blade, scoring saw blade, circular saw blade, carbide saw tips, TCT saw blade, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, furniture manufacturing, furniture factory, cabinet making, panel furniture, kitchen cabinet production, woodworking machinery, CNC router, woodworking cutting tools, acrylic sheet, solid wood, particleboard, chipboard, plywood, rubber sheet, rubber board, hardwood, softwood, MDF, HDF, melamine board, flycutter, planing bit, surfacing bit, slab flattening bit, bottom cleaning bit, spoilboard leveller, rabbeting bit
Performance Data
Standard reference values for guidance only — always adjust to machine rigidity, clamping and tool wear, and confirm on the actual workpiece.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| chipboard / particleboard | 4,500–6,000 rpm | 10–18 m/min | TCT teeth resist abrasive glue |
| MDF / HDF | 5,000–6,500 rpm | 9–16 m/min | Smooth kerf, minimal fuzzing |
| melamine-faced panels | 4,500–5,500 rpm | 8–14 m/min | Score first to prevent face chipping |
| solid wood | 4,800–6,000 rpm | 10–15 m/min | Alternating grain demands sharp teeth |
Frequently Asked Questions
How do I choose the tooth count?
+More teeth give a cleaner edge on thin or faced panels; fewer teeth clear chips faster on thick stock.
What arbor speed suits this blade?
+Set by diameter and tooth count — larger diameters run slower; start near 4,500–6,000 rpm for panel work.
How often should the blade be serviced?
+At the first burn marks or heavy feed resistance; a sharpened tooth costs less than a rejected panel.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification
Related Search Terms
PCD saw blade, diamond saw blade, panel sizing saw blade, PCD scoring blade, diamond tip circular saw, carbon, steel, cutting
\n\n