- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
Tire Stud Screws in 6/7/8/9/10 mm with Screw-In Fixing: Applications, Materials and Selection Notes

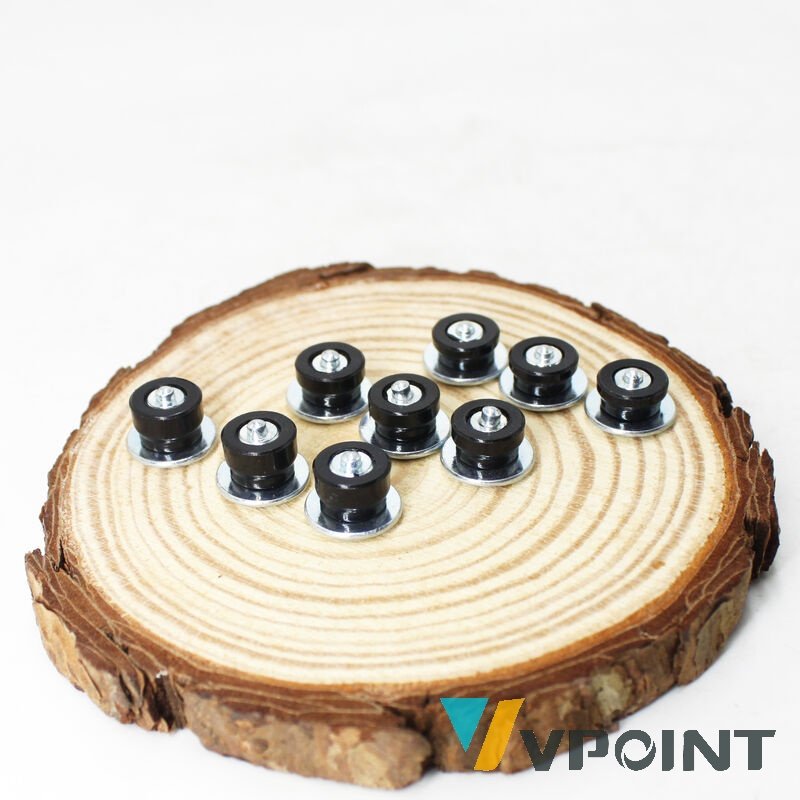
What this product is. Tire stud screws in 6, 7, 8, 9 and 10mm lengths with a tungsten carbide core. The threaded body is the defining feature: the stud is screwed into the tread rather than pressed, which changes both installation and removal.
View Tire Stud Screws in 6/7/8/9/10 mm with Screw-In Fixing →
Specification and how to order
Published specification: Item | Specification | Type | Tire stud screws | Lengths | 6 / 7 / 8 / 9 / 10 mm | Fixing | Threaded screw-in | Core | Tungsten carbide | Supply | Bulk | Inspection | Per-lot thread and length |
- The grade designation and binder content, in writing.
- Dimensions with the tolerance that actually matters to your grinding or brazing operation.
- Grain size, where edge sharpness or wear resistance depends on it.
- Surface condition: as-sintered or ground.
- Quantity and packing, because small blanks are usually packed by piece count or by weight.
Where it is used
- Brazing onto drill, mining, road-planing and wear-part bodies.
- Blanks that are ground into burrs, drills and cutters in a tool room.
- Pellets and crushed grit for hardfacing and welding consumables.
- Preforms for press-tool and wear applications.
Handling and storage
- Carbide is hard but brittle: do not drop blanks or carry them loose in a box.
- Keep the batch dry, and lightly oiled where a steel carrier or a brazed assembly would corrode.
- Store by grade and size. Mixing grades in one bin is the most common way a wrong grade reaches the brazing bench.
- Treat a chipped corner on a ground blank as scrap: it will show up as a defect in the finished tool.
Checks on receipt
- Measure a sample against the drawing, not against the previous delivery.
- Look for cracks, chipping and surface porosity under a magnifier.
- Confirm the grade marking on the box matches the paperwork.
- Record the batch number so a problem can be traced back to a delivery.
Compared with the alternative
Compared with a finished tool, a blank leaves the grinding to the tool shop: the geometry stays under your control and the grade is chosen for the application, at the cost of an extra grinding step.
From the product comparison section: How the fixing route changes service. Typical industry practice: Factor | Screw-In (this stud) | Press-In | Removable Core | Retention mechanism | Thread + rubber | Rubber grip only | Seat + replaceable core | Installation speed | Slower | Fastest | Moderate | Individual replacement | Yes | Difficult | Yes (core only) | Equipment | Screwdriver / tool | Studding gun | Seat tool + core tool | Risk o…
Frequently asked questions
Can you supply to a drawing?
Yes. Send the drawing with the grade, the quantity and the tolerance that matters marked, and the quotation will be against that drawing rather than against a catalogue size.
As-sintered or ground?
Both are available. Grinding adds cost and lead time, and is worth it where the blank locates on a ground face or the edge is used without further machining.
What is the minimum order?
It depends on size and grade. Small trial quantities can be agreed before a production order so the grade can be tested in your own process.
Sources and standards
Amana Tool. "Knowledge Base: shank concentricity, collet installation, vibration and sharpening." www.amanatool.com/knowledge_base. Accessed 10 Nov. 2026.
Amana Tool. "Safety Guidelines for Router Bits and Saw Blades." www.amanatool.com/safety. Accessed 10 Nov. 2026.
C.M.T. Utensili. Router bit instruction sheet: collet seating, feed rate and maintenance guidance. Accessed 10 Nov. 2026.
Standards: ISO 9001 · UNSPSC · eClass
Full specifications for Tire Stud Screws in 6/7/8/9/10 mm with Screw-In Fixing · Resources hub · Ask a VPOINT engineer on WhatsApp →