- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
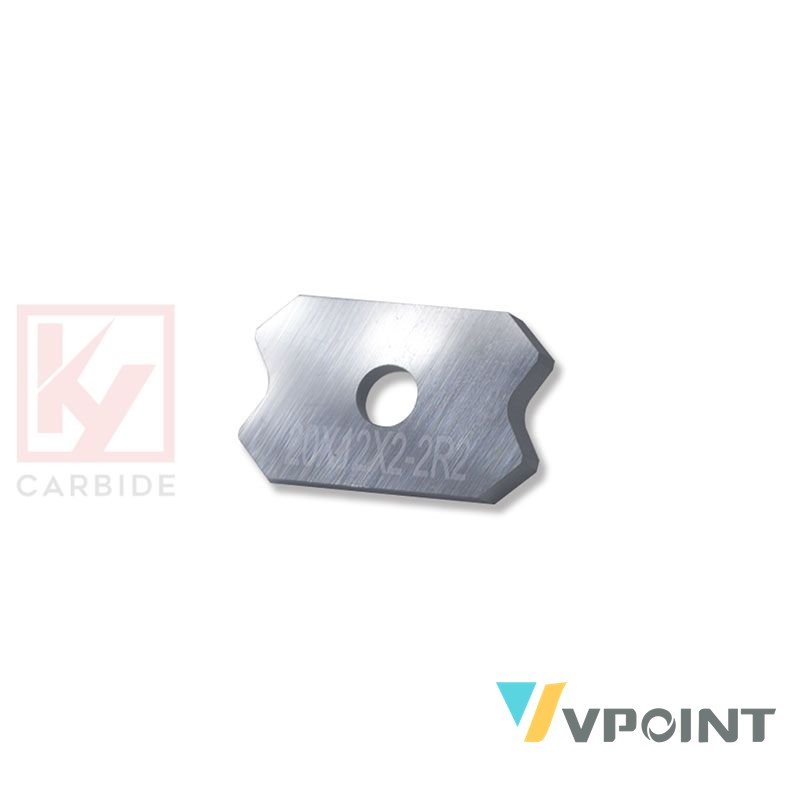
20x12x2mm Carbide Radius Profile Knives: Applications, Materials and Selection Notes

Workshop report from a real user thread. A tooling comparison notes that many shops keep TCT for varied work and PCD for the highest-run profiles, because changeover time dominates high-volume lines.
View 20x12x2mm Carbide Radius Profile Knives →
What actually went wrong
For mixed-production shops the pain is not raw life but the number of interventions per shift.
How 20x12x2mm Carbide Radius Profile Knives addresses this problem
An indexable head reduces those interventions without committing the whole shop to diamond tooling. The radius knives seat in the head pocket and present a ground radius edge: as the panel feeds past, the radius forms in one pass. When an edge dulls, the knife is turned or swapped in minutes — the head stays in the machine and the profile holds its position.
Why this matters for a buyer: Production shops lose output to tool changes: a brazed or solid-carbide profile bit has to leave the spindle for sharpening, and every re-setup risks a dimension shift. A dull edge then starts rubbing instead of cutting, and heat, burn marks and resin build-up follow.
Why shops switch to insert tooling
- Rotate a reversible knife 90 degrees to a fresh edge in the machine, in about a minute: no tool removal, no re-setting, no re-zeroing the spindle.
- The cutting diameter stays constant after rotation, so the first panel and the five-hundredth come out the same size.
- A knife costs a fraction of a brazed or solid profile tool, so a worn edge is a consumable, not a repair.
- Knife seats and screws are the only wear parts; the steel body stays on the spindle for years.
Capability and specifications
The 20 x 12 x 2 mm carbide radius profile knives carries replaceable tungsten carbide insert knives on a 40Cr chrome-molybdenum steel body for spindle and moulder work. The size table covers lengths (L) of 12 to 20 mm, widths (W) of 12 to 17.5 mm, thicknesses (T) of 2 mm and radius values (R) from R1 to R3 per the specifications table.
Which machines this tool is built for
Machine choice changes the result more than most operators expect. The same tool on a rigid spindle with a power feed behaves differently from the same tool fed by hand: chip load, heat and finish all shift. The table below states where this tool is the right choice, what it actually delivers there, and where it should not be used.
| Machine | Fit | What you get | Key limit |
|---|---|---|---|
| CNC router | Recommended | The best control of feed and RPM. Because rotating a knife keeps the cutting diameter, nested parts stay identical across the batch and the Z datum does not need resetting. | Needs a rigid collet or toolholder and effective extraction; a light hobby gantry will chatter on large diameters. |
| Router table | Workable with limits | Gives a stable, repeatable fence for edge profiles on shank-type insert bits. Feed is by hand, so surface quality depends on steady pressure through the cut. | Shank versions only. Bore-mounted cutterheads cannot be run on a table. |
| Hand-held trimmer | Not recommended | A trimmer is sized for small laminate bits. An insert head is heavy and large in diameter, so balance and control are lost. | Keep hand-held work to light flush trimming with a small solid-carbide bit. |
| Spindle moulder | Recommended | The natural home for bore-mounted insert cutterheads: power feed, brake, guard and a rigid spindle hold the cutting circle steady through long runs. | Spindle speed must suit the cutter diameter; never exceed the marked limit. |
| Four-side moulder | Recommended | Continuous feed and mechanical pressure keep the profile constant over thousands of metres. A knife rotation becomes a planned stop, not a breakdown. | Needs the correct spindle arrangement and jointed knives for the finish pass. |
Machine by machine: what to expect
CNC router. The best control of feed and RPM. Because rotating a knife keeps the cutting diameter, nested parts stay identical across the batch and the Z datum does not need resetting. Needs a rigid collet or toolholder and effective extraction; a light hobby gantry will chatter on large diameters.
Router table. Gives a stable, repeatable fence for edge profiles on shank-type insert bits. Feed is by hand, so surface quality depends on steady pressure through the cut. Shank versions only. Bore-mounted cutterheads cannot be run on a table.
Hand-held trimmer. A trimmer is sized for small laminate bits. An insert head is heavy and large in diameter, so balance and control are lost. Keep hand-held work to light flush trimming with a small solid-carbide bit.
In short: if the work is repetitive and the machine is rigid, this tool is at its best. If the setup relies on hand control, expect the finish to depend on feed discipline rather than on the tool alone.
Typical production applications
- Kitchen and wardrobe doors: stile-and-rail and raised-panel profiles run on a spindle moulder.
- Furniture frames: rebating and flush trimming on a CNC router.
- Window and door components: profile runs where the cutting diameter must not drift between batches.
- Panel edge preparation before banding, where a constant diameter keeps the joint line even.
Each of these is a repeated operation, which is where consistency matters more than a single good test cut: the first part and the five-hundredth part have to match.
Installation, step by step
- Isolate the power first. Unplug the router, or remove the battery pack on a cordless machine, before touching the collet. A machine that cannot start cannot injure a hand.
- Clean the collet and the shank. Wipe resin and dust from the collet taper and from the full length of the shank with a solvent-damp cloth. A contaminated collet cannot clamp evenly, and uneven clamping is the root of most runout complaints.
- Match the collet to the shank exactly. 6 mm, 6.35 mm (1/4 in), 12 mm and 12.7 mm (1/2 in) are different sizes. Never shim a small shank into a large collet, and never rely on a worn collet to hold a nominal size.
- Seat the shank fully, then back off 1/16 in. Push the bit in until it bottoms out, then withdraw it about 1/16 in (1.6 mm). This leaves room for shank expansion and stops the bit freezing in the collet.
- Keep enough shank engaged. Aim for at least three quarters of the shank length inside the collet. A bit gripped only near the tip will slip, chatter or break at the collet mouth.
- Tighten with two wrenches, firmly but not brutally. Hold the spindle and turn the collet nut. Over-tightening stretches the collet and reduces its grip next time; under-tightening lets the bit creep down during the cut.
- Check runout before the first cut. Spin the spindle by hand and look for wobble, then run the tool in free air and listen. Any visible wobble means re-seat the bit, not run it in.
Two rules cover most of the risk: the shank or bore must be clean, and the tool must be seated with enough engagement. Everything else, torque, projection, guard clearance, is a check on those two.
Installation mistakes that cause most failures
- Shank inserted only halfway Contact area drops, vibration rises, and the bit can slip or be ejected. Seat the full shank, then back off 1/16 in.
- Shank bottomed out in the collet There is no room for expansion, clamping force becomes uneven, and the bit can freeze so tightly that it cannot be removed.
- Dirty or resin-coated shank The classic cause of a rippled wall and chatter: the bit runs off-centre no matter how hard the nut is tightened.
- Worn collet kept in service Concentricity is lost permanently. No amount of torque restores it, and the tool starts breaking at the collet mouth.
- Over-tightening the collet nut Stretches the collet and deforms it, which reduces grip on every tool fitted afterwards.
- Excessive overhang or an unnecessarily long cutting edge Length compounds vibration and deflection, and deflection is a leading cause of tool breakage. Use the shortest cutting edge that does the job.
- A large-diameter bit run at full speed Mass and RPM together create vibration and imbalance. Respect the diameter and RPM limit for the tool.
Rules during the cut
- Never start the spindle with the tool touching the workpiece. Let it reach full speed first, then enter the cut.
- Feed against the direction of rotation. Feeding with the rotation climbs the work and invites a kickback.
- Take shallow passes. Depth per pass should suit the tool diameter, the material and the machine rigidity.
- Watch the chips. Chips mean the edge is cutting; fine dust means it is rubbing, and heat is building.
- Keep extraction running for the whole cut. Recut chips are the fastest way to bake resin onto a flute.
- Stop the moment the sound changes. A new squeal or knock is cheaper to investigate than a broken tool or a scrapped panel.
- Do not reach near the tool until the spindle has fully stopped.
Maintenance and inspection schedule
| Interval | What to do |
|---|---|
| Every shift | Wipe resin from the flutes and the shank with solvent and a soft brush. Inspect the cutting edges under a light for chipping, a bright wear land or blue heat marks. Check that the collet or flange is clean before mounting. |
| Weekly | Check runout with a dial indicator against the toolmaker limit. Inspect the collet for scoring or ovality and replace it if marked. On bearing-guided tools, check the bearing for wobble and free rotation. Verify extraction airflow at the hood. |
| Monthly | Review the tool log by tool number: metres cut, material, and any change in finish or feed force. Send the tool for resharpening when finish drops or feed force rises, not on a calendar date. Replace worn collets and damaged screws as consumables. |
Inspect with a 10x magnifier in good light. What to look for: a chipped or flaked corner, a bright wear land running back from the edge, cracks at the joint between carbide and steel body, blue or straw discolouration from heat, and resin filling the flute. On a mounted tool, a dial indicator on the shank or body shows runout, and a test cut in scrap shows the result that matters.
When to stop using a tool: any visible crack, a chipped cutting corner, a bent shank or a body that has been run hot is a removal, not a touch-up. A tool that has lost its edge can be resharpened; a tool with a crack cannot be made safe.
Why tools break, chip or deform
Nearly every failure has a setup cause rather than a manufacturing cause. The table maps the symptom an operator sees to the mechanism behind it and the correction that actually removes the cause.
| Symptom | Most likely cause | Correction |
|---|---|---|
| Tool snaps at the collet mouth | Too much overhang, an unnecessarily long cutting edge, or a worn collet that lets the tool flex. | Shorten the overhang, use the shortest cutting edge that suits the job, replace the collet, and reduce depth per pass. |
| Tool creeps down or pulls out mid-cut | Shank bottomed out in the collet, or oil and dust on the shank reducing friction. | Seat fully then back off 1/16 in, clean the shank and collet with solvent, and re-torque. |
| Chatter and a rippled wall | Worn or wrong-size collet, debris in the taper, or a machine spindle with runout. | Replace the collet, clean the taper, check spindle runout, and reduce depth per pass. |
| Chipped corner on the carbide | Impact with a fastener, a hard knot or a glue line, or a tool dropped on the bench. | Inspect stock and use metal detection, store the tool in its case, and keep a spare for the finishing pass. |
| Burn marks and resin build-up | Feed too slow for the RPM, a dull edge, or poor extraction. | Raise feed or lower RPM, clean the resin off, and restore extraction before the next batch. |
| Blue shank or discoloured tip | Heat from forced feed, packed chips or no extraction. | Reduce depth per pass, clear chips, and treat a discoloured tool as worn, not just dirty. |
| Vibration immediately after mounting | Bent shank, damaged collet, or an unbalanced large-diameter tool run too fast. | Check runout with a dial indicator, replace the collet, and respect the diameter and RPM limit. |
Insert knives benchmarked against TIGRA
TIGRA, based in Oberndorf am Lech and founded in 1983, is the reference most European toolmakers use for reversible knife blanks. Its woodworking programme is built around named carbide grades: T04F as the universal grade covering hard and soft wood, chipboard and MDF; T07MF for hard and soft wood; T10MG for hard species at roughly 1650 HV10 with a 10 percent binder, not recommended for HDF, MDF or chipboard; T04MG for very hard species and glued panels; TL15 for softwood. The catalogue is sold as reversible knives, profiling blanks, saw tips, planer knives and PCD discs. A knife programme is therefore compared on measurable criteria, not on a brand claim.
| What to compare | Why it decides the result | What to ask for |
|---|---|---|
| Grade and hardness (HV10) | Hardness and binder content set the balance between wear resistance and edge toughness. A grade that is too hard for an interrupted cut chips; too soft and it wears a rounded edge that burns the work. | The grade name, the HV10 value and the binder percentage in writing, plus which materials the grade is and is not recommended for. |
| Cutting edges per knife | Each edge is a service interval. Four usable edges per knife means four rotations before the tool leaves the spindle. | Whether the knife is a true four-edge reversible type and whether all four edges are finish-ground, not just two. |
| Thickness tolerance | Knife thickness sets the cutting circle. If a replacement knife is a few hundredths thinner, the joint shows and the profile changes depth. | The thickness tolerance band, and confirmation that a spare batch will hold the same cutting circle as the first. |
| Seat and clamping fit | A knife that does not sit flat in its pocket rocks under load, which is how seats wear and screws loosen. | Flatness of the seat, screw grade and torque value, and whether screws are supplied with each knife set. |
| Profile and size coverage | The gap between a catalogue blank and a finished profile is machining time, or a second supplier. | Whether the blank is supplied pre-profiled to the drawing, and how a custom profile is quoted. |
| Supply model | Lead time and minimum order decide whether a knife programme fits a shop that runs mixed batches. | Stock sizes, MOQ for custom profiles, lead time, and whether OEM marking is available. |
Where a VPOINT insert tool is the stronger buy: the body and the knives come from one source, so a fit problem is one conversation instead of two. Custom profiles are quoted from a drawing with no separate tooling supplier in between, small and mixed orders are accepted, and engineering questions are answered directly by the factory that grinds the knife. For a shop that buys European blanks and machines its own bodies, that single-point responsibility is usually worth more than a catalogue line item.
Where TIGRA is genuinely stronger, stated plainly: the catalogue depth is larger than any single Chinese factory can match, grade consistency is backed by decades of production data, and European stock and logistics are shorter for a European buyer. A buyer comparing on brand alone will choose TIGRA. A buyer comparing on cost per finished metre, lead time for a custom profile, and how quickly a seat problem is resolved will usually shortlist both.
Where it wins, and where it does not
Advantages: Radius profiling on spindle moulders Edge rounding on panel lines Cabinet and furniture profile work Production moulding heads
Limitations, stated honestly: Solid wood, plywood, chipboard, MDF and laminated panels within the cutter geometry. Not for steel, stainless steel, stone, or boards with nails and heavy glue lines.
Machining characteristics and performance
Standard reference values for guidance only — always adjust to machine rigidity, clamping and tool wear, and confirm on the actual workpiece. Material | Typical spindle speed | Typical feed | Notes | solid wood profiles | 10,000–14,000 rpm | 5–10 m/min | Sharp edges slice dense grain cleanly | MDF / particleboard | 12,000–16,000 rpm | 6–10 m/min | Watch glue-line wear on the profile | veneered panels | 12,000–14,000 rpm | 5–8 m/min | Profile the spare before the show face |
All published parameter values are standard reference values for guidance only. Confirm them against your tool, spindle and workpiece before a production run.
Compared with the alternative
Compared with a brazed carbide or solid-carbide bit, an indexable head trades a higher purchase price for near-zero setup downtime: rotating a knife keeps the cutting diameter constant, while a brazed bit must be removed and reground.
From the product comparison section: Insert systems keep the body in service and replace only the cutting edges. For production work, this is usually the lower-cost way to hold edge quality. Property | Replaceable Insert Knife (This Tool) | Solid Profile Knife | Edge replacement | Swap the worn insert only; the steel body stays in service | Regrind or replace the complete tool | Body material | 40Cr chrome-molybdenum steel body, reus…
Materials and machine fit
Materials it cuts: Solid wood MDF and particleboard Plywood and veneered panels Laminated boards The ground radius inserts hold the profile geometry across long production runs.
Solid wood, plywood, chipboard, MDF and laminated panels within the cutter geometry. Not for steel, stainless steel, stone, or boards with nails and heavy glue lines.
Machine fit: CNC routers, shapers, moulders and spindle moulders with a matching shank or arbor. Not for hand-held die grinders or metalworking machining centres.
Frequently asked questions
A steady moderate feed with sharp knives; fuzzing means rotate or replace before adjusting anything else.
The answer depends on the workpiece and the machine setup. The specification table on the product page is the starting point, and our engineers can confirm it against your machine on WhatsApp.
Each profile radius is its own cutter — match the cutter to the profile drawing rather than forcing one radius into several.
Use the parameter table as a reference and verify on a test cut before a production batch.
Can I use this tool in a hand-held trimmer?
Generally no. A hand-held trimmer does not give the balance, guarding or rigidity this tool needs; the machine table above sets out what it is designed for.
How deep should the shank sit in the collet?
Insert it until it bottoms out, then withdraw about 1/16 in (1.6 mm), and keep at least three quarters of the shank length gripped. That leaves room for expansion and prevents the tool freezing in the collet.
Why did my previous bit break at the shank?
The usual combination is too much overhang with a collet that no longer holds concentric. Deflection at the collet mouth fatigues the shank until it snaps. Shorten the overhang, replace the collet and reduce depth per pass.
How often should it be sharpened?
By symptom, not by calendar: when surface finish drops, feed force rises, or the chips turn to dust. Send the tool for service with its tool number so the log stays usable.
Sources and standards
Case source: Leabon Carpentry Accessories. "Carbide vs PCD Diamond Router Bits." www.carpentryaccessories.com. Accessed 10 Nov. 2026.
Amana Tool. "Knowledge Base: shank concentricity, collet installation, vibration and sharpening." www.amanatool.com/knowledge_base. Accessed 10 Nov. 2026.
Amana Tool. "Safety Guidelines for Router Bits and Saw Blades." www.amanatool.com/safety. Accessed 10 Nov. 2026.
C.M.T. Utensili. Router bit instruction sheet: collet seating, feed rate and maintenance guidance. Accessed 10 Nov. 2026.
TDT Diamant. "PCD tools in comparison: advantages over carbide and CVD." www.tdt-vertrieb.de. Accessed 10 Nov. 2026.
Litian Century Diamond Tools. "PCD inserts vs cermet vs carbide vs CBN." www.ltctdiamonds.com. Accessed 10 Nov. 2026.
Standards: ISO 9001 · UNSPSC · eClass
Full specifications for 20x12x2mm Carbide Radius Profile Knives · Resources hub · Ask a VPOINT engineer on WhatsApp →