- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
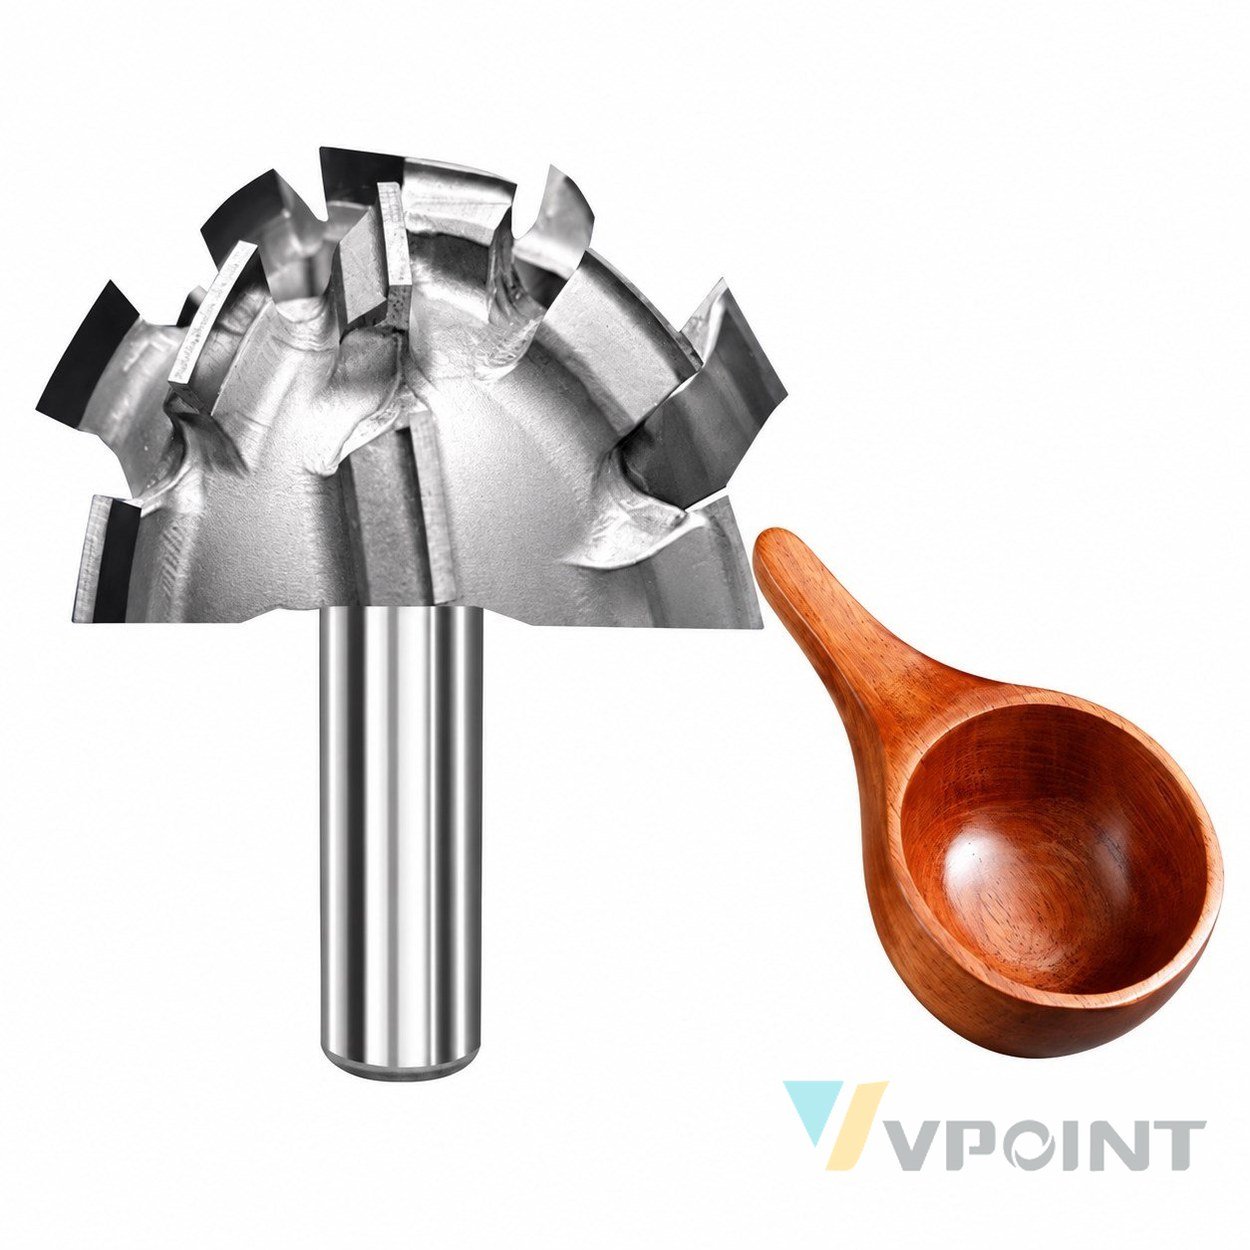


Design and Construction — a VPOINT PCD V-groove / special-profile router bit for V-groove, signmaking and decorative panel work, sized for MDF and similar workpieces. Start near 20,000–24,000 rpm / 8–12 m/min (standard reference values in the performance table below); the specification table lists angles, diameters, cut lengths and shanks. Diamond edges hold 15–20× carbide life on abrasive panels. ISO 9001 production, batch-verified, custom sizes from drawings.
Design and Construction
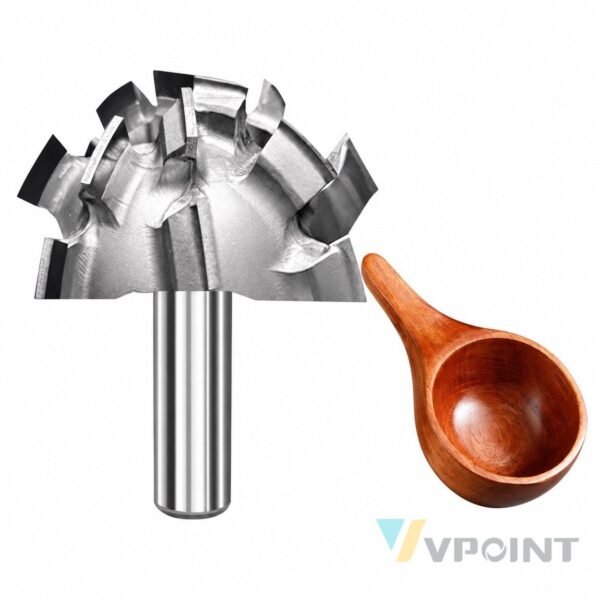
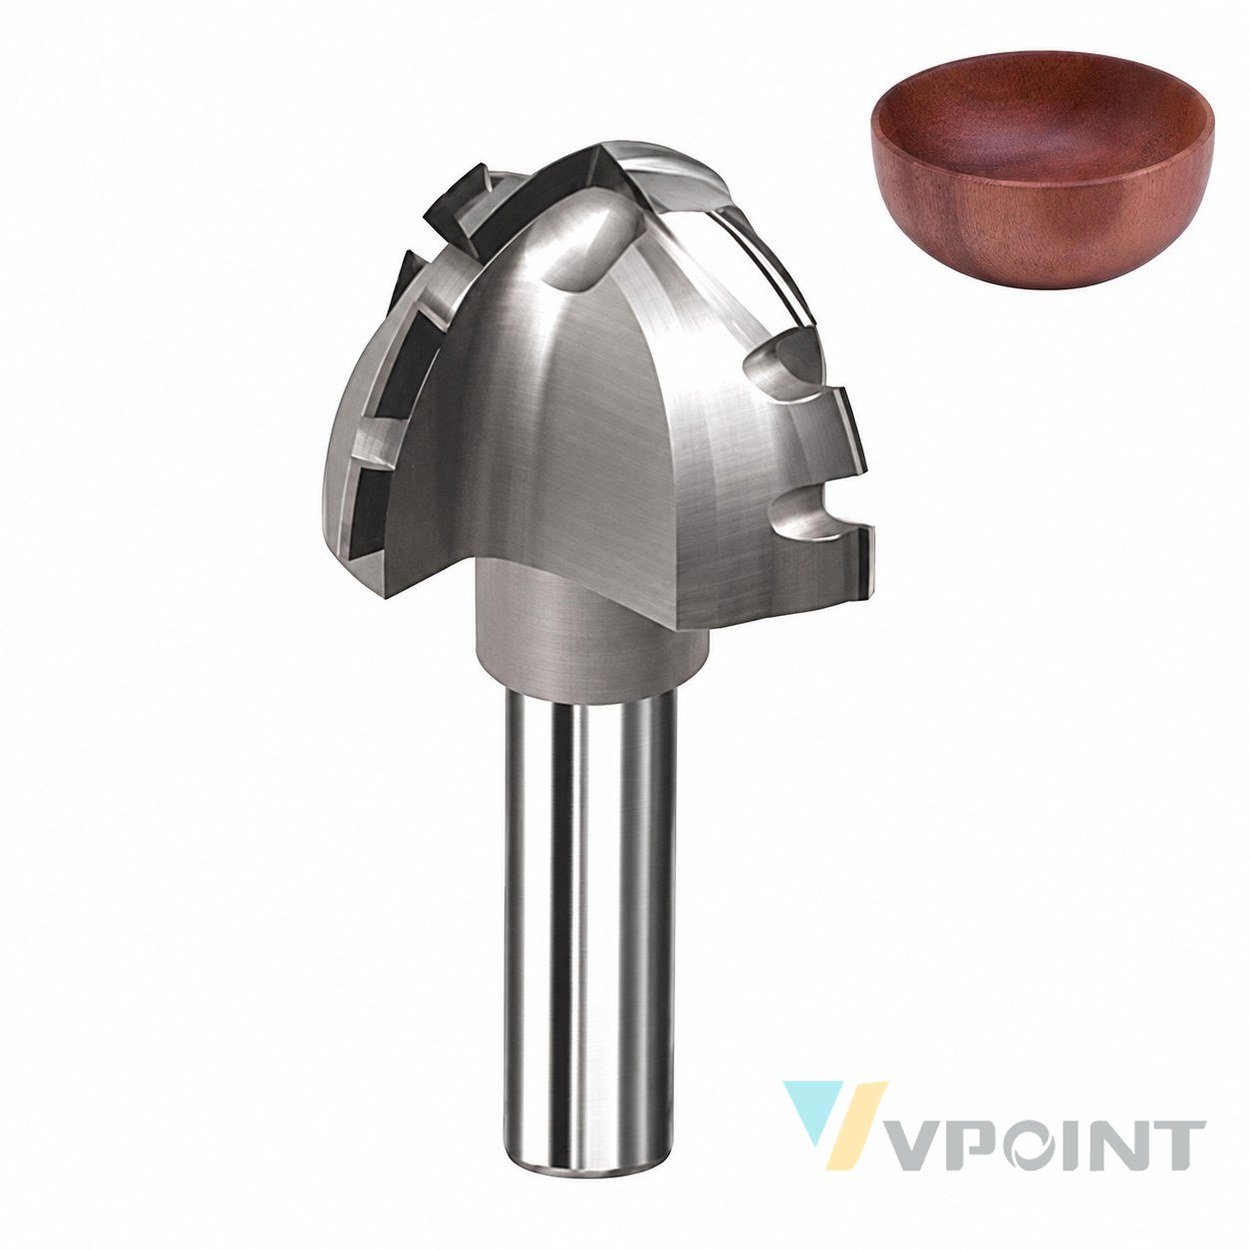
The PCD spiral round-bottom router bit family machines shaped recesses, including the pictured bowl and spoon applications. The chart lists 20 mm shank diameter with 65 mm (33 mm head height, 2+2T) and 55 mm (28 mm head height, 3+3T) head configurations as supplied; the cutting material is PCD.
How It Works
The ball-nose head sweeps the recess in CNC passes: the spiral diamond teeth shear the curved bottom and walls while the 20 mm shank matches the tool holder. The pictured bowl and spoon show the typical finished applications of this head family.
Applications
- Shaped recesses (bowls, spoons)
- 3D CNC surface machining
- Round-bottom cavity work
- CNC router production runs
Suitable Materials
- Hardwood blanks
- Selected softwoods
- Wood-based bowl and spoon stock
- Selected tool-handle materials

Material Comparison: Tungsten Carbide vs. PCD (Diamond)
This tool is a PCD (polycrystalline diamond) cutter. Tungsten carbide is the conventional alternative. Typical industry data:
| Property | Tungsten Carbide Cutter | PCD (Diamond) Cutter (This Tool) |
|---|---|---|
| Hardness | 1,500-2,000 HV | 7,000-9,000 HV |
| Best suited for | General profiling across mixed materials | Highly abrasive boards and long production runs |
| Tool life vs. carbide baseline | 1x (baseline) | 10-15x on abrasive panels (typical industry data) |
| Edge wear on MDF/particleboard | Wear visible within shorter runs | Minimal wear over extended runs |
| Toughness | Higher toughness; tolerates impacts better | Lower toughness; sensitive to impact and metal contamination |
| Regrinding | Can be reground | Not reground in the normal case |
| Initial cost | Lower | Higher |
| Cost per part at long runs | Usually higher | Usually lower on abrasive, long-run work |
| Typical choice | Short runs and mixed materials | This tool: long-run profiling on abrasive boards |
Typical industry data; actual tool life varies with workpiece, machine and feeds.
Delivery Scope
- 1 x PCD Spiral Round-Bottom Router Bit (configuration per chart)
- Individual box packaging
Why Choose VPOINT
- One-year warranty on manufacturing defects
- Custom and non-standard geometries supported against drawings
- Regrinding service available for carbide components
- Factory-direct since 2008, ISO 9001 certified
- Manufacturing in Sichuan and Dongguan, China
Precision & Quality Control
Each cutter is inspected against the specification sheet before packing: bore and diameter tolerances, cutting geometry and balance are checked under the ISO 9001 quality system, with batch traceability on every order.
Specifications
+The source specification lists the following confirmed configurations:
| Shank diameter (mm) | Head diameter (mm) | Head height (mm) | Tooth configuration as supplied |
|---|---|---|---|
| 20 | 65 | 33 | 2+2T |
| 20 | 55 | 28 | 3+3T |
+Cutting material: PCD (diamond), as listed in the source chart.
Performance Data
Standard reference values for guidance only — always adjust to machine rigidity, clamping and tool wear, and confirm on the actual workpiece.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| MDF | 20,000–24,000 rpm | 8–12 m/min | PCD V-edges hold the 60° angle on abrasive MDF |
| particleboard | 18,000–22,000 rpm | 8–12 m/min | Grit-resistant diamond edges |
Frequently Asked Questions
Which configurations are listed?
+The chart lists a 20 mm shank with a 65 mm head (33 mm height, 2+2T) and a 55 mm head (28 mm height, 3+3T).
What is this bit used for?
+Shaped recesses such as the pictured bowls and spoons, machined on CNC routers.
Which shank does it use?
+A 20 mm shank as listed; confirm the collet size against your CNC tool holder before ordering.
What should I provide before ordering?
+Send the required recess shape, workpiece material and CNC machine details.
+Key words: pcd cutter, diamond cutter woodworking, pcd profiling cutter, diamond tip router bit, PCD straight router bit, diamond straight bit, PCD slotting cutter, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, furniture manufacturing, furniture factory, cabinet making, panel furniture, kitchen cabinet production, woodworking machinery, CNC router, woodworking cutting tools, woodworking, carpentry, DIY woodworking, acrylic sheet, solid wood, particleboard, chipboard, plywood, rubber sheet, rubber board, hardwood, softwood, MDF, HDF, melamine board, flycutter, planing bit, surfacing bit, slab flattening bit, bottom cleaning bit, spoilboard leveller, rabbeting bit
What feed should I start with when V-grooving MDF?
+Begin near 8–12 m/min at 20,000–24,000 rpm. The 60-degree PCD point holds its angle on abrasive boards, so the V line stays crisp; tune by chip load and line quality.
Why PCD for V-groove and decorative lines?
+The V point is the smallest, most heat-stressed edge on the tool. PCD at 7,000–9,000 HV keeps that point far longer than brazed carbide on abrasive panels.
Single or multiple passes for the V groove?
+One pass for thin veneers; two passes (rough then finish) on dense MDF above 12 mm keep the apex sharp and the line flutter-free.
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification
Related Search Terms
PCD router bit, PCD spiral router bit, diamond router bit, PCD tips, diamond compression end mill, PCD shank cutter, PCD helicoidal cutter, PCD vs brazed tungsten carbide, diamond cutting tool for MDF, PCD tooling for chipboard, polycrystalline diamond router bit, spiral, round, bottom, router