- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling
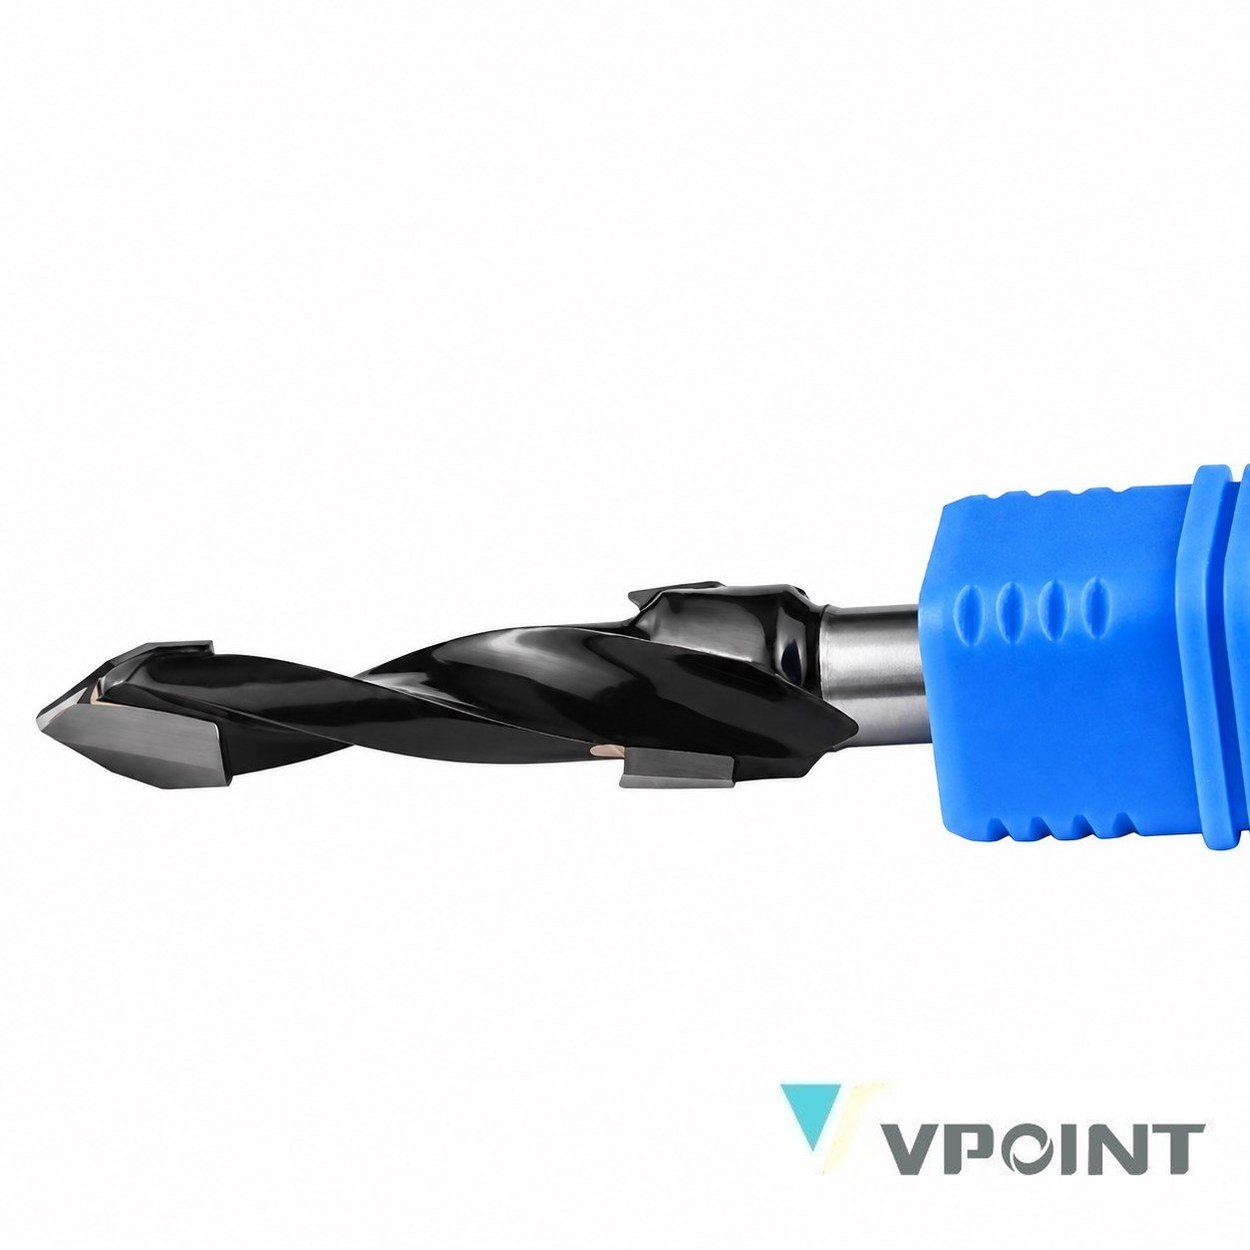
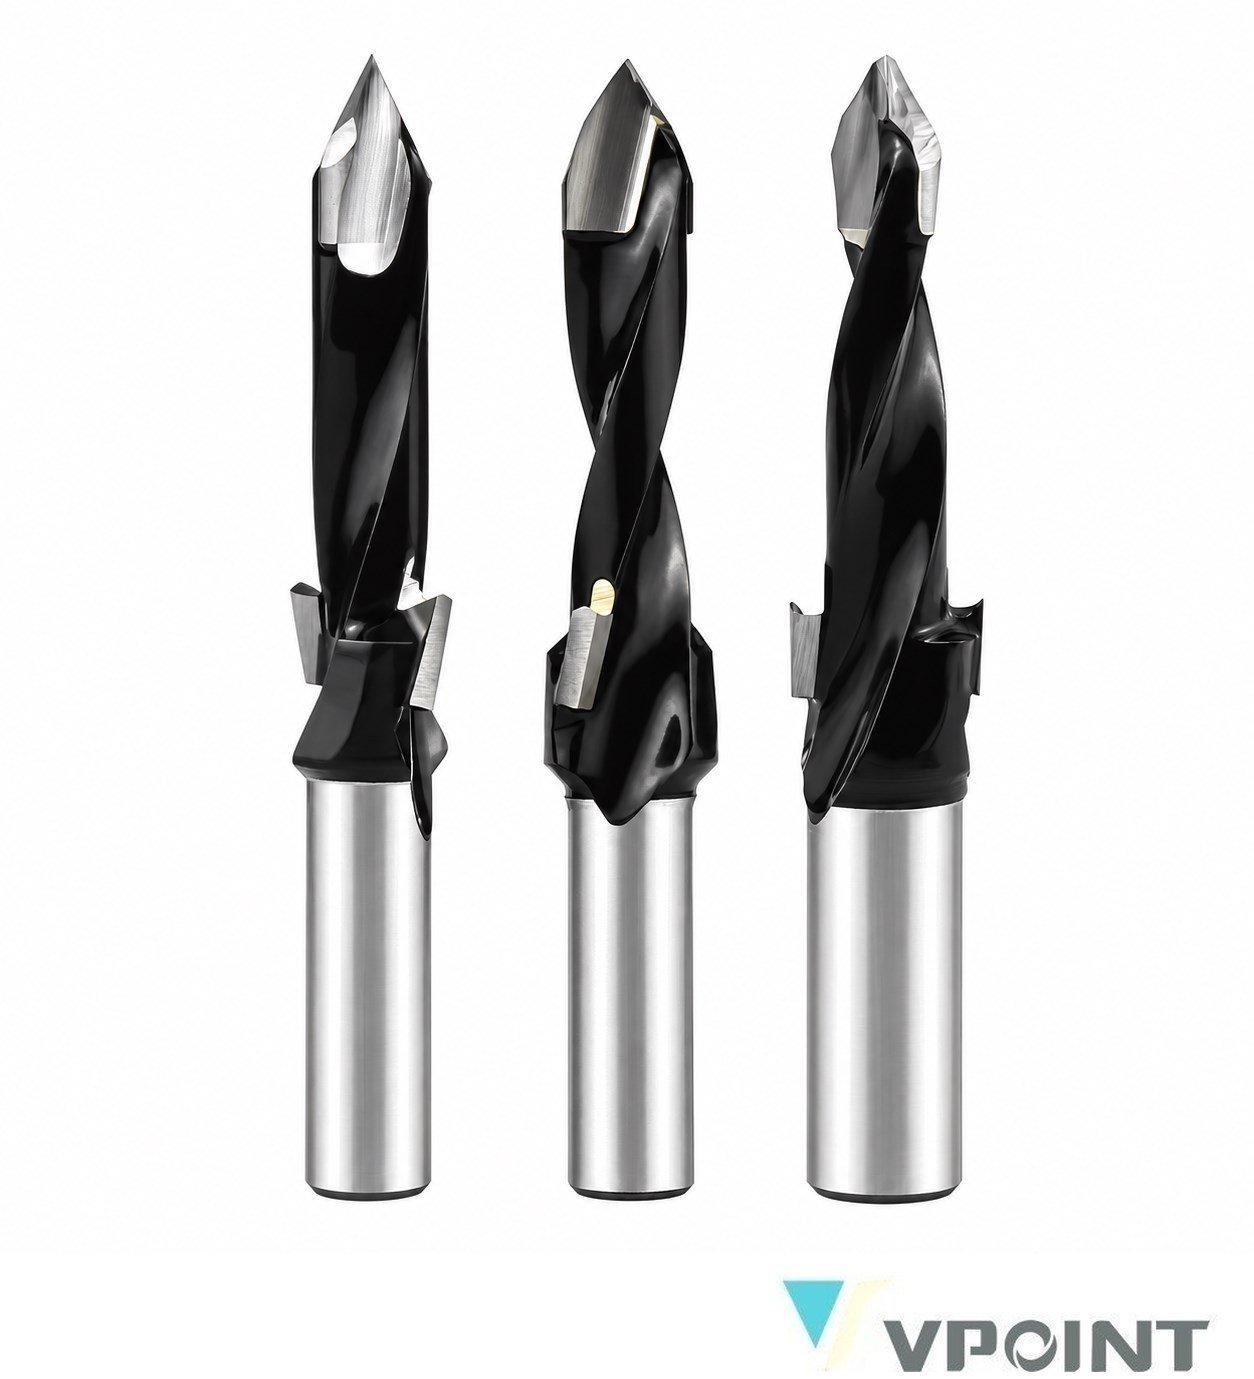


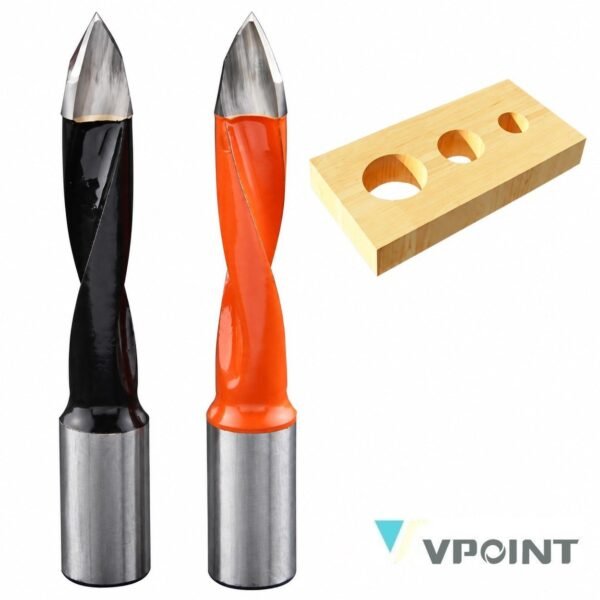
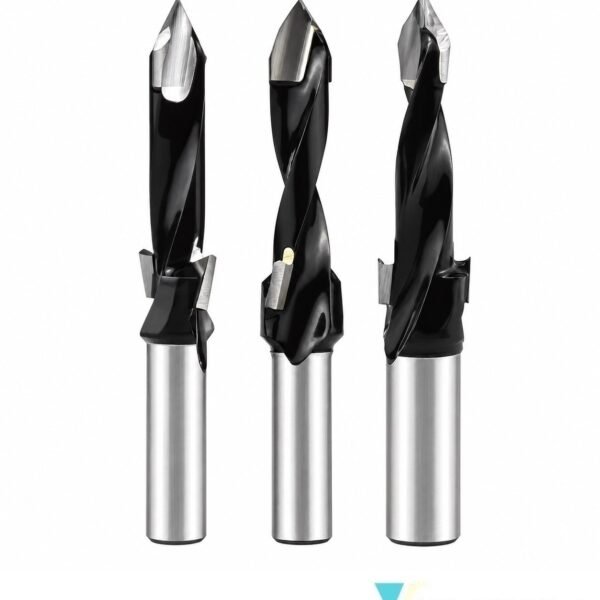
Carbide Step Drill for Magnetic-Levitation Side-Hole Machines for Woodworking Production
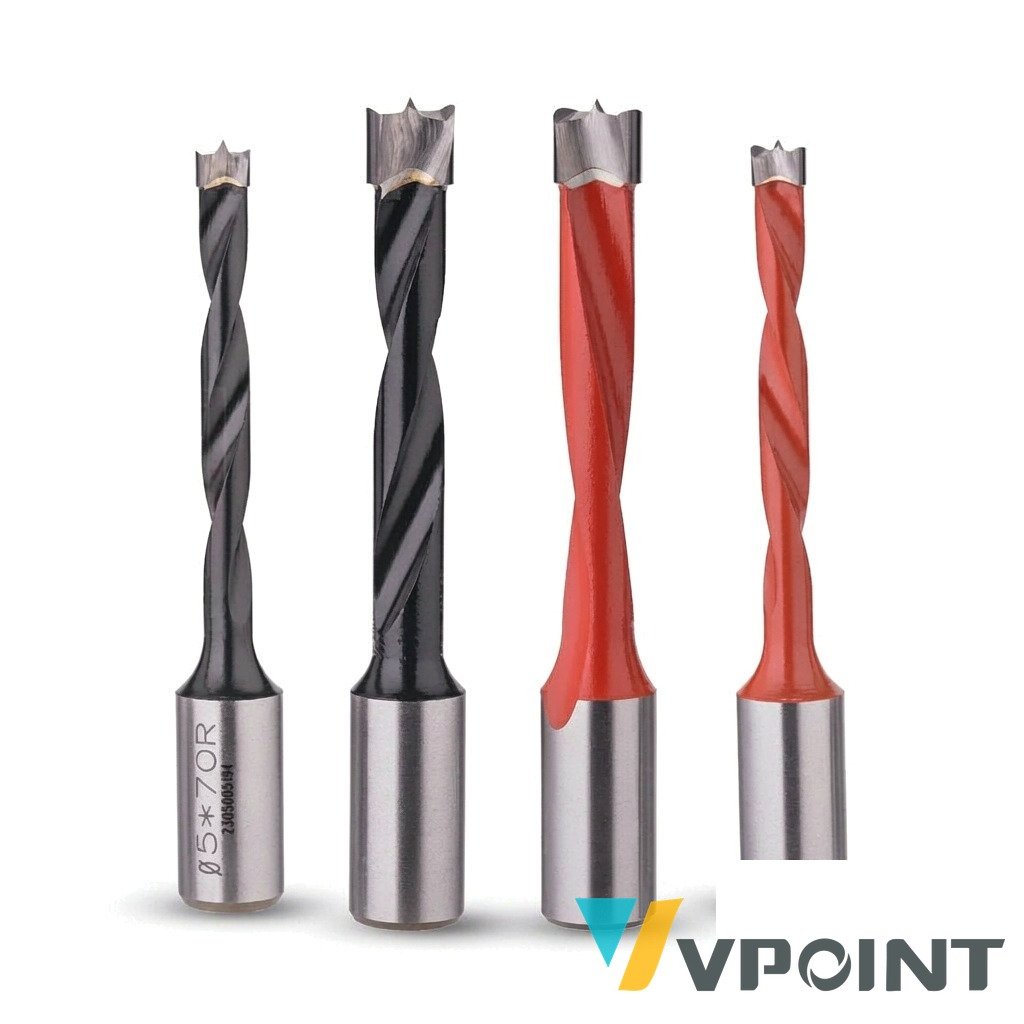
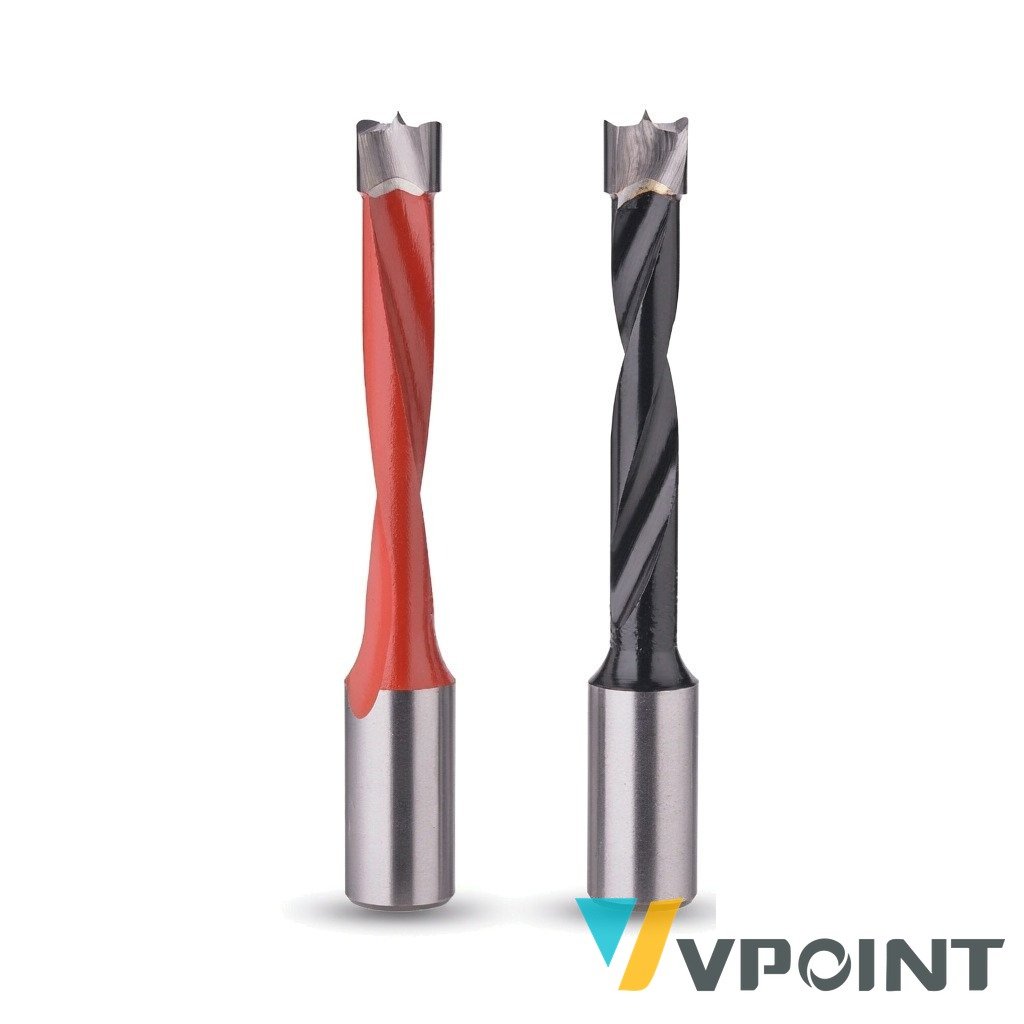
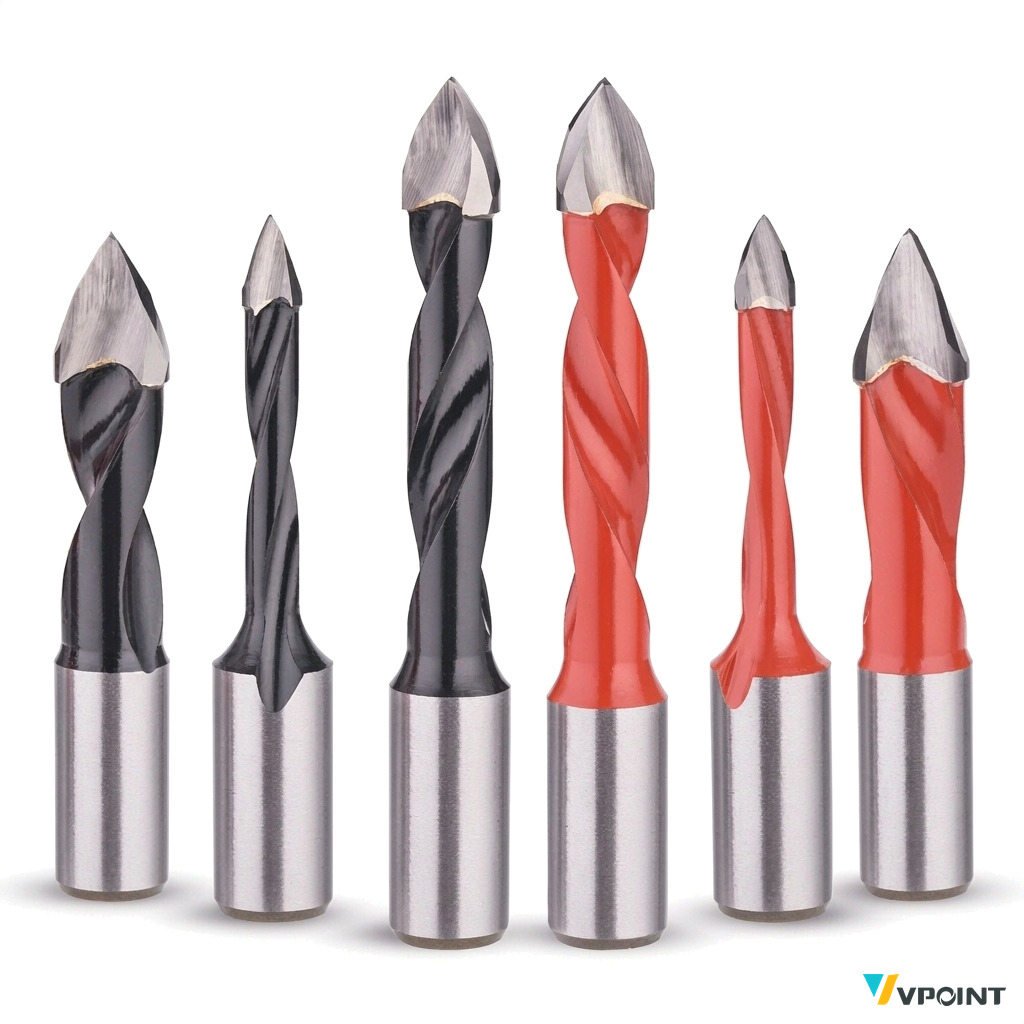
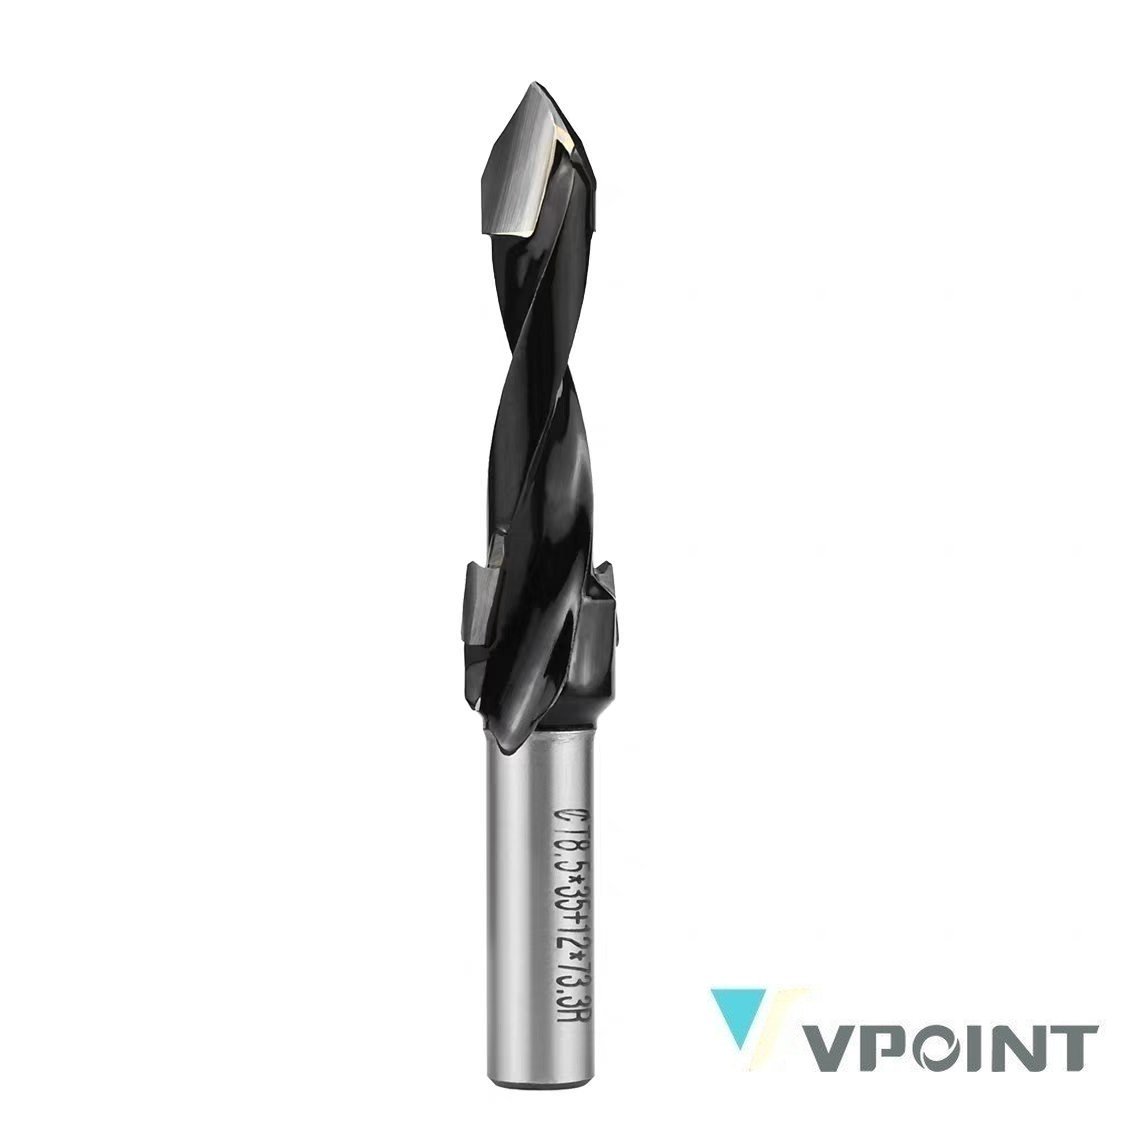
This step drill is intended for magnetic-levitation side-hole drilling machines, combining tungsten-carbide cutting edges with a high-speed steel shank. A pilot section drills the system hole while the larger stepped diameter opens the cam fitting — one tool, one pass.
Design and Construction
+The pilot section and larger stepped diameter are ground in one profile: pilot diameters 8–8.5 mm with a 35 mm pilot length, stepping up to a 12 mm step diameter, on 8 or 10 mm shanks, at a 73.3 mm overall length, right-hand rotation. The series is produced in the Sichuan and Dongguan, China manufacturing bases.
How It Works
+In the side-hole machine the pilot centres the tool in the small system hole while the step enlarges it to the cam diameter at a controlled depth. The carbide edges hold both diameters on MDF and particleboard, keeping the cam seat concentric with the pilot hole.
Applications
- Side-hole drilling on magnetic-levitation side-hole machines
- Cam-fitting and system-hole drilling in cabinet side panels
Suitable Materials
- MDF, density board and particleboard
- Not suitable for plywood / multilayer board or solid pine wood, per the original application list; confirm the material before ordering
Material Comparison: High-Speed Steel (HSS) Tool vs. Solid Carbide Tool
+Typical industry data for reference. Actual results depend on the workpiece grade, machine condition and feed rate.
| Property | High-Speed Steel (HSS) Tool | Solid Carbide Tool |
|---|---|---|
| Cutting edge hardness | ≈ 60–65 HRC (HSS) | 1,500–2,000 HV (solid carbide) |
| Heat resistance of the edge | Loses hardness above ≈ 315 °C | Retains hardness up to ≈ 1,000 °C |
| Edge life on abrasive panels | Baseline (1×) | 5–10× longer edge life |
| Feed rate at equal quality | Lower | Higher |
| Sharpness retention on MDF / particleboard | Dulls quickly | Holds the edge through long runs |
| Regrinding cycles over tool life | Limited | More regrinds |
| Cut edge quality as the edge wears | More fuzzing and tearout | Consistent clean walls |
| Rigidity in long tools | Lower | Higher (solid carbide body) |
| Typical machines | Light-duty routers and drills | CNC machining centres, multi-spindle borers |
| Cost per hole / metre of cut | Higher over long runs | Lower over long runs |
Delivery Scope
Choose the exact pilot and shank combination from the table and confirm the side-hole machine model.
+Each order also includes an inspection record. Send the machine model, board material and the pilot/step diameters required so the configuration is confirmed before production.
Why Choose VPOINT
+VPOINT supports this carbide tool series with:
- One-year warranty on every tool
- Custom diameters, shanks and rotations produced to order
- Regrinding service to extend tool life
- Factory direct since 2008, ISO 9001 certified
- Dual manufacturing bases in Sichuan and Dongguan, China
Precision & Quality Control
+Every step drill is inspected before shipment: cutting diameter, shank diameter and tool runout are checked against the specification table at micron level. Production follows an ISO 9001 process with batch traceability, so reorders match the original configuration.
Specifications
The table below reproduces the original specification chart. Dimensions are in millimetres; R denotes right-hand rotation.
| P | i | l | o | t | d | i | a | m | e | t | e | r | ( | m | m | ) | ||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| P | i | l | o | t | l | e | n | g | t | h | ( | m | m | ) | ||||
| S | t | e | p | d | i | a | m | e | t | e | r | ( | m | m | ) | |||
| O | v | e | r | a | l | l | l | e | n | g | t | h | ( | m | m | ) | ||
| S | h | a | n | k | d | i | a | m | e | t | e | r | ( | m | m | ) | ||
| R | o | t | a | t | i | o | n |
| 8 | |||
|---|---|---|---|
| 3 | 5 | ||
| 1 | 2 | ||
| 7 | 3 | . | 3 |
| 8 | |||
| R |
| 8 | . | 5 | |
|---|---|---|---|
| 3 | 5 | ||
| 1 | 2 | ||
| 7 | 3 | . | 3 |
| 8 | |||
| R |
| 8 | . | 5 | |
|---|---|---|---|
| 3 | 5 | ||
| 1 | 2 | ||
| 7 | 3 | . | 3 |
| 1 | 0 | ||
| R |
Frequently Asked Questions
Which pilot and shank combinations are listed?
+The chart lists pilot diameters of 8 and 8.5 mm with a 35 mm pilot length, a 12 mm step diameter, 73.3 mm overall length, and shank diameters of 8 or 10 mm, right-hand rotation.
Can it drill plywood or solid pine?
+No. The original application list covers MDF, density board and particleboard only, and explicitly excludes plywood / multilayer board and solid pine.
Why a stepped profile?
+The pilot drills the system hole while the step opens the cam fitting in one pass, keeping the two diameters concentric on the side-hole machine.
What should I send for a quotation?
+The side-hole machine model, board material and thickness, and the required pilot/step diameters and shank size.
+Key words: carbide step drill, side hole drilling bit, magnetic levitation drill, cam fitting step drill