- PCD Tools For Wood
- Replaceable Insert Router Bits
- CNC End Mill
- Cutter Head
- Woodworking Tools
- Industries Knives
- Carbide Burr
- Carbide Rotary Burr
- Tungsten Carbide Burr Bits
- Tungsten Carbide Burr Set
- Cylindrical Carbide Burr
- Long Shank Carbide Burr
- Double Cut Carbide Burr
- Flame Carbide Burr
- Cone Carbide Burr
- Burr Blanks
- Carbide Rods
- Tire Reamer Bit
- Tungsten Carbide End Mill
- Carbide Tire Studs
- Snow Tire Studs
- ATV Tire Studs
- Motorcycle Tire Studs
- Mining & Oiling


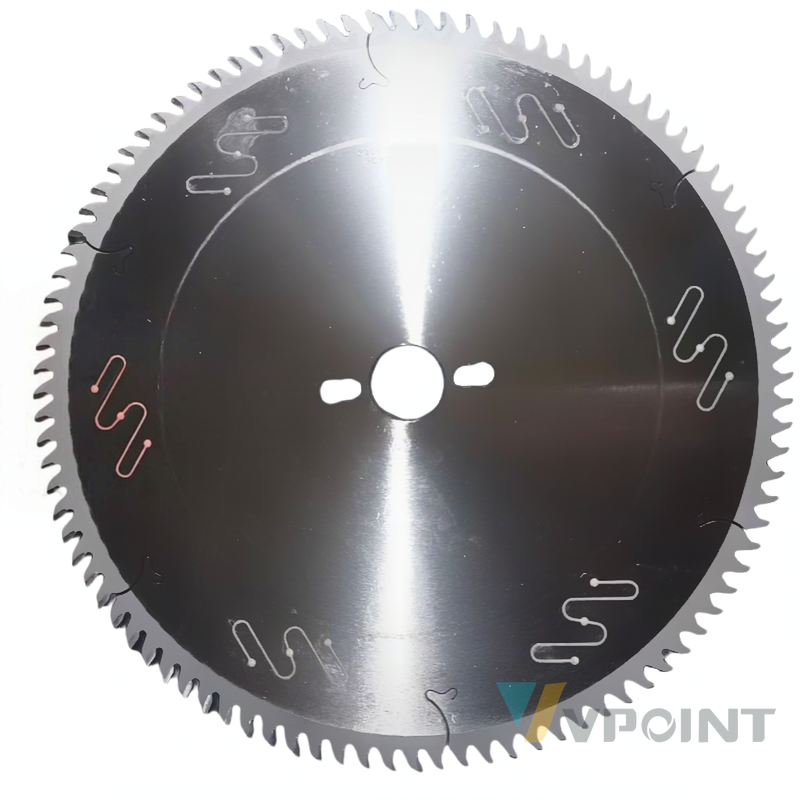
PCD Grooving Saw Blade for Edge Banders for Panel and Wood Processing — a VPOINT saw tool for panel sizing and beam saws, sized for MDF / HDF and similar workpieces. The specification table below lists dimensions; the performance data table gives standard reference speeds and feeds to start with, and the FAQ covers selection, parameters and service. ISO 9001 production, batch-verified, custom sizes from drawings.
PCD Grooving Saw Blade for Edge Banders for Panel and Wood Processing
This PCD saw blade is supplied for grooving operations on edge-banding equipment, cutting the rear groove for the hidden fastener system in cabinet production. The material list includes MDF, particleboard, composite panels, solid wood and hardwood.

Design and Construction
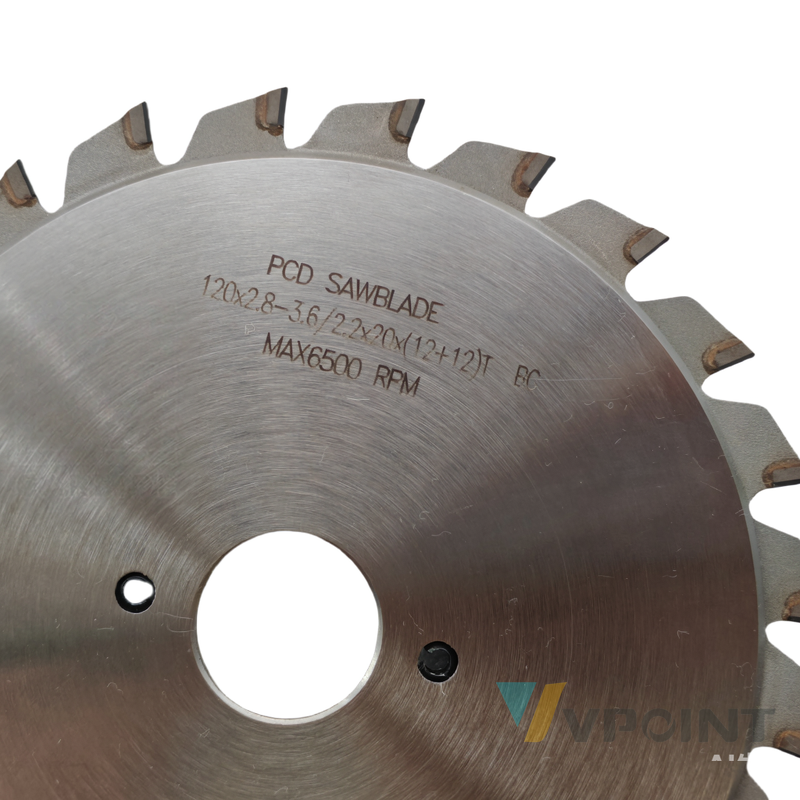
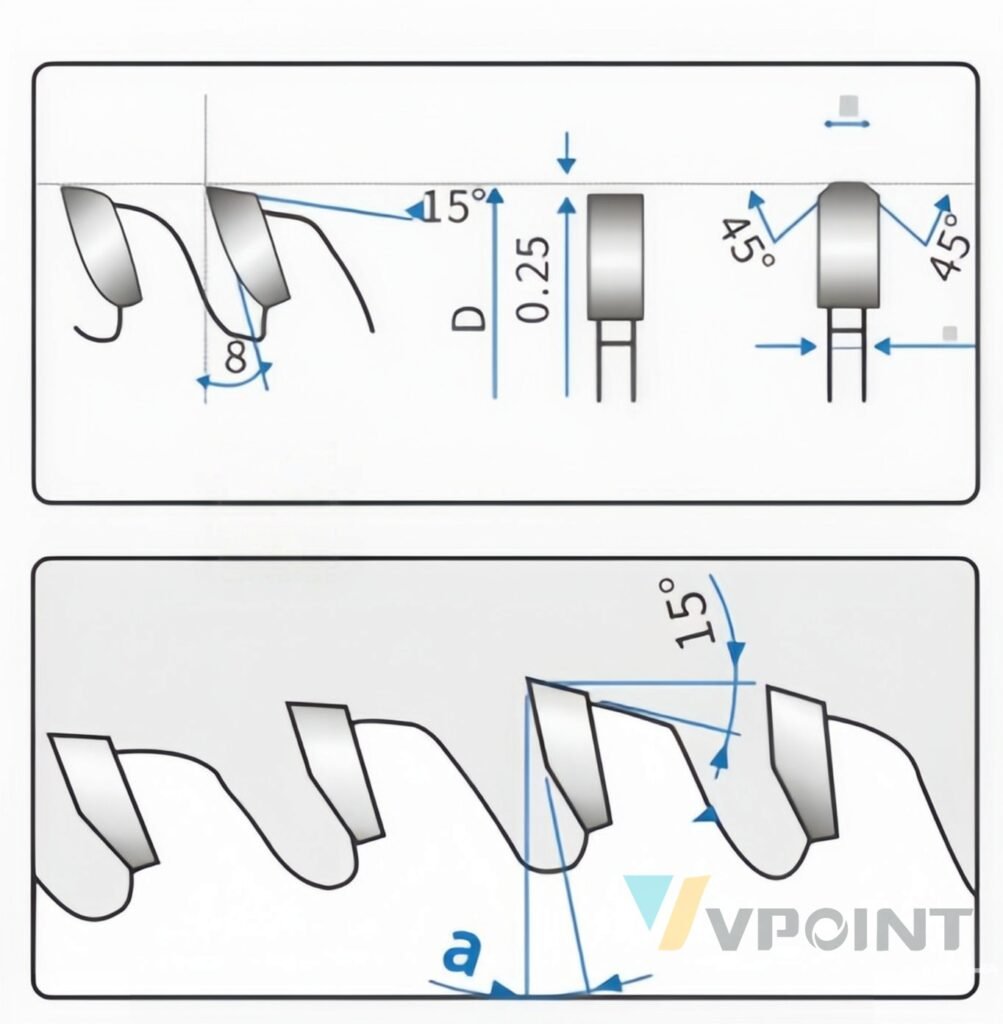
+Polycrystalline diamond (PCD) teeth are brazed into a thin steel plate sized for the edge bander grooving unit. The chart lists diameters from 80 to 160 mm, cutting widths from 1.5 to 6.0 mm, bores of 25.4/30/35 mm and tooth counts from 12 to 24. The series is produced in the Sichuan and Dongguan, China manufacturing bases.
How It Works
+Mounted in the edge bander grooving unit, the blade cuts a precise rear groove that receives the cabinet hanging rail. The PCD edge keeps the groove width stable over long runs on abrasive boards, so rails fit without rework.
Applications
- Grooving operations on edge-banding equipment (rear groove for hanging rails)
- Grooving MDF, particleboard, composite panels, solid wood and hardwood cabinet panels
Suitable Materials
- MDF, particleboard, composite panels, solid wood and hardwood, subject to grade and application review
- Suitability depends on the specific material grade, groove requirement and machining parameters; confirm the application before ordering
Material Comparison: Traditional Carbide-Tipped Saw Blade vs. Diamond (PCD) Saw Blade
+Typical industry data for reference. Actual results depend on the workpiece grade, machine condition and feed rate.
| Property | Traditional Carbide-Tipped Saw Blade | Diamond (PCD) Saw Blade |
|---|---|---|
| Cutting material hardness | 1,500–2,000 HV | 7,000–9,000 HV |
| Edge life on MDF / particleboard | Baseline (1×) | 15–20× longer edge life |
| Edge life on solid wood | Baseline (1×) | 10–13× longer edge life |
| Edge life on laminate / compact board | Baseline (1×) | 10–15× longer edge life |
| Sharpening cycles | 2–4 times | 5–8 times |
| Cut edge quality | Ra 0.4–0.8 µm, more fuzzing | Ra 0.2–0.4 µm, cleaner edge |
| Thermal conductivity | ≈ 100 W/m·K | ≈ 500 W/m·K, heat cleared faster |
| Friction coefficient | ≈ 0.3 | ≈ 0.05–0.1, lower cutting force |
| Chipping risk on brittle boards | Higher at high feed | Lower, stable edge at high feed |
| Cost per metre of cutting | Higher over long runs | Lower over long runs |
Delivery Scope
Blades are produced against the groove requirement specified for the machine; confirm the complete configuration before ordering.
+Each order also includes an inspection record. Send the edge bander make and model, groove position and width, workpiece material, blade diameter, bore and current blade reference so the configuration is confirmed before production.
Why Choose VPOINT
+VPOINT supports this saw blade series with:
- One-year warranty on every saw blade
- Custom diameters, kerfs, bores and tooth counts produced to order
- Regrinding service to extend blade life
- Factory direct since 2008, ISO 9001 certified
- Dual manufacturing bases in Sichuan and Dongguan, China
Precision & Quality Control
+Every grooving saw blade is inspected before shipment: diameter, bore, kerf, plate flatness and tooth geometry are checked against the specification table at micron level. Production follows an ISO 9001 process with batch traceability, so reorders match the original configuration.
Specifications
The table below reproduces the original specification chart. Dimensions are in millimetres; slash-separated values are listed options and do not confirm every possible combination. D is diameter, B cutting width, d bore and Z tooth count.
| Diameter D (mm) | Cutting width B (mm) | Bore d (mm) | Teeth Z |
|---|---|---|---|
| 80 | 1.5 / 1.8 | 25.4 / 30 / 35 | 12 |
| 80 | 2.0 / 2.4 | 25.4 / 30 / 35 | 12 |
| 100 | 1.6 / 1.8 | 25.4 / 30 / 35 | 12 |
| 100 | 2.0 / 2.5 | 25.4 / 30 / 35 | 12 |
| 125 | 1.6 / 1.8 | 25.4 / 30 / 35 | 18 |
| 125 | 2.0 / 2.6 | 25.4 / 30 / 35 | 18 |
| 125 | 3.0 / 3.2 | 25.4 / 30 / 35 | 18 |
| 125 | 3.5 | 25.4 / 30 / 35 | 18 |
| 125 / 135 | 4.0 | 25.4 / 30 / 35 | 18 / 24 |
| 125 / 140 | 4.5 | 25.4 / 30 / 35 | 18 / 24 |
| 125 / 150 | 5.0 | 25.4 / 30 / 35 | 18 / 24 |
| 125 / 160 | 5.5 | 25.4 / 30 / 35 | 18 / 24 |
| 125 / 160 | 6.0 | 25.4 / 30 / 35 | 18 / 24 |
Performance Data
Standard reference values for guidance only — set final speeds by blade diameter and tooth count, and confirm on the actual panel stack.
| Material | Typical spindle speed | Typical feed | Notes |
|---|---|---|---|
| MDF / HDF | 5,000–6,500 rpm | 9–16 m/min | Smooth kerf, minimal edge fuzzing |
Frequently Asked Questions
Which widths and diameters are available?
+The chart lists diameters from 80 to 160 mm, cutting widths from 1.5 to 6.0 mm, bores of 25.4/30/35 mm and tooth counts from 12 to 24, with slash-separated options.
How is the groove width set?
+The cutting width B must match the rail system. Send the groove position and width and the edge bander model; slash-separated values are options and the complete combination is confirmed before ordering.
Can it run on my edge bander?
+Send the edge bander make and model, groove requirement, workpiece material, blade diameter and bore for confirmation against the machine.
What should I send for a quotation?
+Groove width and depth, panel material and thickness, blade bore, rotation and machine model, plus a current blade reference where available.
What spindle speed suits MDF / HDF?
+Set the saw arbor near 5,000–6,500 rpm with the feed around 9–16 m/min; final speed depends on blade diameter and tooth count — larger diameters run slower.
How long do PCD teeth last compared with TCT saw blades?
+On abrasive chipboard and MDF, PCD teeth typically run 10–20 times longer than TCT before needing service, which is why panel-sizing lines standardise on PCD.
How do I choose the tooth count?
+More teeth give a cleaner edge on thin or melamine-faced panels; fewer teeth clear chips faster on thick, gummy stock. Match the tooth pitch to your feed rate.
+Key words: PCD grooving saw blade, diamond grooving blade, edge bander grooving blade, rear groove saw blade, PCD saw blade, diamond saw blade, panel sizing saw blade, PCD scoring blade, diamond tip circular saw, saw blade, panel saw blade, scoring saw blade, circular saw blade, carbide saw tips, TCT saw blade, reversible knives, rota-tip bit, constant cutting diameter, rotate insert 90 degrees, double the cutting life, on-machine knife change, ER collet, 1/2-inch shank insert bit, furniture manufacturing, furniture factory, cabinet making, acrylic sheet, solid wood, particleboard, chipboard, plywood, rubber sheet, rubber board, hardwood, softwood, MDF, HDF, melamine board, flycutter, planing bit, surfacing bit, slab flattening bit, bottom cleaning bit, spoilboard leveller, rabbeting bit
Sources & standards: ISO 9001 quality management · UNSPSC commodity codes · eClass product classification
Related Search Terms
PCD saw blade, diamond saw blade, panel sizing saw blade, PCD scoring blade, diamond tip circular saw, grooving, blade, banders